Industrial Bakery Chain
08BSS A-1 Stainless Steel Attachment Chain
08BSS A-1 Stainless Steel Attachment Chain is presented as a measured-geometry configuration for industrial bakery conveying. Use the dimensional values below for identification and RFQ preparation; final material, heat treatment, clearance, working rating and attachment details are confirmed for the ordered configuration and actual machine duty.
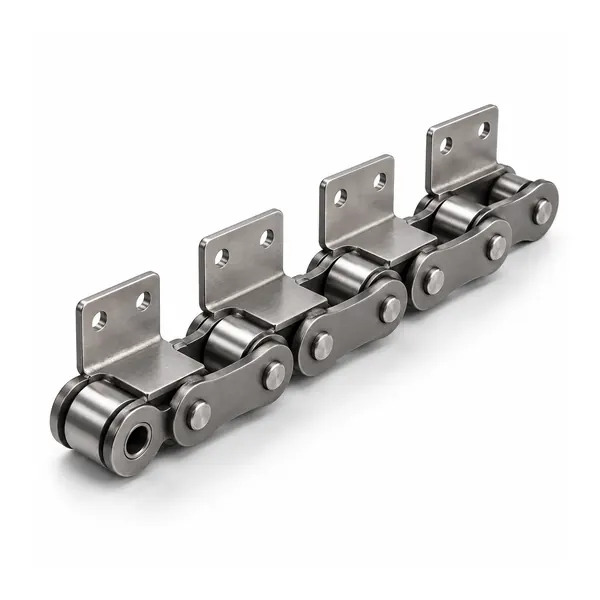
Configuration Overview
08BSS A-1 Stainless Steel Attachment Chain is presented as a measured-geometry configuration for industrial bakery conveying. Use the dimensional values below for identification and RFQ preparation; final material, heat treatment, clearance, working rating and attachment details are confirmed for the ordered configuration and actual machine duty.
This chain can be reviewed for proofing, baking, cooling, pan handling or transfer service depending on the category and installed interface. A replacement match should preserve pitch, transverse dimensions, sprocket engagement and carrier location.
How the Chain Is Built
A conveyor chain is a sequence of articulated bearings restrained by link plates. The pin and bush establish the bearing joint; a roller or bush engages the sprocket and, where applicable, runs on a track. Bakery versions may add stainless construction, increased clearances, extended pins, hollow pins or attachments for pans and carriers.
Do not use a photograph alone to approve interchangeability. Two chains can look alike while differing in inside width, pin length, attachment offset or roller diameter. Those differences affect sprocket seating, tracking and machine clearances.
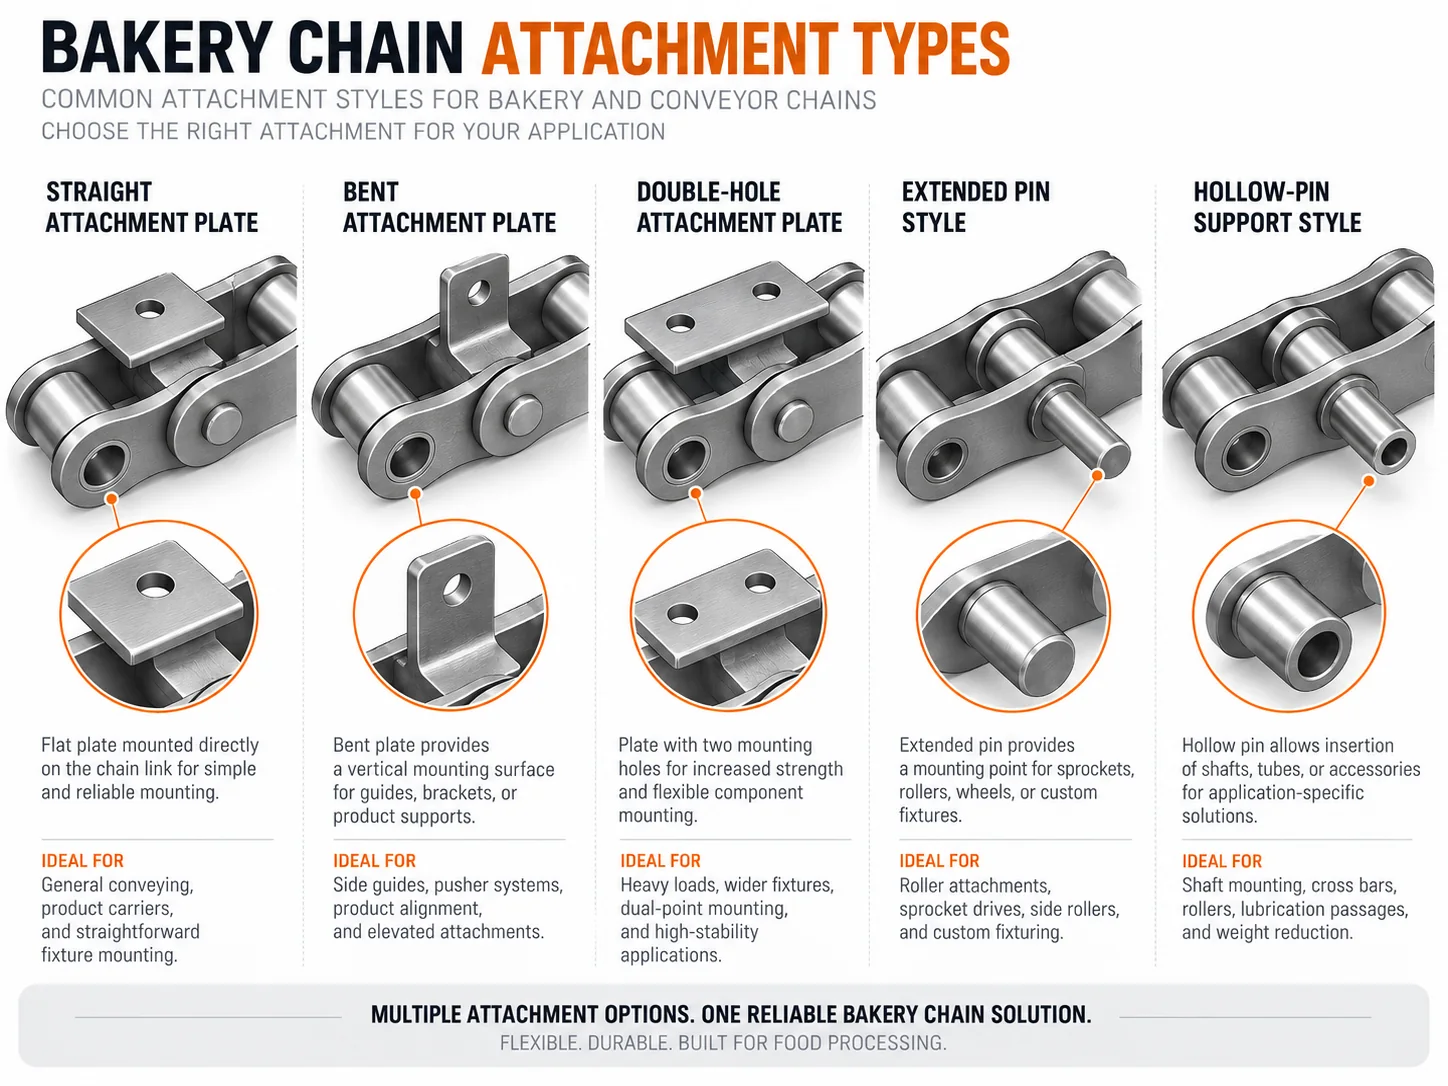
Dimension Reference

The drawing/diagram is shown complete and is not cropped. Use it with the table below for RFQ preparation.
Technical Specifications
| مواصفة | القيمة المرجعية |
|---|---|
| Pitch 12.70 mm | Confirm on drawing |
| Base series 08BSS | Confirm on drawing |
| A-1 attachment configuration | Confirm on drawing |
Values shown here are identification dimensions associated with this configuration. Confirm the final production drawing before installation, especially where material, clearance, attachment position or performance rating is application-dependent.

Bakery Application Context
In bakery equipment, chain duty is defined by more than the product being conveyed. Proofing systems add humidity and long circulation paths; ovens add heat and thermal movement; cooling conveyors may use long transfer routes; pan and tray systems add concentrated carrier loads; packaging areas often require stable, clean transfer.
Record the machine zone, product carrier, chain speed, load per carrier and cleaning routine. If the chain passes through a transition between zones, include that transition in the RFQ because temperature and contamination can change along the route.
Selection and Customization
Geometry match
Confirm pitch, inside width, roller/bush diameter, pin diameter, plate height and overall width.
Attachment match
Define mounting holes, bend direction, offset, cross-rod size and repeated spacing.
Material choice
State moisture, washdown, cleaning chemistry and temperature; material is confirmed against those conditions.
System check
Inspect sprockets, guides, take-up and alignment so a new chain is not installed into a worn or misaligned system.
Installation, Inspection and Maintenance
Before installation, lock out the machine and inspect the sprockets and guides. Worn or hooked teeth can prevent smooth roller seating and accelerate wear in a new chain. Confirm that shafts are aligned, the take-up has usable travel and parallel strands remain synchronized where the conveyor uses more than one chain.
During commissioning, watch the chain through at least one complete circuit. Look for tight joints, side rubbing, carrier interference and unusual noise at sprocket entry or exit. After the initial running period, recheck tension or take-up position according to the machine maker’s practice.
For maintenance planning, our bakery chain maintenance guide covers inspection points, while the سلاسل المخابز المزودة بملحقات page compares related configurations.
Manufacturing and Inspection
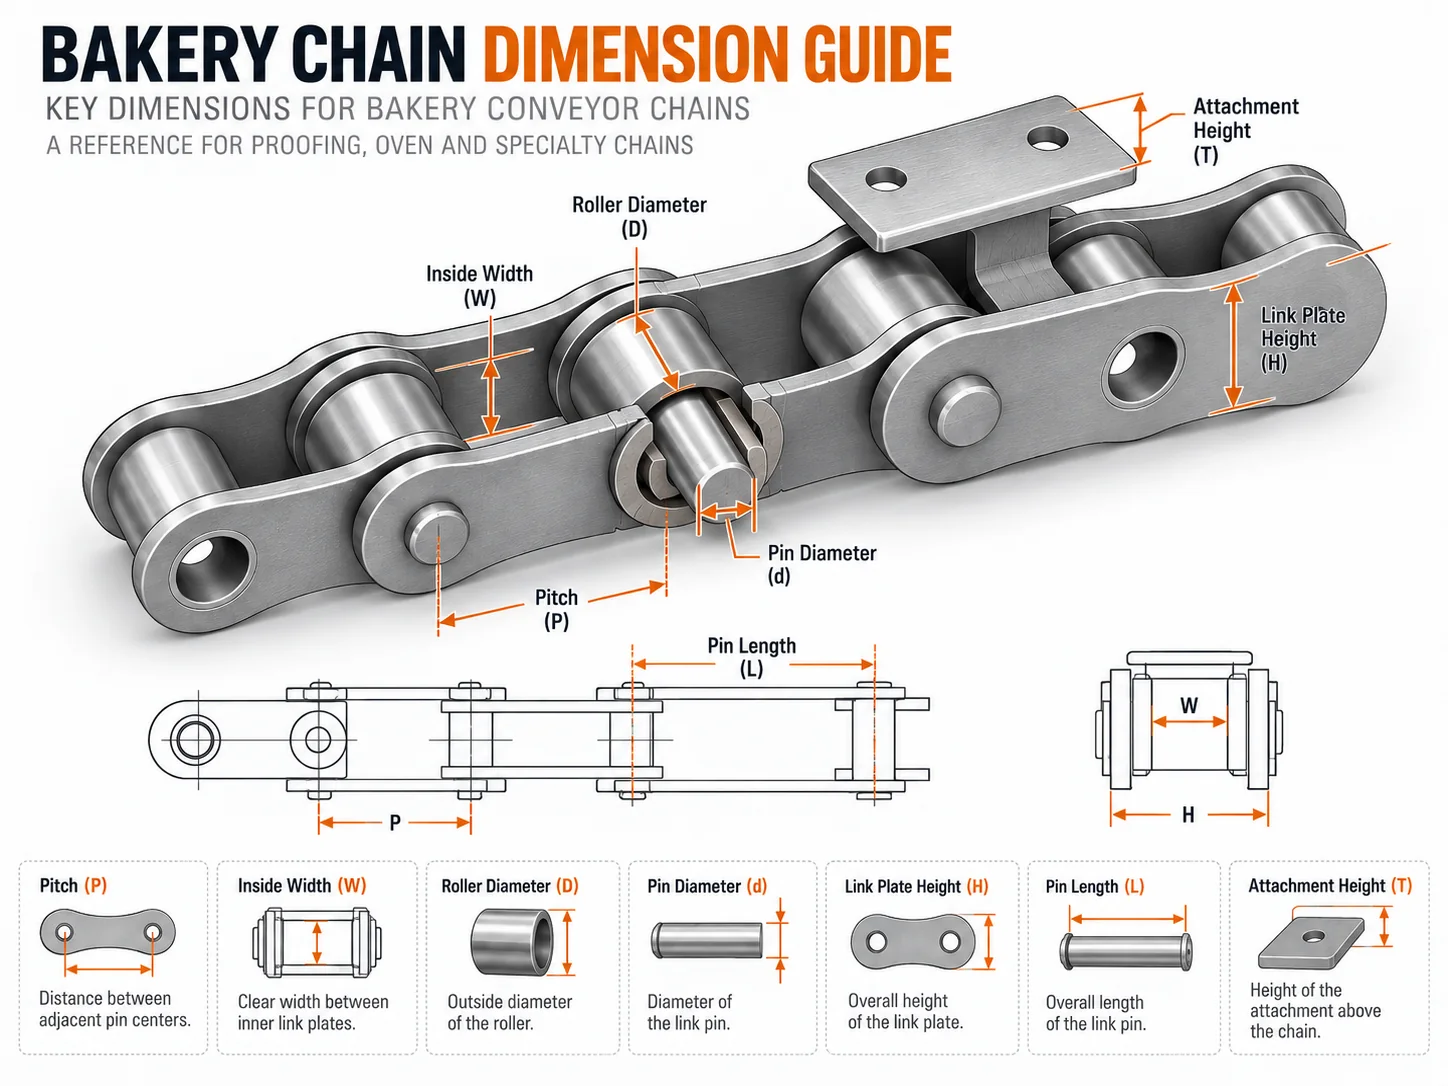
Dimensional inspection should verify the characteristics that control interchangeability: pitch consistency, transverse width, pin projection, roller or bush size and attachment location. For custom configurations, inspection should also verify the carrier hole pattern and attachment interval against the approved drawing. Product-specific inspection documents can be arranged according to the confirmed order requirements.
التحقق من الشركة لمراجعة المشتري
تتوفر خدمات تدقيق الموردين الخارجيين والتحقق من الشركات، بدعم من SGS وTÜV Rheinland، لمساعدة المشترين على مراجعة هوية الشركة وعملياتها التجارية وملف تعريف المورد وقدراتها التصنيعية العامة. ويمكن توفير تقارير فحص خاصة بالمنتج، ووثائق المواد، أو سجلات الامتثال وفقًا لمتطلبات الطلب ونطاق المنتج المُعتمد.
Machine-Side Verification Before Release
Reproduce the identification dimensions
For 08BSS A-1 Stainless Steel Attachment Chain, record Pitch 12.70 mm, Base series 08BSS, A-1 attachment configuration using consistent datum points. Where wear is visible, measure over several pitches and note whether the chain is relaxed or under load. The objective is a dimension set another engineer can reproduce, not a single convenient measurement.
Check the chain route, not only the strand
Trace the product through pan, tray and carrier handling where the chain provides a mounting interface. Mark drive and tail sprockets, guide rails, return tracks, transfer points and the take-up position. Local scuffing or a tight section can indicate alignment or clearance problems that a new chain alone will not correct.
Treat the interface as a load path
Review A/K/F/L-style attachments, bent plates, mounting holes and carrier brackets. If pans, rods or brackets are fitted, record their hole pattern, offset and repeated spacing. Confirm whether the carrier is rigidly fixed or allowed to articulate, because an over-constrained carrier can force parallel strands out of alignment.
Separate fixed geometry from selectable details
Machine pitch, chain centers and carrier mounting points are often fixed by the existing equipment. Material, joint clearance, roller style or attachment manufacturing method may have room for review. This distinction keeps replacement work compatible while allowing the ordered configuration to reflect repeated mechanical loading combined with bakery heat, moisture or cleaning exposure.
| يفحص | لماذا يُعد ذلك مهماً؟ | ما الذي يجب إرساله أو التحقق منه؟ |
|---|---|---|
| Installed geometry | Verify Pitch 12.70 mm, Base series 08BSS, A-1 attachment configuration against the existing chain or approved machine drawing. | Dimensioned sketch plus side/end photos. |
| Sprockets and guides | Check tooth profile, alignment, guide contact and roller seating. Worn mating parts can make a new chain appear to stretch or run rough. | Tooth count, sprocket photos and guide layout. |
| Take-up and wear | Record current take-up position and any adjustment history. Multi-pitch measurement helps separate joint wear from a simple installation-length issue. | Take-up travel and multi-pitch reading. |
| Environment | Document repeated mechanical loading combined with bakery heat, moisture or cleaning exposure. State normal conditions and short peaks separately where temperature is involved. | Temperature/humidity/cleaning description and lubrication constraints. |
| Release check | Before ordering, compare the proposed chain with guards, sensors, transfers and the full carrier envelope. The final drawing should control dimensions and options, especially where carrier skew, fatigue around attachment bends and interference with guides or sprockets is possible. | Approved drawing revision and requested quantity/length. |
Ordering Information
تخطيط الطلبات والشروط التجارية
الحد الأدنى للطلب: يتم تقييم المنتجات حسب نوعها، ودفعة التصنيع، وقيمة الطلب. تستخدم المنتجات القياسية في الكتالوج عادةً حدًا أدنى للإنتاج يعتمد على الكمية، بينما يمكن مراجعة المنتجات الكبيرة أو ذات القيمة العالية بناءً على قيمة المشروع.
أمثلة: يمكن للعملاء الجدد طلب من قطعة إلى خمس قطع عند اختيار نوع السلسلة وطريقة التصنيع المناسبة. يتم تأكيد سعر العينة وجدواها قبل بدء الإنتاج.
الطلبات المختلطة: يمكن دمج نماذج متعددة بقيمة طلب تبلغ حوالي 1500 دولار أمريكي، وذلك رهناً بتوافق العملية ومتطلبات التعبئة والتغليف.
كميات صغيرة جداً: يتم النظر في طلب 1-2 قطعة فقط للعينات المعتمدة أو الاستبدال أو الحالات الهندسية؛ ولا يتم قبول طلبات البيع بالتجزئة الروتينية، ويمكن أن تؤدي المعالجة الخاصة إلى ارتفاع تكلفة الوحدة.
مهلة: تستغرق العناصر القياسية عادةً من 10 إلى 25 يوم عمل؛ والمكونات المخصصة من 20 إلى 45 يومًا؛ والمعدات القائمة على المشاريع أو الحزم المعقدة من 45 إلى 120 يومًا، بعد الرسم وتأكيد الطلب.
شروط التداول: تُدعم شروط التسليم EXW وFOB وCIF وDAP بشكل شائع. ويمكن مناقشة شروط FCA وCFR وCPT وCIP وDDP فيما يتعلق بوجهة الشحن وخطة الشحن.
Commissioning Checkpoints
Confirm the installed geometry before power-up
For 08BSS A-1 Stainless Steel Attachment Chain, verify chain centers, sprocket alignment, guide clearance and the mating carrier or attachment with the machine stationary. Turn the system manually where the machine design permits. The chain should enter and leave each sprocket without side forcing, and no attachment, rod or plate should contact a guard or guide through the carrier route.
Observe one complete path, not only the drive end
Run at a controlled commissioning speed and watch the loaded and return runs. Pay particular attention to attachment alignment and carrier squareness. Listen for a repeating impact and mark the machine position where it occurs. A symptom that repeats at one location is often more useful than a general statement that the chain is noisy or tight.
Recheck after the real process condition is established
Once the line reaches its normal repeated carrier loading, inspect articulation, tracking and take-up position again. Confirm attachment spacing and guide clearance. Do not compensate for a local interference by adding excessive chain tension. Record any adjustment so the final maintenance baseline reflects the actual commissioned condition rather than the cold, unloaded setup.
Leave maintenance a reproducible reference
Store the approved chain drawing, installed length or pitch reference, sprocket tooth count, take-up position and clear photographs of the critical interface. This creates a baseline for later wear checks and gives purchasing a controlled reference when another 08BSS A-1 Stainless Steel Attachment Chain strand or compatible replacement is required.
الأسئلة الشائعة
Are the dimensions enough to approve a replacement?
They are a strong identification start, but the final check also needs sprocket geometry, attachment arrangement, duty, material and machine clearances.
Can you make a custom attachment?
Custom attachment review is possible when a dimensioned drawing, chain geometry and load/application description are provided.
What should I send with an RFQ?
Send dimensions, photos, existing drawing if available, chain quantity or length, machine type, temperature, cleaning environment, load and requested documentation.

























