Opptaksgeometri
Stigning, bredde, rulle/hylse, tapp, plate, totalbredde og festemønster.
Teknisk veiledning for bakerikjeden
How to Select Attachments for Bakery Pans is best answered by combining measured chain geometry, machine duty and the operating environment. This guide shows what to inspect, record and discuss before a replacement or new-chain decision.
How to Select Attachments for Bakery Pans should be evaluated from the actual conveyor. Start with chain pitch, transverse geometry, sprocket condition and any carrier attachment, then add temperature, moisture, washdown, load, speed and take-up information. The objective is not to identify a chain by appearance; it is to produce an RFQ that preserves the machine interface and makes application-dependent choices explicit.
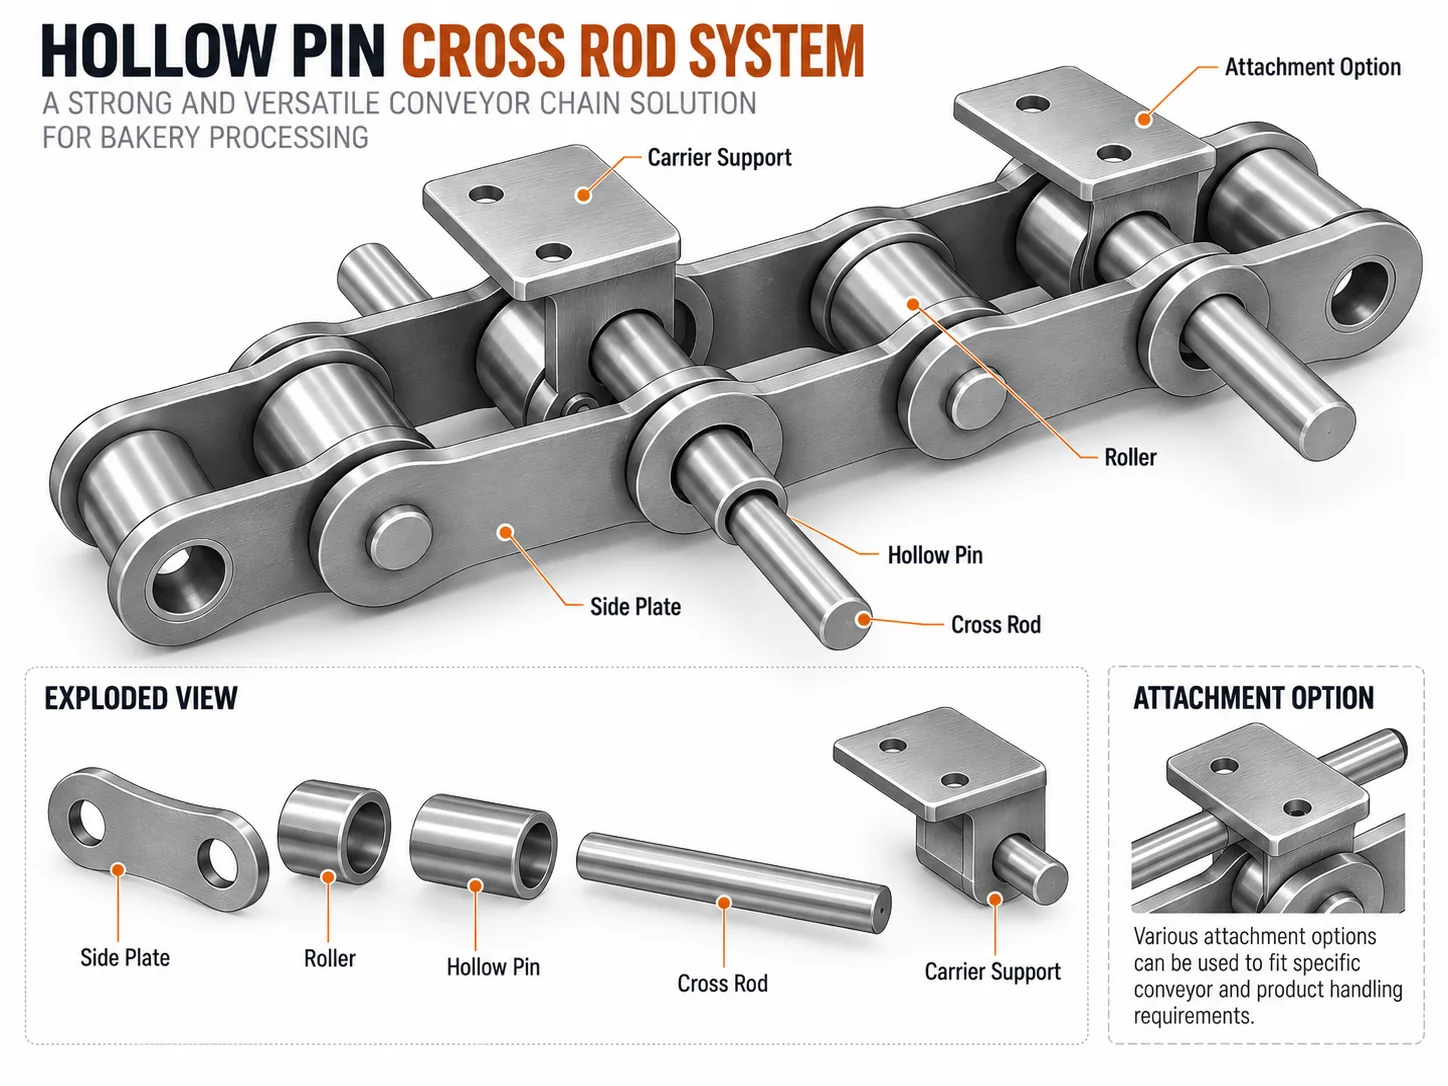
Mål flere egenskaper før du fjerner kjedet. Stigningen bestemmer det grunnleggende girforholdet, men innvendig bredde, rulle- eller bøssingdiameter, pinnediameter, platehøyde, totalbredde og festemål skiller konfigurasjoner som kan dele samme nominelle stigning.
For en slitt kjedetråd, mål den kumulative stigningslengden over flere lenker. Fotografer kjedet fra siden og enden, og inkluder tannhjulet der det er praktisk.
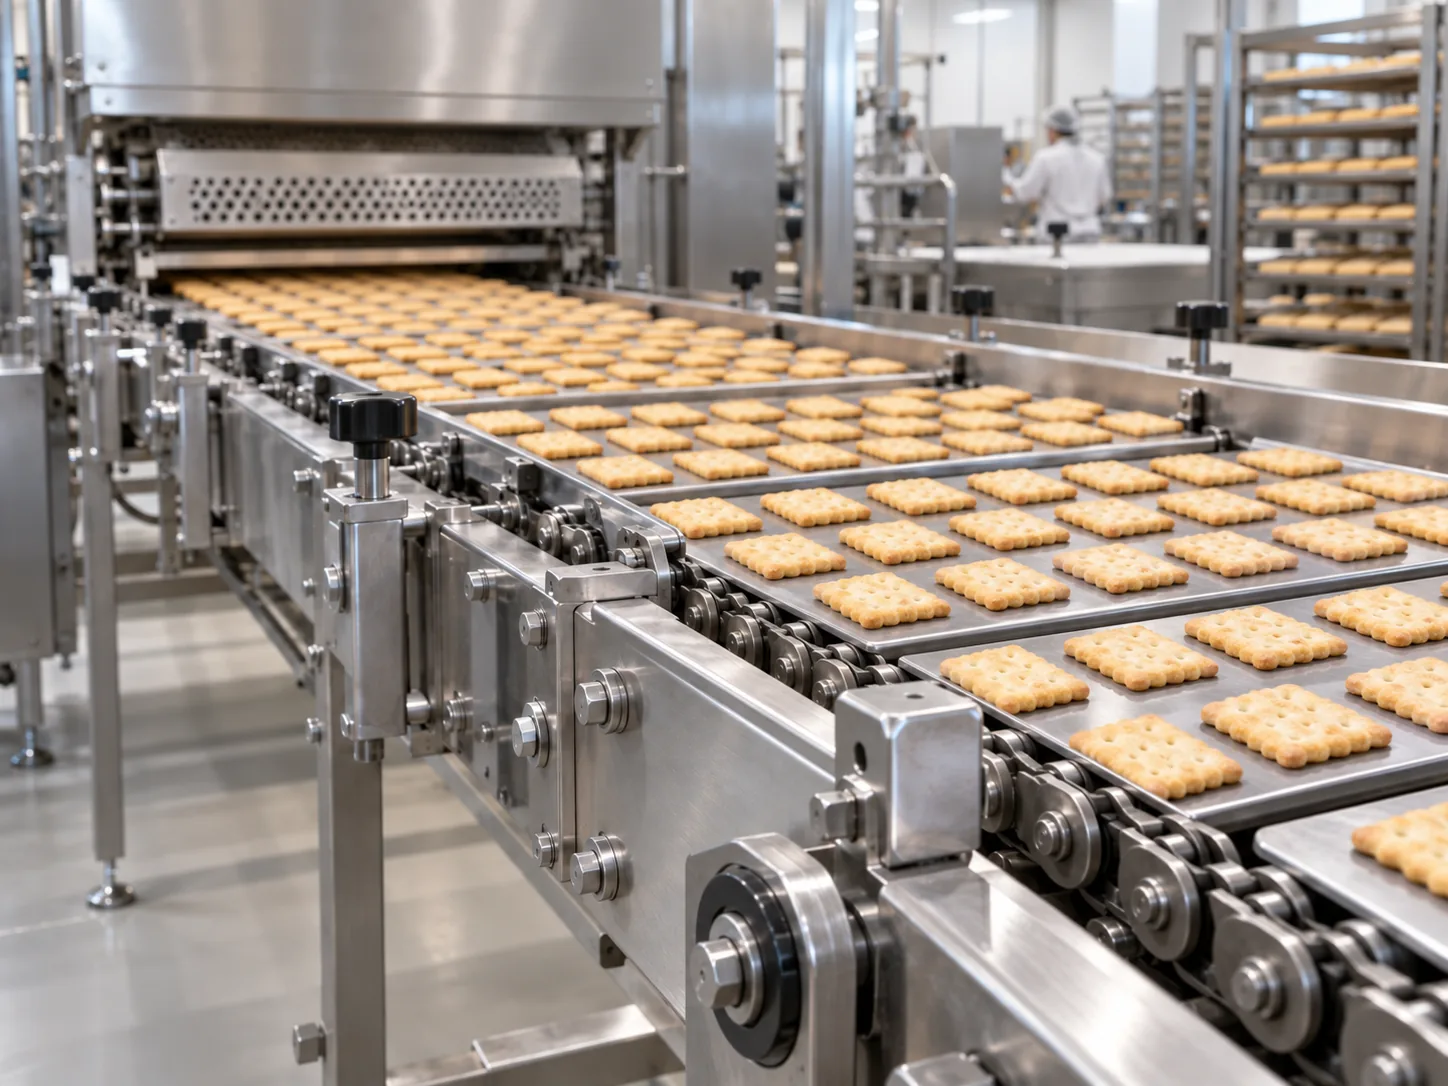
The same chain geometry can behave differently in a humid proofer, a hot oven, an ambient cooling section or a washdown area. For how to select attachments for bakery pans, document the exact machine zone, whether the chain carries product directly or moves pans/fixtures, and whether the joint sees heat, moisture, cleaning chemicals or abrasive residue.
Prosessdata bidrar til å bestemme hvilke egenskaper som er fastsatt ved utskiftbarhet, og hvilke egenskaper – som materiale, klaring eller produksjonsmetode for fester – som bør gjennomgås for applikasjonen.

En kjede fungerer ikke uavhengig. Ruller eller hylser må gå jevnt inn i og ut av tannhjulets tannmellomrom, mens føringsskinner støtter tråden uten å tvinge den sidelengs. Krokede tenner, feiljustering av akselen, eksentriske tannhjul eller en stram føring kan føre til at en ny kjede slites raskt.
Inspiser hele kjedebanen gjennom én full krets. Hvis skaden gjentar seg på samme maskinsted, undersøk den lokale støtten, overføringen eller transportøren før du antar at selve kjedet er defekt.
Stigning, bredde, rulle/hylse, tapp, plate, totalbredde og festemønster.
Temperatur, fuktighet, nedvask, hastighet, last, produksjonstimer og starter.
Tannhjul, føringer, kjedesenter, opptak, justering og klaring mellom bærerhjulene.
Godkjenn den endelig bestilte geometrien, materialet og den applikasjonsavhengige konfigurasjonen før installasjon.
Spør hva som endret seg før problemet oppsto: produksjonshastighet, produkt- eller pannvekt, rengjøringssyklus, smøremiddel, temperatur, vedlikeholdsintervall eller utskiftede tannhjul. Trendinformasjon er mer verdifull enn et enkelt fotografi fordi det viser om slitasjen er jevn eller konsentrert.
Under rutinemessig inspeksjon, se etter stive skjøter, slitasje på ruller, boltbevegelse, sprukne eller bøyde fester, unormal sidekontakt og ujevn opptak. Hold vern og sikkerhetsprosedyrer på plass i henhold til maskineierens krav.
Inkluder de målte dimensjonene, maskin-/prosessnavn, bilder, tegning hvis tilgjengelig, antall eller nødvendig kjedelengde, festeintervall, kjedesenteravstand, informasjon om tannhjul, temperatur, nedvaskingstilstand, last og målleveringsvindu. Se gjennom veiledning for valg av bakerikjede og den oversikt over produktfamilien for neste beslutningstrinn.
A useful diagnosis starts with evidence that can be repeated by a second person. matching pan support geometry to the chain while allowing assembly, cleaning and thermal movement. Record hole pattern, support height, offset, pan pitch, chain centers and attachment interval. When the chain is worn, note which readings may be influenced by joint clearance or deformation, and prefer multi-pitch or multi-point measurements over one isolated dimension.
The chain does not operate by itself. In pan conveyors through proofing, baking or return handling, inspect the sprockets, guides, return path, take-up and carrier interface at the same time. The symptom to watch is pan skew, binding, difficult cleaning or contact with guides. A local problem that repeats at one machine position often points to alignment, clearance or mating-hardware issues rather than a uniform chain problem.
The practical decision is to start from the pan support/load path and work back to the attachment rather than choosing from appearance. That prevents a common error: changing chain tension, material or size before the root constraint has been identified. Use the chain drawing and the machine envelope together, because a configuration that looks correct in isolation can still interfere with a guard, transfer plate, sensor bracket or carrier.
Beskriv driftssyklusen i stedet for et enkelt adjektiv som «varm», «våt» eller «matkvalitet». Oppgi normal og topptemperatur der det er relevant, fuktighets- eller rengjøringseksponering, hastighet, start/stopp-oppførsel og smørebegrensninger. Disse detaljene avgjør om klaringer, materialer eller vedlikeholdspraksis må endres mens den grunnleggende geometrien forblir fast.
| Sjekke | Hvorfor det er viktig | Hva som skal sendes eller bekreftes |
|---|---|---|
| Identifikasjon | Confirm hole pattern, support height, offset, pan pitch, chain centers and attachment interval. Use a measurement sequence that can be repeated after removal so the installed and bench readings can be compared. | Målskisse, skalabevisste bilder og eventuelle eldre tegninger eller delenummer. |
| Ruteposisjon | Map where the chain runs through pan conveyors through proofing, baking or return handling. Mark the exact location of pan skew, binding, difficult cleaning or contact with guides instead of reporting the condition only as a whole-line problem. | Kontekstbilde som viser transportbåndseksjonen, driv-/haleposisjoner og returvei. |
| Paringsdeler | Inspiser tannprofil, rullefeste, aksel-/tannhjuljustering, føringskontakt og opptaksreserve. Disse delene kan skape slitasjemønstre som imiterer et kjedevalgproblem. | Tanntall og bilder av tannhjul, føringslayout og gjeldende opptaksposisjon. |
| Last inn bane | Identify how product carriers, pans, rods or fixtures transfer load into the chain. For this topic, the key focus is matching pan support geometry to the chain while allowing assembly, cleaning and thermal movement. | Bæretegning, festeintervall, kjetting-senteravstand og støttet masse/kraft der det er kjent. |
| Miljø | Registrer temperatur-, fuktighets-, nedvaskings-, forurensnings- og smørerestriksjoner per maskinsone. Skill kontinuerlig eksponering fra korte topper eller rengjøringshendelser. | Sammendrag av driftstilstand og vedlikeholds-/smørepraksis. |
| Utgivelse | The final engineering action is to start from the pan support/load path and work back to the attachment rather than choosing from appearance. The approved drawing should distinguish fixed interchange dimensions from selectable options. | pan drawing, attachment sketch, chain centers, load, temperature and cleaning method. |
A uniform change along the whole strand suggests a different mechanism from damage concentrated at one sprocket, guide or transfer. For How to Select Attachments for Bakery Pans, compare left/right sides and loaded/return paths. The distribution of wear can reveal whether the driver is joint wear, side loading, contamination, thermal change or a carrier that is forcing the chain out of its natural path.
Increasing tension can temporarily change noise or tracking without correcting the underlying cause. If the observed issue is pan skew, binding, difficult cleaning or contact with guides, first confirm alignment, take-up geometry and articulation. Excessive tension can add bearing load and make a marginal guide or attachment problem worse.
Bakeriutstyr kan bevege seg mellom produksjons-, rengjørings- og nedstengningstilstander. En kjede kan leddene normalt når den avkjøles og bli stram når den varmes opp, eller løpe fritt under produksjon, men korrodere etter gjentatte våte nedstengninger. Registrer tilstanden der symptomet oppstår, slik at den valgte korrigerende handlingen retter seg mot den faktiske driftssyklusen.
For an unknown chain, one close-up is not enough. Pair a complete machine-zone image with side and end views of several pitches, a sprocket-engagement photo and a clear attachment/carrier view. Place a scale only where it does not hide the feature being measured. This photo set makes matching pan support geometry to the chain while allowing assembly, cleaning and thermal movement easier to evaluate remotely.
Record hole pattern, support height, offset, pan pitch, chain centers and attachment interval, chain centers, sprocket tooth count and the carrier interface before changing components.
Describe what happens in pan conveyors through proofing, baking or return handling, including temperature or moisture changes, speed, load and cleaning/lubrication constraints.
Document where pan skew, binding, difficult cleaning or contact with guides appears. Compare drive, tail, loaded run, return run and transfer points rather than averaging the entire conveyor.
Include pan drawing, attachment sketch, chain centers, load, temperature and cleaning method. State the required quantity or chain length and any documentation needed with the order.
Review pitch, widths, pin/roller geometry, attachments and material notes on one controlled drawing revision. For How to Select Attachments for Bakery Pans, the release decision should explicitly address matching pan support geometry to the chain while allowing assembly, cleaning and thermal movement.
Etter installasjon, observer minst én full krets, sjekk tannhjulets inn-/utgang og klaring for kjedeholderen, og sjekk opptrekkingen på nytt i henhold til maskinprodusentens prosedyre. Ny kjede skal ikke brukes til å kompensere for slitt eller feiljustert maskinvare.
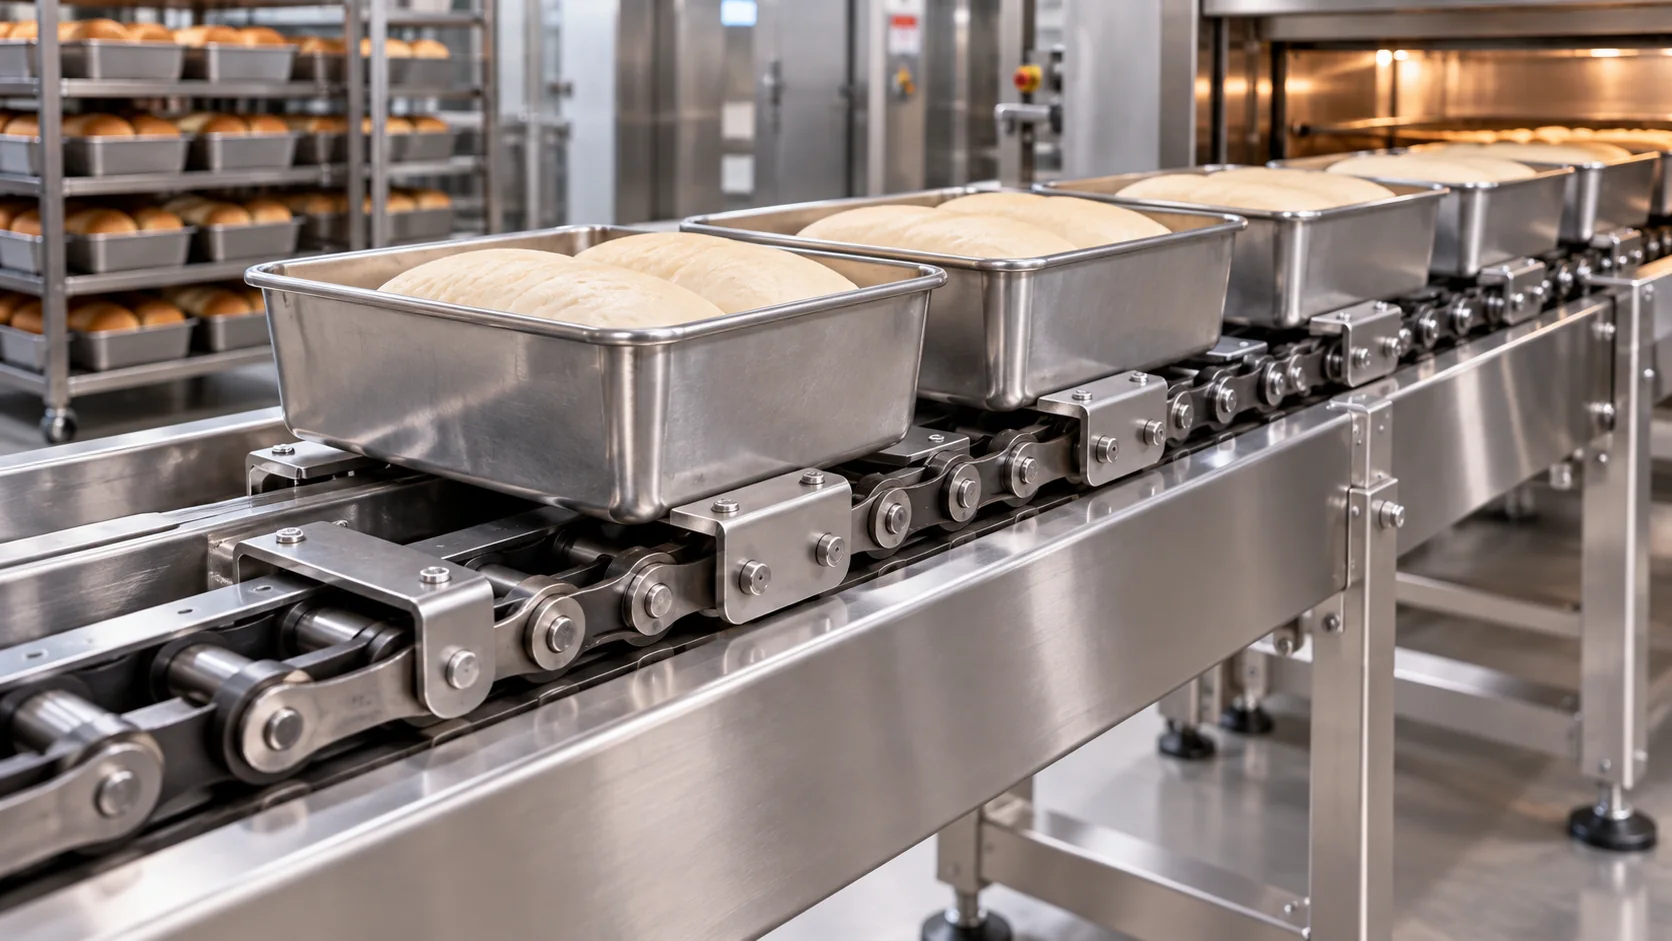
The main reason to keep this process structured is that matching pan support geometry to the chain while allowing assembly, cleaning and thermal movement interacts with more than one component. A change that improves one symptom can shift load into another part of the mechanism. For example, correcting guide alignment may reduce side wear but also expose a take-up setting that was previously compensating for the misalignment. Record changes one at a time so the result can be interpreted.
For planned maintenance, compare the present condition with a baseline whenever one exists. If there is no baseline, create one during the next shutdown: photograph the sprockets and guide surfaces, record take-up position, measure a defined number of pitches, and note the chain’s location in pan conveyors through proofing, baking or return handling. Repeating the same observations later is more informative than relying on general statements such as “the chain has stretched.”
Når en eksisterende tegning er tilgjengelig, må du kontrollere at den installerte maskinvaren fortsatt samsvarer med den. Bakeriutstyr modifiseres ofte i løpet av levetiden: bærere kan repareres, føringsskinner flyttes, tannhjul byttes ut og festeintervaller endres. Tegningen forblir nyttig, men feltverifisering forhindrer at et historisk dokument behandles som bevis på gjeldende konfigurasjon.
Procurement and engineering should use the same evidence package. The RFQ should not separate commercial quantity from technical context: pan drawing, attachment sketch, chain centers, load, temperature and cleaning method. This makes it possible to judge whether a standard series, a modified attachment or a custom replacement is the appropriate route without creating unnecessary back-and-forth.
Finally, treat the website as a preparation tool rather than the controlling product drawing. Measurements and diagrams narrow the family and help organize the RFQ; the released drawing defines the ordered configuration. That distinction is especially important where pan skew, binding, difficult cleaning or contact with guides could have more than one mechanical cause.
Use How to Select Attachments for Bakery Pans as a machine-level question, not just a chain inspection. Compare the loaded and return runs, drive and tail ends, and any transfer or carrier transition in pan conveyors through proofing, baking or return handling. Document whether pan skew, binding, difficult cleaning or contact with guides is distributed along the strand or repeats at one location. That pattern helps separate progressive joint wear from alignment, guide, sprocket or carrier problems that a new chain alone will not correct.
The working record should include hole pattern, support height, offset, pan pitch, chain centers and attachment interval. Mark which values are fixed by the existing machine and which values can be changed to improve service. The central engineering focus is matching pan support geometry to the chain while allowing assembly, cleaning and thermal movement. When a legacy part number conflicts with field measurements, hold the RFQ until the installed interface and the controlled drawing can be reconciled.
A useful enquiry combines commercial quantity with the technical package: pan drawing, attachment sketch, chain centers, load, temperature and cleaning method. Also state whether the request is a direct replacement, a planned modification or a new machine design. The release objective is to start from the pan support/load path and work back to the attachment rather than choosing from appearance. This reduces quote revisions and prevents a visually similar chain from being treated as interchangeable before geometry and duty have been checked.
Bruk den gamle referansen hvis tilgjengelig, men bekreft den installerte geometrien og oppgaven. Maskinmodifikasjoner, tidligere utskiftninger eller slitasje kan gjøre et delenummer alene ufullstendig.
Bruk en flertonemåling over et praktisk antall lenker og registrer metoden. Sammenlign den med nominell tone og maskinens vedlikeholdsgrenser i stedet for å stole på én måling av tilstøtende lenker.
Når det er tannslitasje, hekting, problemer med kjedejustering eller gjentatt for tidlig kjedeslitasje, fungerer kjedet og tannhjulet som et inngripende system.

























