Where This Chain Family Fits
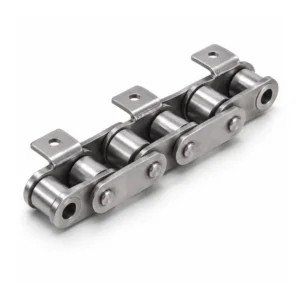
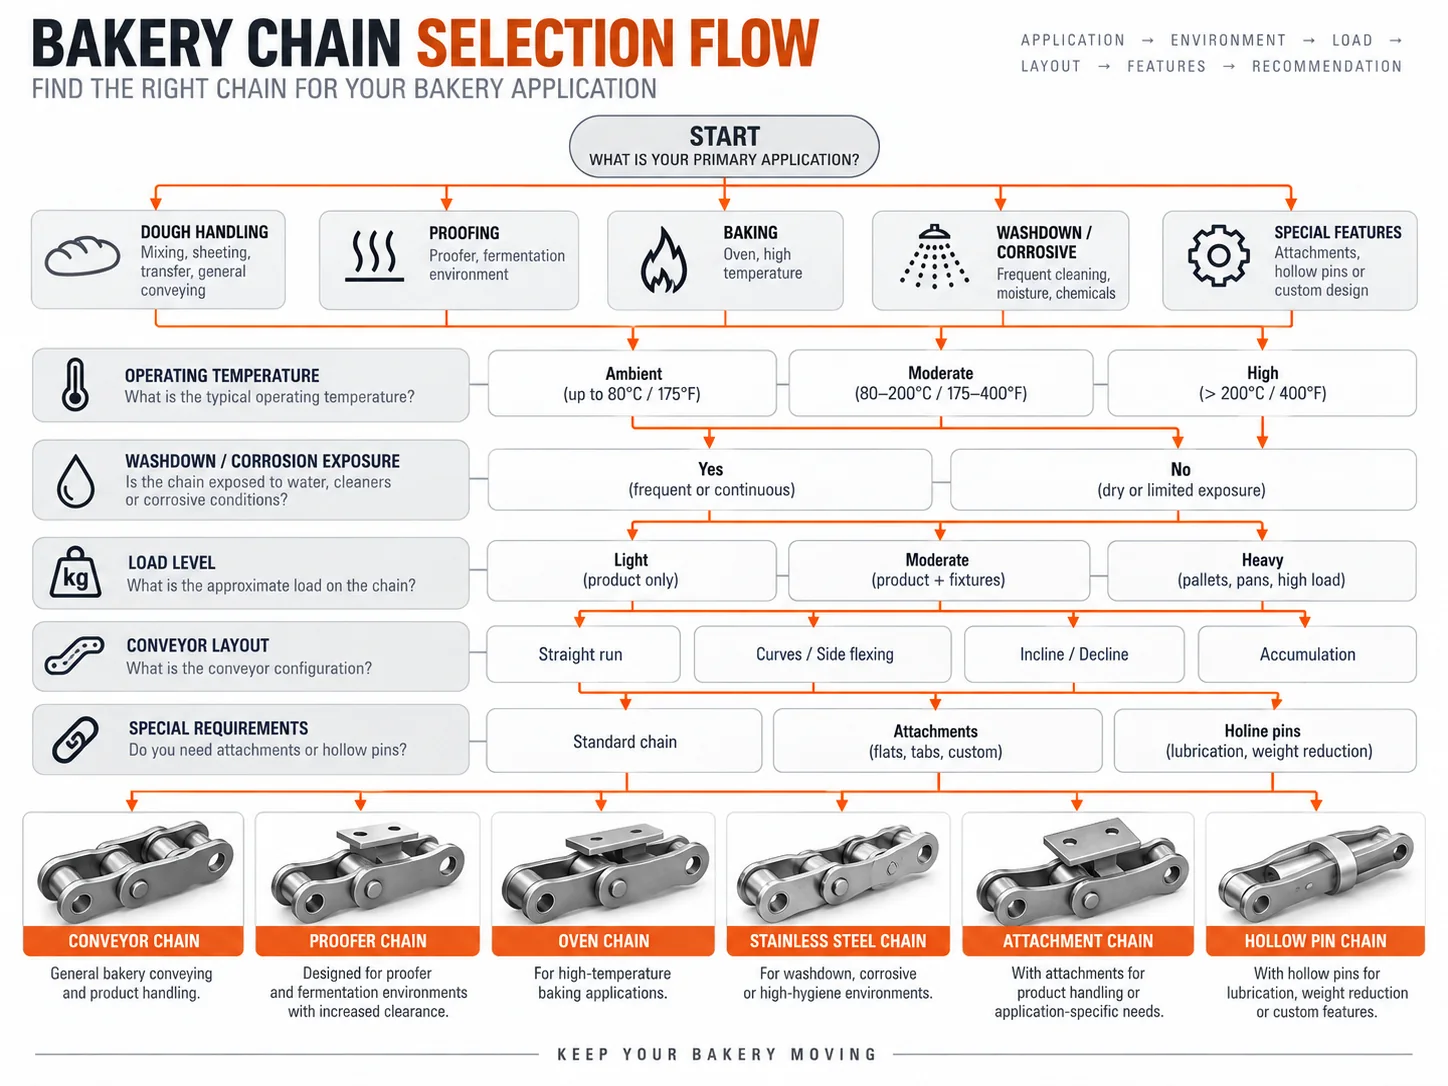
Hollow Pin Bakery Chains are a practical starting point for systems using cross rods, carrier bars or application-specific fixtures through the pin axis. In an industrial bakery, one production line can move from humid proofing to hot baking, ambient cooling and dry packaging. Each section can impose a different combination of load, temperature, washdown and carrier requirements, so the chain family should be matched to the actual machine zone.
For replacement projects, begin with pitch, inside width, roller or bush diameter, pin diameter and plate geometry. Then record the attachment pattern and chain-center spacing. For new equipment, also define conveyor speed, supported mass, start/stop frequency, take-up arrangement and expected cleaning routine.
Construction and Interface
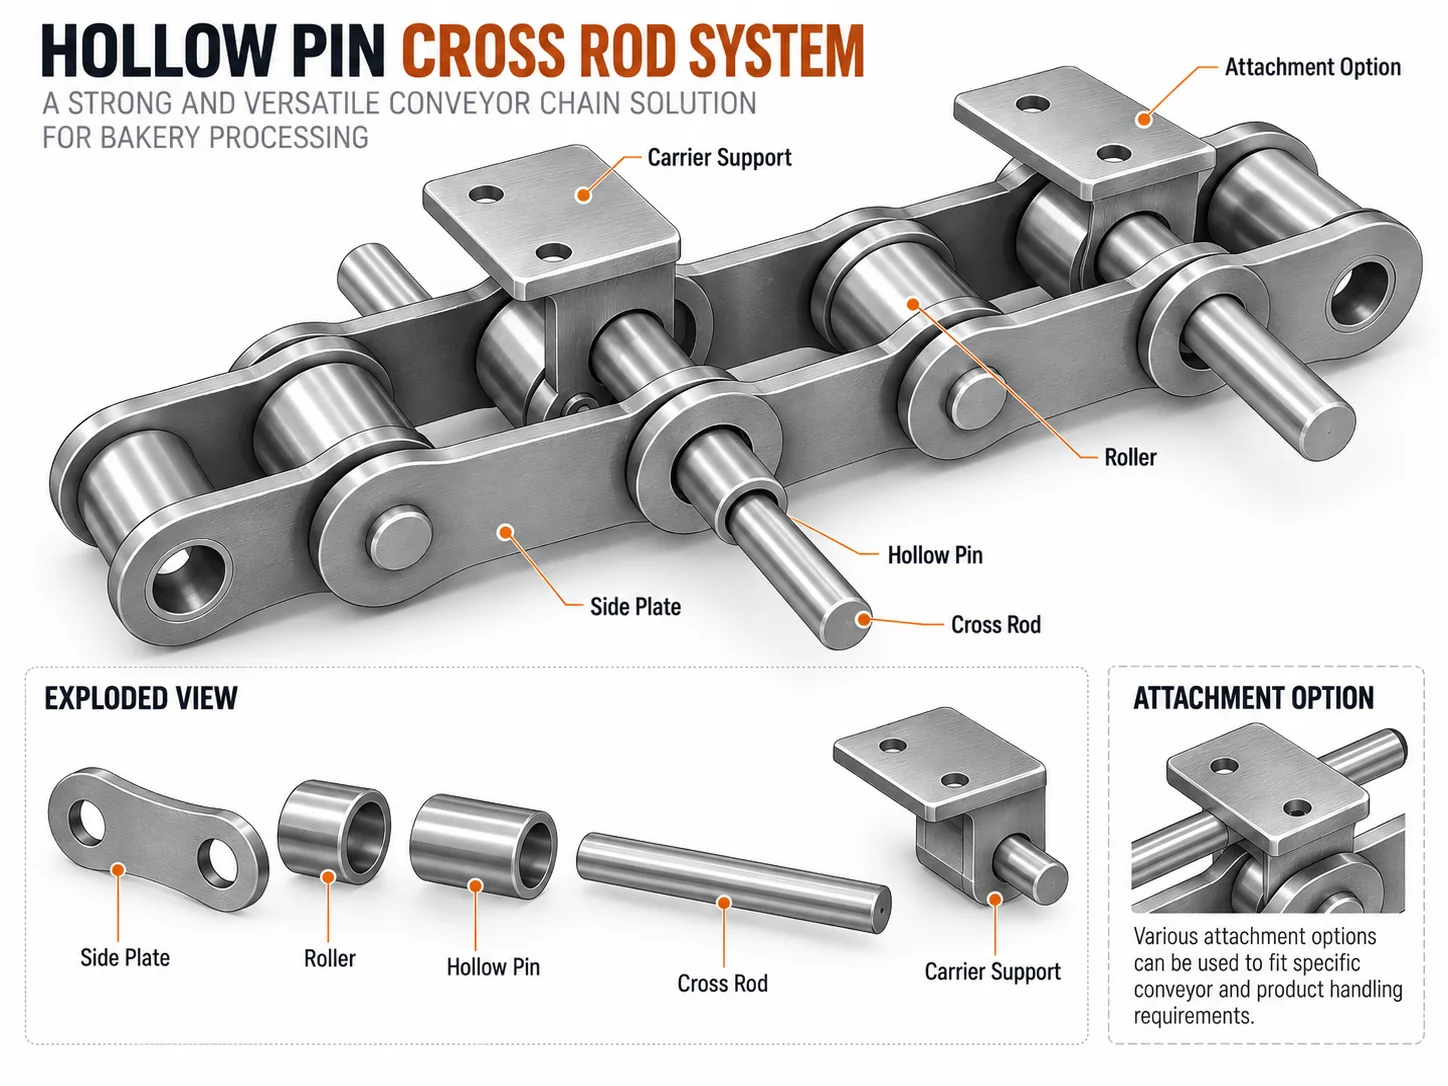
The base chain provides articulation and sprocket engagement, while plates, pins, bushes, rollers and attachments define how the chain carries load and interfaces with the machine. For hollow pin bakery chain, check whether the conveyor needs a standard roller, larger roller, hollow pin, extended pin, top plate or dedicated attachment. The visible attachment is only one part of the assembly; its offset and spacing must also match the carrier.
Use the technical illustration as a configuration guide. Final dimensions, material, clearances and ratings are confirmed on the ordered drawing for the chosen series and duty.
Product Options
Bakery Application Conditions
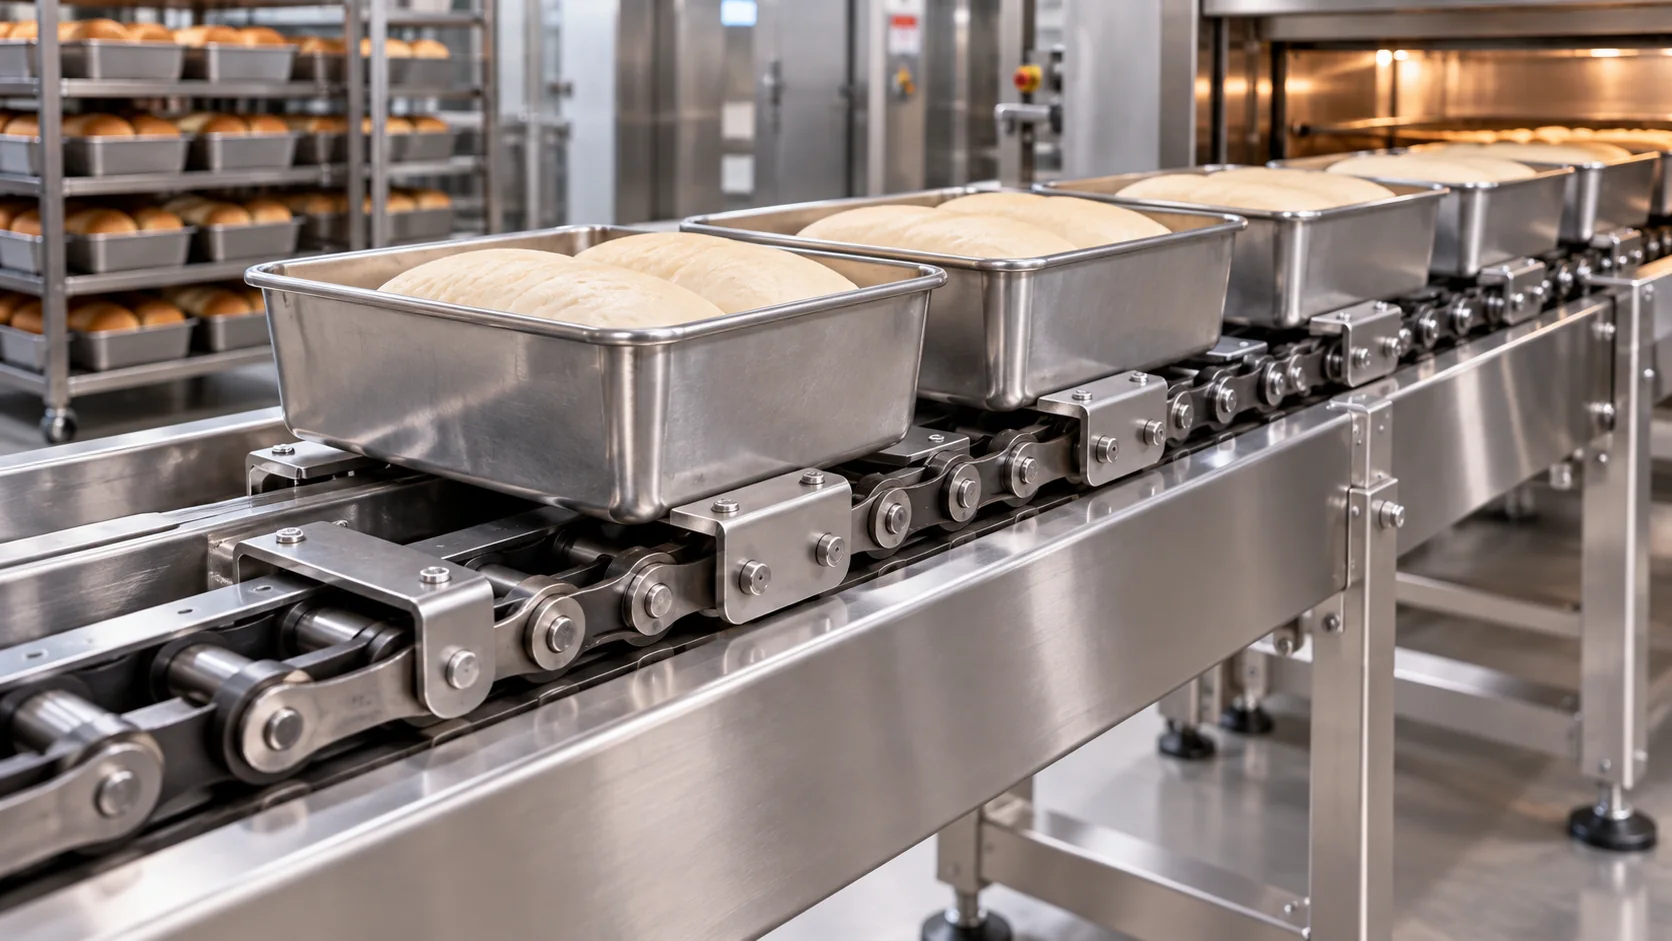
Bakery equipment combines food-handling requirements with mechanical drive requirements. Consider condensate near proofers, radiant and conducted heat near ovens, moisture during washdown, flour or crumbs around transfer zones, and the possibility that trays or pans create eccentric loads. A suitable chain should work with the sprocket, guide track and take-up system as a complete mechanism.
When the application crosses more than one environment, define the most demanding zone and the time spent in it. That information helps determine whether a stainless configuration, special clearance, custom attachment or different carrier arrangement should be reviewed.
Selection Checklist
Chain geometry
Measure pitch, inside width, roller or bush diameter, pin diameter, plate height and overall width.
Carrier interface
Record attachment style, hole pattern, offset, cross rods, pan supports and attachment interval.
Operating environment
State temperature range, humidity, washdown frequency, cleaning chemistry, contamination and lubrication constraints.
Machine integration
Confirm sprocket tooth count, center distance, take-up travel, guides, chain-center spacing, speed and supported load.
Procurement and Replacement
Send a photo of the complete chain, a side view, an end view and a close-up of the attachment together with measured dimensions. If an existing drawing is available, include it even when the original supplier reference is unknown. This reduces the risk of matching a chain by pitch alone.
For related configuration work, review our chain identification guide before submitting the RFQ. It explains which dimensions are most useful for screening a replacement.
Ordreplanlegging og kommersielle vilkår
MOQ: evaluert etter produkttype, produksjonsbatch og ordreverdi. Standard katalogvarer bruker vanligvis mengdebaserte produksjonsminimum, mens store eller høyverdige varer kan gjennomgås etter prosjektverdi.
Prøver: Nye kunder kan be om 1–5 stk. når den valgte kjedetypen og produksjonsruten passer. Priseksempler og gjennomførbarhet bekreftes før produksjon.
Blandede bestillinger: Flere modeller kan kombineres mot en ordreverdi på omtrent USD 1500, avhengig av prosesskompatibilitet og pakkekrav.
Svært små mengder: 1–2 stk. vurderes kun for godkjente prøve-, erstatnings- eller ingeniørsaker; rutinemessige detaljhandelsbestillinger aksepteres ikke, og spesialhåndtering kan føre til høyere enhetskostnad.
Leveringstid: standardvarer vanligvis 10–25 virkedager; spesialtilpassede komponenter 20–45; prosjektbasert utstyr eller komplekse pakker 45–120, etter tegning og ordrebekreftelse.
Handelsvilkår: EXW, FOB, CIF og DAP støttes vanligvis. FCA, CFR, CPT, CIP og DDP kan diskuteres for destinasjon og forsendelsesplan.
Fit Checks Before You Specify
Start with the machine zone
Use conveyors using cross rods, shafts or removable carrier fixtures through the chain as the first boundary for selection. The same bakery line can move through very different conditions, so define where this chain actually runs and how long it remains in that zone before comparing series or materials.
Record the environment
Describe proofing, cooling and transfer duties where carrier change or cleaning access matters. Those conditions influence joint freedom, corrosion exposure, dimensional growth and lubrication practice. A material name by itself does not replace an operating-condition review.
Map the carrier interface
Document hollow pins, cross rods, retaining hardware and parallel chain strands. Record hole centers, offsets, strand spacing and repeated intervals where applicable. The chain must preserve articulation while the carrier transfers load into the plates, pins or attachments.
Verify the complete mechanism
Selection should confirm pin bore, cross-rod fit, strand spacing, articulation and retention method. Also inspect sprockets, guides and take-up travel. A replacement chain can be dimensionally close and still perform poorly if the mating system is worn or misaligned.
| Sjekke | Hvorfor det er viktig | Hva som skal sendes eller bekreftes |
|---|---|---|
| Geometry | Pitch, inside width, roller/bush diameter, pin dimensions and plate envelope control interchangeability. | Measure several pitches and include side and end photographs. |
| Driftstilstand | The main concerns here are proofing, cooling and transfer duties where carrier change or cleaning access matters. | State normal and peak conditions, cleaning practice and lubrication restrictions. |
| Carrier/load path | Check hollow pins, cross rods, retaining hardware and parallel chain strands and the way the load enters the chain. | Send the carrier drawing, attachment interval and supported mass or force where known. |
| Risk check | Watch for cross-rod binding, unequal strand loading and loss of articulation from over-tight fixtures before approving a replacement. | Include sprocket tooth count/condition, guide layout and take-up position. |
Ofte stilte spørsmål
Can the same bakery chain be used in a proofer and an oven?
Sometimes the geometry may be related, but temperature, humidity, clearance and material requirements can differ substantially. Treat each machine zone as a separate duty condition before confirming a common chain.
Can attachments be changed without changing the base chain?
In many families several attachment styles are possible, but hole pattern, offset, plate load and manufacturing process must be checked. Send the carrier drawing and required interval.
How do I request a replacement match?
Provide pitch, inside width, roller or bush diameter, pin size, overall width, attachment dimensions, photos and the operating conditions. A sample section can be useful when measurements are difficult.

























