Product Description
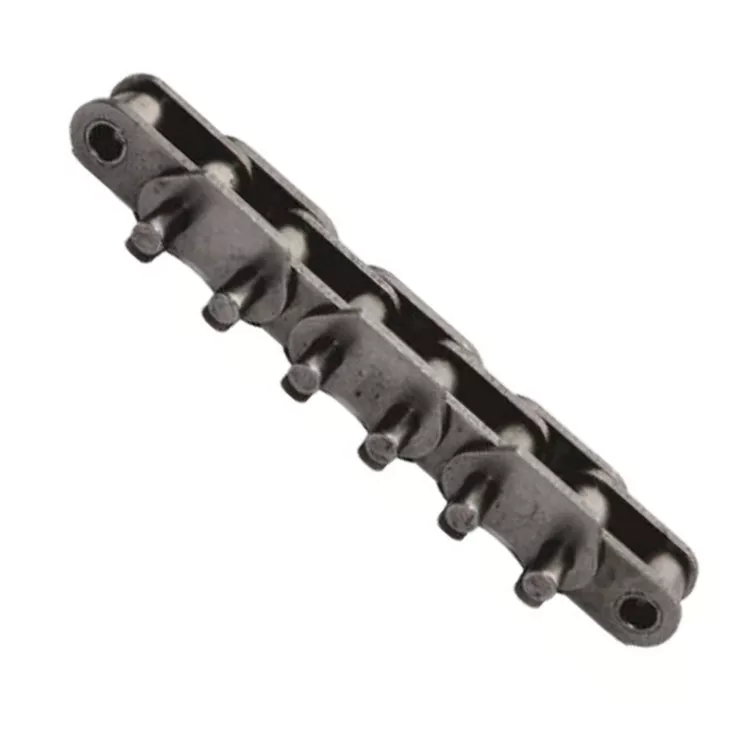
Duplex Short Pitch Precision Conveyor Roller Chain Transmission Chain (DIN764)
SHORT PITCH PRECISSION ROLLER CHAINS (B SERIES)
Material: Alloy Steel
Surface Treatment: Shot Peening / Blacking / Blueing
Main Application: Idustry machinery
ANSI CHAIN NO.: 05B-2 06B-2 10B-2 12B-2 16B-2 20B-2 24B-2 28B-2 32B-2 40B-2 48B-2 56B-2 72B-2
Pitch:8 9.525 12.7 15.875 19.05 25.4 31.75 38.1 44.45 50.8 63.5 76.2 88.9 101.6 114.3
| Product name | Duplex Short Pitch Precision Roller Chain (B series) Chain (DIN764) |
| Materials Available | 1. Stainless Steel: SS201, SS303, SS304, SS316, SS416, SS420 |
| 2. Steel:C45(K1045), C46(K1046),C20 | |
| 3. Brass:C36000 ( C26800), C37700 ( HPb59), C38500( HPb58), C27200(CuZn37), C28000(CuZn40) | |
| 4. Bronze: C51000, C52100, C54400, etc | |
| 5. Iron: 1213, 12L14,1215 | |
| 6. Aluminum: Al6061, Al6063 | |
| 7.OEM according to your request | |
| Surface Treatment | Annealing, natural anodization, heat treatment, polishing, nickel plating, chrome plating, znic plating,yellow passivation, gold passivation, satin, Black surface painted etc. |
| Products Available | sprockt chains, pulley, shafts(axles, spline shafts, dart shafts),gears (pinions, wheels gear rack) bearing, bearing seat, bushing, coupling, lock assembly etc. |
| Processing Method | CNC machining, punch,turning, milling, drilling, grinding, broaching, welding and assembly |
| QC : | Technicians self-check in production,final-check before package by professional Quality inspector |
| Size | Drawings |
| Package | Wooden Case/Container and pallet, or as per customized specifications |
| Certificate | ISO9001:2008 , ISO14001:2001,ISO/TS 16949:2009 |
| Advantage | Quality first Service superior , Advanced equipment,Experienced workers,Perfect testing equipment |
| Lead Time | 15-25days samples. 30-45days offcial order |
1. Are you manufacturer or trade Company?
We are a factory founded in 1991 with trade team for international service.
2. What terms of payment you usually use?
T/T 30% deposit and 70% against document, Western Union, L/C at sight
3. what is your lead time for your goods?
Normally 45 days after confirmed order. 30 days could be available in low season for some items (during May to July), and 65 days during new year and hot season ( Jan to March).
4. Do you attend any Show?
We attend Hannover show in Germany, NMW in Austrilia, Canton fair, PTC, in China and many other special furniture shows.
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Usage: | Transmission Chain |
|---|---|
| Material: | Alloy/Carbon Steel |
| Surface Treatment: | Polishing |
| Feature: | Heat Resistant |
| Chain Size: | 1/2"*3/32" |
| Structure: | Roller Chain |
| Customization: |
Available
| Customized Request |
|---|

What are the considerations for selecting a corrosion-resistant conveyor chain?
When selecting a corrosion-resistant conveyor chain, several considerations should be taken into account to ensure optimal performance and longevity in corrosive environments. Here are the key factors to consider:
– Material Selection:
Choose a conveyor chain material that is resistant to the specific corrosive agents present in the environment. Stainless steel, plastic, and special coatings such as zinc or nickel plating are commonly used for their corrosion resistance properties.
– Corrosion Resistance Ratings:
Review the corrosion resistance ratings of different chain materials and coatings. Look for industry standards such as ASTM or ISO ratings that indicate the material’s resistance to specific corrosive substances or environmental conditions.
– Environmental Factors:
Consider the specific environmental factors that contribute to corrosion, such as humidity, temperature, presence of chemicals or solvents, and exposure to saltwater or acids. Evaluate how these factors may impact the chain’s corrosion resistance requirements.
– Coating or Surface Treatment:
If using a metal chain, consider applying additional coatings or surface treatments to enhance its corrosion resistance. Options may include electroplating, powder coating, or using specialized anti-corrosion coatings.
– Compatibility with Cleaning Methods:
Ensure that the selected chain material is compatible with the cleaning methods and chemicals used in the application. Some corrosive-resistant materials may require specific cleaning procedures to maintain their performance and longevity.
– Operational Considerations:
Take into account the load capacity, speed, and operational requirements of the conveyor system. Ensure that the corrosion-resistant chain can withstand the mechanical stresses and operational demands without compromising its corrosion resistance properties.
– Cost-Effectiveness:
Weigh the initial cost and long-term benefits of using a corrosion-resistant conveyor chain. While corrosion-resistant materials may have a higher upfront cost, they can significantly reduce maintenance, replacement, and downtime costs associated with corrosion-related failures.
By considering these factors, you can select a corrosion-resistant conveyor chain that is well-suited for the specific corrosive environment, ensuring reliable and durable performance in applications such as chemical processing, food production, wastewater treatment, or outdoor environments.
How does a conveyor chain handle different types of materials?
A conveyor chain is designed to handle a wide variety of materials in diverse industrial applications. It is capable of efficiently transporting different types of materials, including:
1. Bulk Materials: Conveyor chains are commonly used to handle bulk materials such as grains, coal, ores, aggregates, and powders. The design of the chain, including the spacing and shape of the links, helps prevent material spillage and ensures smooth and consistent flow.
2. Packaged Goods: Conveyor chains are also used for conveying packaged goods such as boxes, cartons, crates, and pallets. They provide a stable and reliable method of transporting these items along the production line, reducing manual handling and increasing productivity.
3. Small Parts: Conveyor chains with specialized attachments or small-pitch configurations are suitable for handling small parts or components. These chains ensure precise positioning and gentle transport of delicate or intricate items.
4. Heavy-Duty Loads: Industrial conveyor chains are capable of handling heavy-duty loads, such as automotive parts, machinery components, and large equipment. They are engineered to withstand the weight and stress of these objects, providing reliable and efficient material handling in demanding environments.
5. Food and Beverage Products: Conveyor chains used in the food and beverage industry are designed to meet strict hygiene and safety standards. They are constructed from materials that are resistant to corrosion, easy to clean, and compliant with food-grade regulations. These chains ensure the safe and contamination-free handling of food products.
6. Hazardous Materials: Conveyor chains can be used to safely transport hazardous materials, such as chemicals or waste products. Specialized chains with additional safety features, such as sealed housings or containment systems, are utilized to minimize the risk of spills or leaks.
Conveyor chains can be customized with different chain configurations, attachments, and accessories to accommodate specific material characteristics and handling requirements. The selection of the appropriate chain type, material, and design parameters ensures optimal performance and efficient material handling for a wide range of materials.

What are the advantages of using a conveyor chain in material handling?
Conveyor chains offer numerous advantages in material handling applications, making them a preferred choice in various industries. Here are some of the key advantages:
- Efficient Transportation: Conveyor chains provide a continuous and reliable means of transporting materials, ensuring a smooth flow throughout the production or distribution process. They can handle both light and heavy loads, enabling efficient movement of items of different sizes and weights.
- Increased Productivity: By automating the material handling process, conveyor chains help increase productivity and operational efficiency. They eliminate the need for manual handling and reduce human effort, allowing employees to focus on other tasks, resulting in higher throughput and reduced labor costs.
- Flexibility and Customization: Conveyor chains can be designed and configured to meet specific material handling requirements. They are available in various lengths, widths, and configurations, allowing for customization based on the layout and space constraints of the facility. Additionally, different types of conveyor chains can be selected to handle specific materials or accommodate special handling needs.
- Improved Safety: Conveyor chains enhance workplace safety by reducing the risk of manual lifting and carrying heavy loads. They provide a controlled and controlled movement of materials, minimizing the chances of accidents and injuries. Additionally, safety features such as emergency stop buttons, guardrails, and sensors can be incorporated into the conveyor system to further enhance safety.
- Space Optimization: Conveyor chains utilize vertical and horizontal space efficiently, making them ideal for facilities with limited floor space. They can be designed to navigate corners, inclines, and declines, allowing for optimized layout and maximizing the use of available space.
- Versatility: Conveyor chains are versatile and can handle a wide range of materials, including bulk items, packaged goods, fragile items, and irregularly shaped objects. They can accommodate different types of conveyance methods such as flat, inclined, or spiral conveyors, providing flexibility in material handling processes.
- Improved Inventory Control: Conveyor chains enable better inventory control by facilitating the smooth movement and tracking of materials. They can be integrated with barcode scanners, RFID technology, or other tracking systems to monitor the flow of goods and provide real-time information on inventory levels.
- Reduced Material Damage: Conveyor chains help minimize material damage during handling and transportation. They provide a stable and controlled movement, reducing the risk of items falling or getting damaged due to manual handling or rough transportation methods.
The advantages of using a conveyor chain in material handling include improved efficiency, productivity, safety, space utilization, and inventory control, leading to cost savings and enhanced overall operational performance.


editor by CX 2024-03-28

























