Product Description
About Factory
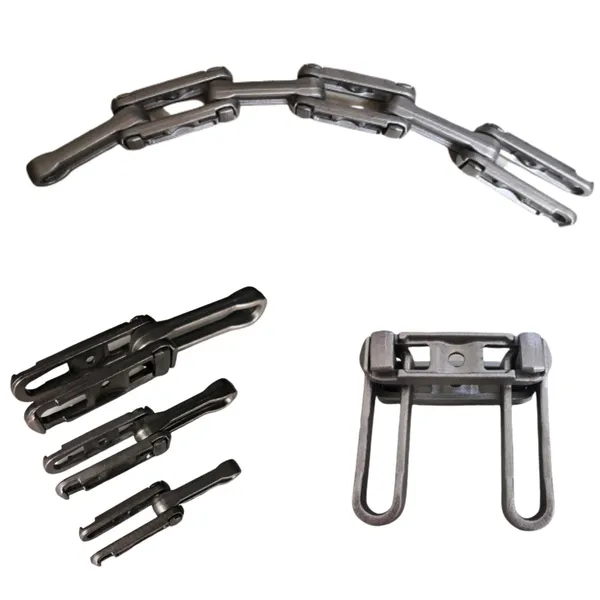
With more than 18 years’ histiory, we are a professinal manufacturer for drop forged products such as forged chain (X348 X458 X658 X678 X698 F100 F160), scraper chain (10160, 14218, 14226, 142N), conveyor trolley (X348, X458, X678, XT160), and drive chain (X348, X458, X678), and so forth standard moulds of chain.
Besides, we can also produce as per your drawing or sample, special link chain, pusher, pin and plate, according to customers’ unique requirements.
Product Description
1) Material: Alloy steel, 40Cr, 42CrMo and so on.
2) Types: Standard types, X348 X458 X678, and so on. (Or as per your drawing)
3) Process: Moulding→Forging→Polishing & Blasting→Fine machining→Heat treatment→Blasting→Inspecting & testing→Packing
Product Show
Technical Data
| Model | Dimension | Weight (Kg) | Material | Hardness | Working Load (KN) | Limit Load (KN) | ||||||
| P | T | C | S | F | R | D | ||||||
| 10160B | 101.6 | 24 | 36 | 13 | 14 | 6 | 14 | 0.32 | 20CrMnTi | Surface HRC56-64° Depth 0.6-1.2mm |
18 | 100 |
| 10160 | 101.6 | 30 | 36 | 13 | 14.5 | 9 | 14 | 0.36 | 20CrMnTi | Surface HRC56-64° Depth 0.6-1.2mm | 21.6 | 120 |
| 14218 | 142 | 42 | 50 | 19 | 20.5 | 11 | 25 | 1.15 | 20CrMnTi | Surface HRC56-64° Depth 0.6-1.2mm | 48.6 | 270 |
| 14226 | 142 | 62 | 50 | 28 | 30 | 15 | 25 | 1.75 | 20CrMnTi | Surface HRC56-64° Depth 0.6-1.2mm | 61.2 | 340 |
| 2571 | 200 | 66 | 60 | 30 | 32 | 18 | 30 | 2.8 | 20CrMnTi | Surface HRC56-64° Depth 0.6-1.2mm | 72 | 400 |
| 26014 | 260 | 70 | 75 | 31 | 33 | 20 | 34 | 5.2 | 20CrMnTi | Surface HRC56-64° Depth 0.6-1.2mm | 135 | 750 |
| 142N | 142 | 43 | 50 | 19 | 22 | 12.5 | 25 | 1.2 | 40Cr | Quench HRC36-44° | 75.6 | 420 |
| 150D | 142 | 42 | 50 | 19 | 20.5 | 11 | 25 | 1.15 | 40Cr | Quench HRC36-44° | 75.6 | 420 |
| MG20 | 200 | 70 | 50 | 27 | 29 | 17 | 35 | 3.78 | 40Cr | Quench HRC36-44° | 144 | 800 |
| MG20B | 200 | 70 | 50 | 27 | 29 | 17 | 30 | 3.82 | 40Cr | Quench HRC36-44° | 140.4 | 780 |
| MG20C | 200 | 70 | 50 | 27 | 29 | 17 | 28 | 3.85 | 40Cr | Quench HRC36-44° | 122.4 | 680 |
| MS32 | 200 | 42 | 50 | 20 | 22 | 12 | 25 | 1.4 | 40Cr | Quench HRC36-44° | 75.6 | 420 |
| MS55 | 200 | 80 | 70 | 35 | 38 | 25 | 28 | 4.36 | 40Cr | Quench HRC36-44° | 138.6 | 770 |
| 3006 | 200 | 65 | 70 | 30 | 33 | 24 | 32 | 3.6 | 40Cr | Quench HRC36-44° | 160.2 | 890 |
| MS63 | 250 | 70 | 80 | 30 | 33 | 20 | 32 | 4.93 | 40Cr | Quench HRC36-44° | 147.6 | 820 |
| S16 | 100 | 30 | 27 | 15 | 16 | 8 | 14 | 0.3 | 40Cr | Quench HRC36-44° | 16 | 88 |
| S20 | 125 | 34 | 33 | 17 | 18 | 8 | 17 | 0.37 | 40Cr | Quench HRC36-44° | 19.4 | 108 |
| S25 | 160 | 48 | 39 | 23 | 25 | 13 | 20 | 1.28 | 40Cr | Quench HRC36-44° | 55.8 | 310 |
| S30 | 142 | 46 | 49 | 22 | 23.5 | 14 | 25 | 1.3 | 40Cr | Quench HRC36-44° | 91.8 | 510 |
| Z16 | 100 | 40 | 35 | 18 | 20 | 12 | 17 | 0.4 | 40Cr | Quench HRC36-44° | 32.4 | 180 |
| Z20 | 125 | 50 | 46 | 24 | 26 | 15 | 20 | 0.67 | 40Cr | Quench HRC36-44° | 59.4 | 330 |
| Z20D | 125 | 52 | 60 | 24 | 26 | 16 | 26 | 1.15 | 40Cr | Quench HRC36-44° | 82.8 | 460 |
| Z25 | 160 | 58 | 55 | 28 | 30 | 18 | 25 | 2.25 | 40Cr | Quench HRC36-44° | 82.8 | 460 |
| Z25D | 160 | 66 | 64 | 29 | 31 | 22 | 28 | 2.6 | 40Cr | Quench HRC36-44° | 120.6 | 670 |
| Z30 | 142 | 64 | 50 | 29 | 30.5 | 18 | 25 | 1.8 | 40Cr | Quench HRC36-44° | 111.6 | 620 |
Products & Testing Equipments
Products Application
Packing & Delivery
Why Choose Us?
1. We are engaged in chain industry over 15 years with rich market experience. We keep improving production techniques. All the products have longer working life and have passed the market test.
2. We can design the correct chains with high quality material, good abrasion resistance, good corrosion, high strengthen and etc as per your request or the chain application.
3. We are the chain manufacturer; you can directly purchase the product from us with low price and high quality.
4. We have a professional team for international trade, they have abundant experiences and are always ready to solve problems for customers. So you have nothing to worry about.
5. We have the long-term cooperative forwarder who can give us the lowest freight. And it can help you to save the freight. What’s more, for the FCL, we will design the packages as per the container sizes with the largest capacity to save the shipping cost for both of us.
| Standard or Nonstandard: | Standard |
|---|---|
| Application: | Textile Machinery, Garment Machinery, Conveyer Equipment, Packaging Machinery, Electric Cars, Motorcycle, Food Machinery, Mining Equipment, Agricultural Machinery, Coating, Spraying, Mining, Slaughtering, Assembly |
| Surface Treatment: | Polishing |
| Structure: | Combined Chain |
| Material: | Alloy |
| Type: | Cranked Link Chain |
| Samples: |
US$ 5/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
Can a conveyor chain be used in cleanroom environments?
Yes, conveyor chains can be used in cleanroom environments with proper selection and design considerations. Cleanroom environments require stringent control of airborne particles, such as dust, microbes, and contaminants, to maintain high levels of cleanliness. Here are some factors to consider when using a conveyor chain in a cleanroom:
1. Material Selection:
– Choose a conveyor chain made from materials that are compatible with cleanroom requirements. Stainless steel, plastic, or special coatings are commonly used for their clean and non-contaminating properties.
– Avoid materials that generate excessive particles or contaminants, such as certain types of lubricants or chain coatings.
2. Design Considerations:
– Design the conveyor chain system to minimize particle generation. This includes smooth surfaces, rounded edges, and avoiding areas that can trap or accumulate particles.
– Use sealed or enclosed chain designs to prevent the release of lubricants or contaminants.
– Consider the integration of additional features, such as covers or guards, to further protect the chain and prevent particle ingress.
3. Cleaning and Maintenance:
– Establish a cleaning and maintenance protocol specific to the cleanroom environment. This may include regular cleaning and sanitization procedures to maintain cleanliness standards.
– Use cleaning agents and procedures that are approved for cleanroom use and do not introduce contaminants.
– Regularly inspect the conveyor chain system for any signs of wear, damage, or contamination. Promptly address any issues to ensure the chain’s reliability and cleanliness.
4. Compliance with Cleanroom Standards:
– Ensure that the conveyor chain system meets the cleanliness and particle generation requirements of the specific cleanroom standards or classifications in which it will be used.
– Comply with relevant industry guidelines and regulations, such as ISO standards, when selecting and using conveyor chains in cleanroom environments.
By considering these factors and implementing proper material selection, design considerations, cleaning protocols, and compliance with cleanroom standards, a conveyor chain can be effectively used in cleanroom environments while maintaining the required cleanliness levels.
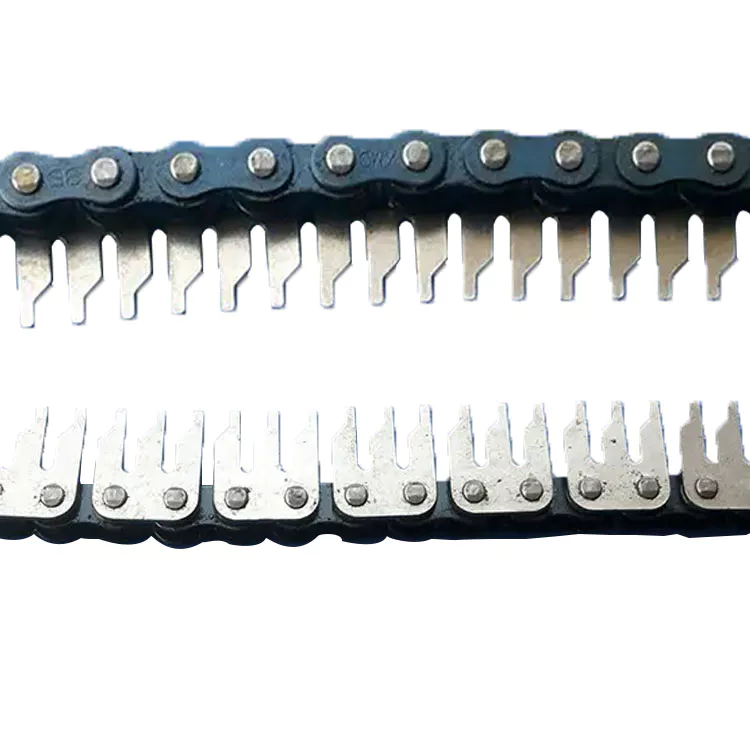
Can a conveyor chain be used in food processing applications?
Yes, a conveyor chain can be used in food processing applications. Conveyor chains play a crucial role in the efficient and hygienic handling of food products throughout the production process. Here are some key points to consider:
1. Food-Grade Materials: Conveyor chains used in food processing applications are typically made from food-grade materials such as stainless steel or plastic. These materials are corrosion-resistant, easy to clean, and comply with food safety regulations.
2. Hygiene Considerations: Food processing environments require high standards of hygiene. Conveyor chains designed for food applications incorporate features such as smooth surfaces, open link designs, and easy disassembly for thorough cleaning. They may also have specialized coatings or treatments to prevent bacterial growth.
3. Sanitary Design: Conveyor chains for food processing applications are designed with minimal crevices or joints to prevent food particles from getting trapped. They may have self-draining capabilities to remove excess fluids or debris.
4. Product Integrity: Conveyor chains in food processing applications ensure gentle handling of delicate food products to avoid damage or contamination. They can be equipped with accessories like cleats, side guards, or modular belt systems to securely hold and transport items of various shapes and sizes.
5. High Temperature and Washdown Capabilities: Some food processing applications require conveyor chains to withstand high temperatures during cooking, baking, or sterilization processes. Specialized chains with heat-resistant materials or coatings are available. Additionally, conveyor chains used in food processing should be capable of withstanding frequent washdowns and cleaning with water or cleaning agents.
6. Compliance with Standards: Conveyor chains used in food processing applications must comply with industry-specific standards such as FDA (Food and Drug Administration) regulations, HACCP (Hazard Analysis Critical Control Point) guidelines, and other food safety certifications.
When selecting a conveyor chain for food processing applications, it is important to consider the specific requirements of the production line, including the type of food being handled, the operating conditions, and the necessary sanitary standards. Proper maintenance and regular cleaning protocols should also be implemented to ensure food safety and product integrity.
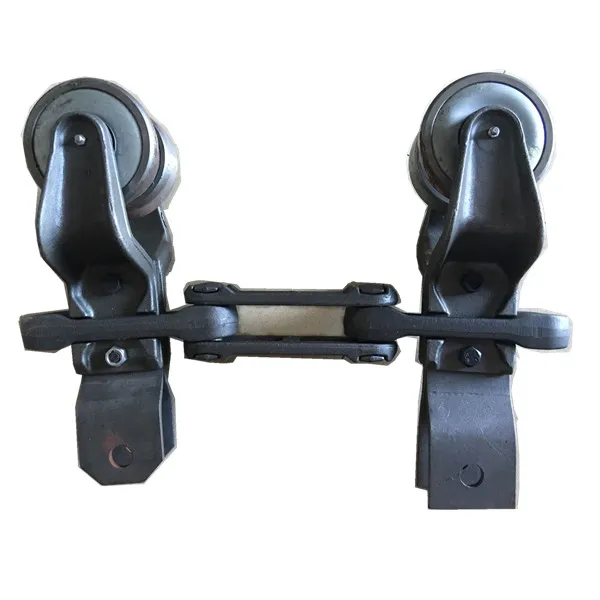
How do you optimize the efficiency of a conveyor chain system?
To optimize the efficiency of a conveyor chain system, several factors should be considered and implemented:
1. System Design: Ensure that the conveyor system is properly designed to minimize energy losses, reduce friction, and optimize material flow. Consider factors such as conveyor length, incline/decline angles, and the number and placement of drive units to achieve efficient operation.
2. Chain Selection: Select the appropriate conveyor chain based on the specific application requirements, such as load capacity, speed, and environmental conditions. Consider factors like chain material, pitch, and strength to ensure optimal performance and longevity.
3. Lubrication: Proper lubrication of the conveyor chain is essential for reducing friction, wear, and power consumption. Choose the right lubricant for the application and regularly maintain the lubrication levels to ensure smooth chain operation.
4. Tensioning and Alignment: Regularly inspect and adjust the tension and alignment of the conveyor chain to prevent excessive slack or tightness. Proper tensioning and alignment help to minimize chain wear, reduce energy losses, and ensure consistent performance.
5. Preventive Maintenance: Implement a regular maintenance program to identify and address potential issues before they escalate. This includes cleaning the chain, inspecting sprockets and guides, replacing worn components, and checking for proper tension and alignment. A well-maintained system reduces downtime and extends the life of the chain.
6. System Monitoring: Utilize monitoring tools such as sensors, cameras, or automated systems to track the performance of the conveyor chain system. Monitoring can provide valuable data on chain tension, alignment, speed, and power consumption, allowing for timely adjustments and optimization.
7. Training and Operator Awareness: Train operators on best practices for operating and maintaining the conveyor chain system. Promote awareness of energy efficiency, proper handling, and safety protocols to ensure optimal system performance.
By considering these factors and implementing appropriate measures, the efficiency of a conveyor chain system can be optimized, leading to improved productivity, reduced energy consumption, and longer chain life.


editor by CX 2023-07-26

























