Bakery Proofing Systems
Process conditions, suitable chain families and RFQ data.
View ApplicationỨng dụng
Match the conveyor chain to the bakery process, operating environment and carrier interface.
Process conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProcess conditions, suitable chain families and RFQ data.
View ApplicationProofing, baking, cooling and packaging are not one mechanical duty. Humidity, temperature, product support, cleaning and access change throughout the line. Application pages help capture those differences before a chain family is selected.
For the next step, use the bakery conveyor chain selection guide.
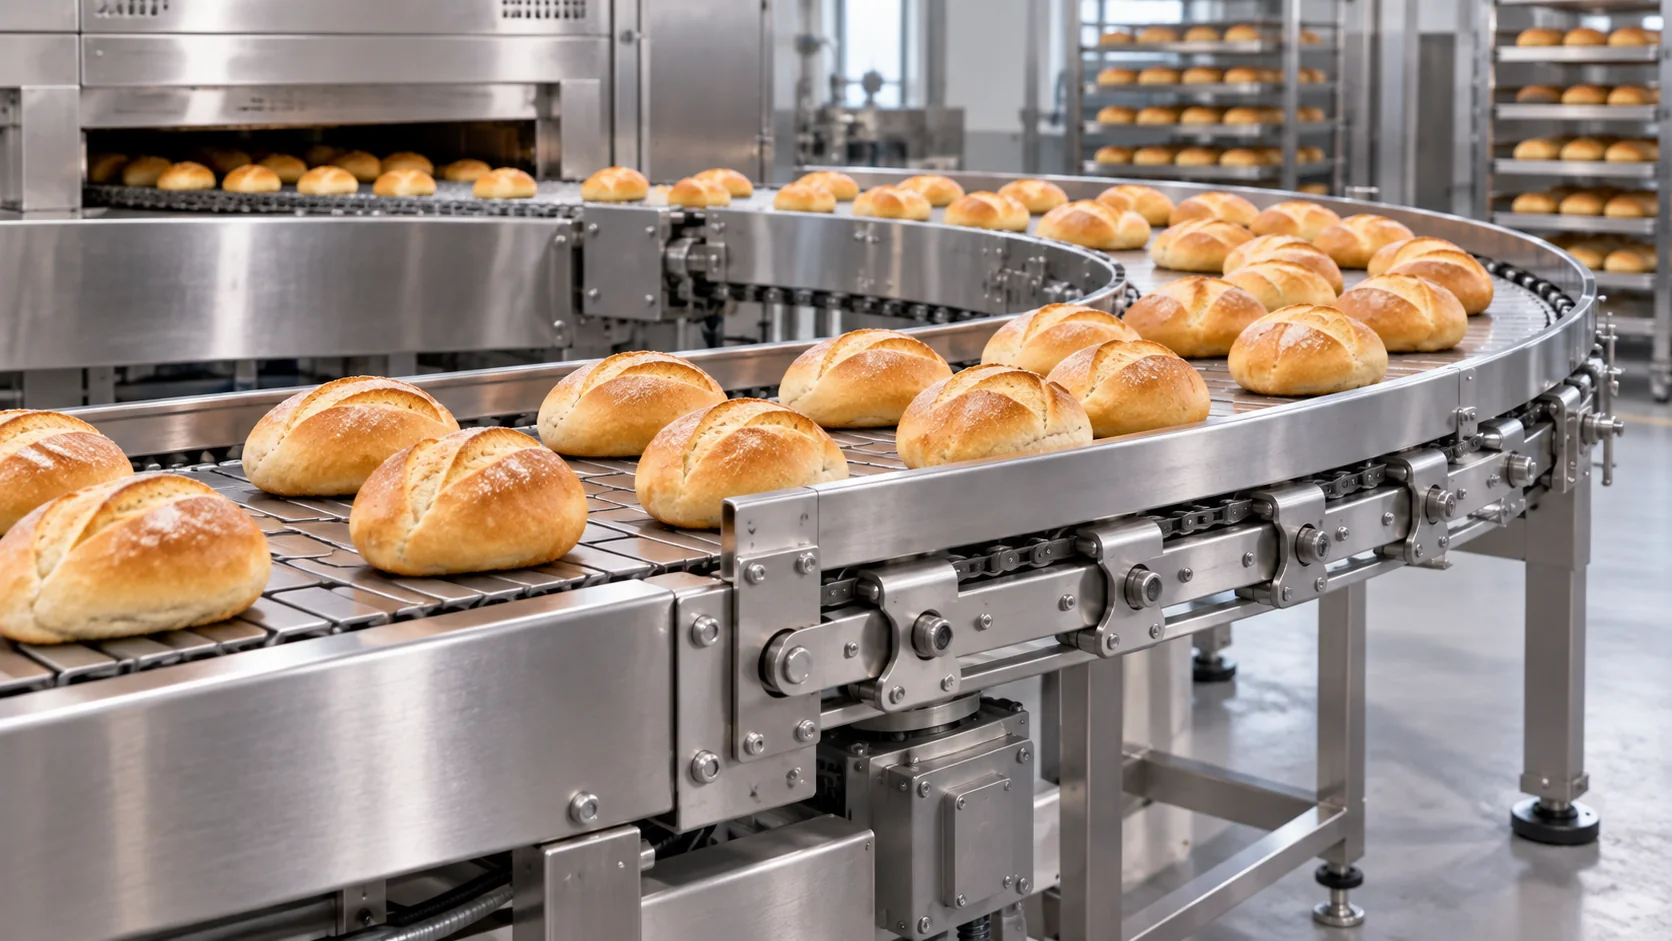
Identify the OEM/machine type and whether the chain works in proofing, oven, cooling, handling or packaging.
Provide pitch, width, roller/bush, pin, attachment and chain-center dimensions.
State speed, carrier/product load, starts, incline and take-up arrangement.
State temperature, humidity, washdown, cleaning chemistry and lubrication restrictions.
Identify exactly where the chain operates: proofing loop, heated oven run, cooling conveyor, tray return or packaging transfer. Avoid treating the whole bakery line as one duty.
Record pans, trays, rods, fixtures and attachment intervals. The carrier is part of the load path and often decides whether a standard, attachment or hollow-pin family is appropriate.
Separate normal production, heat-up, cleaning and shutdown conditions. Temperature peaks, humidity, chemistry and lubrication access can change the selection even when the base geometry stays the same.
Record what the conveyor is doing in the named zone: rising dough through a proofer, pans through a heated oven, finished product during cooling, or packaged goods at transfer. The same nominal chain size can face different joint, guide and carrier demands when the process state changes.
Separate product weight from the hardware carried by the chains. Pans, trays, cross bars, fixtures and supports can dominate the load and can also impose transverse forces when the two strands are not synchronized. Include carrier centers and attachment interval in the application record.
Describe the normal cycle, not only the maximum temperature. Proofing can combine warmth with condensate, ovens add thermal growth, cooling can create long return paths, and washdown introduces chemistry plus drying conditions. Mark where each exposure begins and ends.
State chain speed, start/stop frequency, incline or decline, center distance, number of strands, guide arrangement and take-up method. Long paths and repeated indexing can reveal tracking or synchronization constraints that do not appear in a static product specification.
Explain how the line is cleaned, whether joints are directly sprayed, how quickly the system dries and what lubrication restrictions apply. Material selection should be reviewed together with joint access, drainage and maintenance practice rather than treated as a stand-alone hygiene decision.
For an existing line, identify the dimensions and interfaces that cannot change without modifying the machine. For a new design, identify where there is freedom to optimize pitch, roller style, attachment or material. This keeps the RFQ focused on real interchange requirements.
| Handoff item | What to record | Why it changes the review |
|---|---|---|
| Machine zone | Process, location in line, drive/tail positions and transfer points | Connects the chain family to the real duty rather than a generic bakery label. |
| Hình học chuỗi | Pitch over several links, inside width, roller/bush, pin, plate and overall width | Controls sprocket engagement and physical interchange. |
| Giao diện sóng mang | Attachment holes, bend direction, cross rods, chain centers and repeated spacing | Defines how load reaches the chain and whether standard attachments are suitable. |
| Operating cycle | Speed, load, temperature, humidity, cleaning and lubrication constraints | Separates geometry that must match from service options that may be optimized. |
| Commercial scope | Required length or quantity, sample need, schedule and documentation | Lets technical and commercial review proceed on the same controlled request. |
If any dimension is uncertain, send clear machine-context and chain close-up photographs instead of guessing. The quotation drawing should close the remaining dimensional questions before production.
An application page should narrow the machine context, not select a chain by itself. Use it to identify the process zone, likely chain families and the measurements that deserve priority. When the line combines proofing, baking, cooling and packaging, prepare a separate duty note for each section rather than copying one condition across the full conveyor.
Existing sprockets, shaft centers, guide tracks and carrier locations often create dimensions that cannot change without machine work. Material, roller style, attachment manufacturing method or lubrication approach may have more freedom. Marking that boundary helps engineering improve service without creating an unnecessary retrofit.
Take a wide image of the conveyor route before collecting close-ups. Then photograph the chain at a sprocket, a representative attachment or cross rod, the take-up and any location showing unusual wear. A close-up without machine context can hide the very alignment or clearance issue that caused the symptom.
Compare the quotation drawing with the installed machine or OEM design before approval. Check pitch, widths, pin/roller geometry, attachment interval, chain-center spacing and any special material notes. Keep the approved revision with the maintenance baseline so future replacement requests begin with controlled information instead of a new visual guess.
Application-first selection is most reliable when the process, chain and machine are reviewed as one mechanism.
Define what the conveyor is doing in the process, then map environmental and carrier constraints to a suitable chain family. Record the actual conveyor section rather than describing the entire bakery line with one operating condition.
Bước răng, chiều rộng ngang, kích thước con lăn hoặc bạc lót, kích thước chốt, hình dạng đĩa xích và vị trí lắp đặt là những thông tin ban đầu để xác định khả năng tương thích.
Hãy nêu rõ tốc độ, tải trọng hỗ trợ hoặc khối lượng vật mang, nhiệt độ, độ ẩm, các ràng buộc về làm sạch và bôi trơn. Những chi tiết này sẽ quyết định lựa chọn nào đáng được xem xét.
Hãy gửi bản vẽ và ảnh chụp bối cảnh cùng nhau. Tách riêng các kích thước cố định khỏi các tùy chọn có thể được tối ưu hóa để việc kiểm tra bản vẽ cuối cùng được hiệu quả.


























