บันทึกรูปทรงเรขาคณิต
ระยะห่างระหว่างเกลียว, ความกว้าง, ลูกกลิ้ง/บูช, หมุด, แผ่น, ความกว้างโดยรวม และรูปแบบการติดตั้ง
คู่มือทางเทคนิคสำหรับเครือข่ายร้านเบเกอรี่
Oven Chain Inspection Checklist is best answered by combining measured chain geometry, machine duty and the operating environment. This guide shows what to inspect, record and discuss before a replacement or new-chain decision.
Oven Chain Inspection Checklist should be evaluated from the actual conveyor. Start with chain pitch, transverse geometry, sprocket condition and any carrier attachment, then add temperature, moisture, washdown, load, speed and take-up information. The objective is not to identify a chain by appearance; it is to produce an RFQ that preserves the machine interface and makes application-dependent choices explicit.

ก่อนถอดโซ่ ให้วัดคุณลักษณะหลายอย่าง ระยะห่างของฟันเฟือง (pitch) เป็นตัวกำหนดความสัมพันธ์พื้นฐานของระบบเกียร์ แต่ความกว้างด้านใน เส้นผ่านศูนย์กลางของลูกกลิ้งหรือบูช เส้นผ่านศูนย์กลางของหมุด ความสูงของแผ่น ความกว้างโดยรวม และขนาดของจุดยึด จะเป็นตัวแยกแยะรูปแบบต่างๆ ที่สามารถใช้ระยะห่างของฟันเฟือง (pitch) เดียวกันได้
สำหรับโซ่ที่สึกหรอ ให้วัดระยะห่างสะสมของข้อต่อหลายๆ ข้อ ถ่ายภาพโซ่จากด้านข้างและด้านปลาย และหากทำได้ ให้ถ่ายภาพเฟืองด้วย
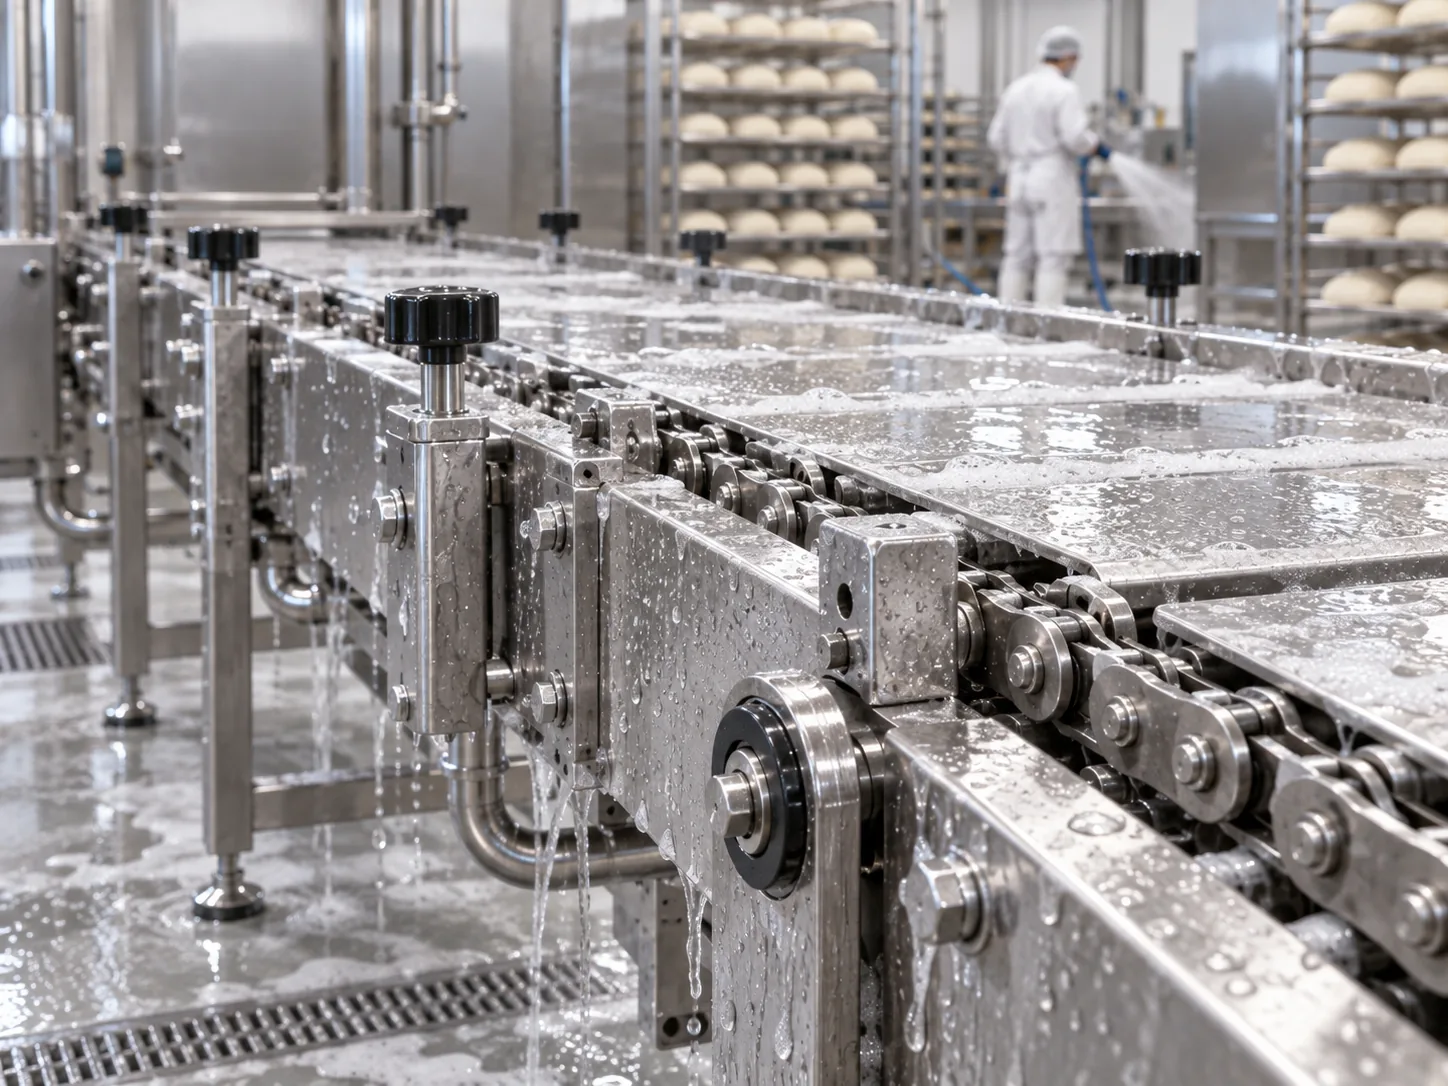
The same chain geometry can behave differently in a humid proofer, a hot oven, an ambient cooling section or a washdown area. For oven chain inspection checklist, document the exact machine zone, whether the chain carries product directly or moves pans/fixtures, and whether the joint sees heat, moisture, cleaning chemicals or abrasive residue.
ข้อมูลกระบวนการช่วยในการพิจารณาว่าคุณลักษณะใดบ้างที่คงที่เนื่องจากสามารถใช้แทนกันได้ และคุณลักษณะใดบ้าง เช่น วัสดุ ระยะห่าง หรือวิธีการผลิตชิ้นส่วนยึด ควรได้รับการตรวจสอบสำหรับการใช้งานนั้นๆ

โซ่ไม่สามารถทำงานได้อย่างอิสระ ลูกกลิ้งหรือบูชต้องเข้าและออกจากช่องว่างระหว่างฟันเฟืองได้อย่างราบรื่น ในขณะที่รางนำทางช่วยรองรับเส้นโซ่โดยไม่ทำให้เส้นโซ่เอียงไปด้านข้าง ฟันเฟืองที่งอ การจัดแนวเพลาที่ไม่ถูกต้อง เฟืองที่เยื้องศูนย์ หรือรางนำทางที่แน่นเกินไป อาจทำให้โซ่ใหม่สึกหรอเร็วขึ้น
ตรวจสอบเส้นทางทั้งหมดผ่านวงจรหนึ่งรอบ หากความเสียหายเกิดขึ้นซ้ำที่ตำแหน่งเครื่องจักรเดิม ให้ตรวจสอบส่วนรองรับ ส่วนถ่ายโอน หรือส่วนขนส่งในบริเวณนั้นก่อนที่จะสรุปว่าห่วงโซ่นั้นมีข้อบกพร่อง
ระยะห่างระหว่างเกลียว, ความกว้าง, ลูกกลิ้ง/บูช, หมุด, แผ่น, ความกว้างโดยรวม และรูปแบบการติดตั้ง
อุณหภูมิ ความชื้น การล้างทำความสะอาด ความเร็ว โหลด ชั่วโมงการผลิต และจำนวนครั้งในการเริ่มการผลิต
เฟือง, ตัวนำ, ศูนย์กลางโซ่, การปรับความตึง, การจัดแนว และระยะห่างของตัวลำเลียง
อนุมัติรูปทรง วัสดุ และการกำหนดค่าที่เหมาะสมกับการใช้งานขั้นสุดท้ายก่อนทำการติดตั้ง
สอบถามว่ามีการเปลี่ยนแปลงอะไรบ้างก่อนที่ปัญหาจะเกิดขึ้น เช่น อัตราการผลิต น้ำหนักของผลิตภัณฑ์หรือถาด รอบการทำความสะอาด สารหล่อลื่น อุณหภูมิ ช่วงเวลาการบำรุงรักษา หรือเฟืองที่เปลี่ยนไป ข้อมูลแนวโน้มมีค่ามากกว่าภาพถ่ายเพียงภาพเดียว เพราะแสดงให้เห็นว่าการสึกหรอเกิดขึ้นอย่างสม่ำเสมอหรือกระจุกตัวอยู่เฉพาะจุด
ระหว่างการตรวจสอบตามปกติ ให้สังเกตข้อต่อที่ฝืด การสึกหรอของลูกกลิ้ง การเคลื่อนที่ของหมุด ชิ้นส่วนที่แตกหรือบิดงอ การสัมผัสด้านข้างที่ผิดปกติ และการดึงที่ไม่สม่ำเสมอ ควรติดตั้งอุปกรณ์ป้องกันและปฏิบัติตามขั้นตอนด้านความปลอดภัยตามข้อกำหนดของผู้เป็นเจ้าของเครื่องจักร
โปรดระบุขนาดที่วัดได้ ชื่อเครื่องจักร/กระบวนการ รูปภาพ ภาพวาด (ถ้ามี) จำนวนหรือความยาวโซ่ที่ต้องการ ช่วงการยึด ระยะห่างระหว่างศูนย์กลางโซ่ ข้อมูลเฟือง อุณหภูมิ สภาพการล้างทำความสะอาด โหลด และช่วงเวลาส่งมอบเป้าหมาย โปรดตรวจสอบ คู่มือการเลือกเครือร้านเบเกอรี่ และ ภาพรวมกลุ่มผลิตภัณฑ์ สำหรับขั้นตอนการตัดสินใจถัดไป
A useful diagnosis starts with evidence that can be repeated by a second person. organizing inspection by route position and thermal exposure rather than by a single chain-length reading. Record joint freedom, side wear, pitch growth, sprocket teeth, guides, take-up and carrier hardware. When the chain is worn, note which readings may be influenced by joint clearance or deformation, and prefer multi-pitch or multi-point measurements over one isolated dimension.
The chain does not operate by itself. In tunnel oven conveyor systems, inspect the sprockets, guides, return path, take-up and carrier interface at the same time. The symptom to watch is localized hot-zone damage, dry joints, guide scuffing or uneven tracking. A local problem that repeats at one machine position often points to alignment, clearance or mating-hardware issues rather than a uniform chain problem.
The practical decision is to record condition at entry, hot zone, exit and return so the cause is not lost in a single overall judgement. That prevents a common error: changing chain tension, material or size before the root constraint has been identified. Use the chain drawing and the machine envelope together, because a configuration that looks correct in isolation can still interfere with a guard, transfer plate, sensor bracket or carrier.
อธิบายวงจรการทำงานโดยรวม แทนที่จะใช้คำคุณศัพท์เพียงคำเดียว เช่น “ร้อน” “เปียก” หรือ “เกรดอาหาร” ระบุอุณหภูมิปกติและอุณหภูมิสูงสุด (หากเกี่ยวข้อง) การสัมผัสกับความชื้นหรือการทำความสะอาด ความเร็ว พฤติกรรมการเริ่ม/หยุด และข้อจำกัดในการหล่อลื่น รายละเอียดเหล่านี้จะเป็นตัวตัดสินว่าจำเป็นต้องเปลี่ยนแปลงระยะห่าง วัสดุ หรือวิธีการบำรุงรักษาหรือไม่ ในขณะที่รูปทรงเรขาคณิตพื้นฐานยังคงเหมือนเดิม
| ตรวจสอบ | ทำไมเรื่องนี้ถึงสำคัญ | สิ่งที่ต้องส่งหรือยืนยัน |
|---|---|---|
| การระบุตัวตน | Confirm joint freedom, side wear, pitch growth, sprocket teeth, guides, take-up and carrier hardware. Use a measurement sequence that can be repeated after removal so the installed and bench readings can be compared. | ภาพร่างที่มีขนาดกำกับ ภาพถ่ายที่แสดงมาตราส่วน และแบบร่างหรือหมายเลขชิ้นส่วนเดิมทั้งหมด |
| ตำแหน่งเส้นทาง | Map where the chain runs through tunnel oven conveyor systems. Mark the exact location of localized hot-zone damage, dry joints, guide scuffing or uneven tracking instead of reporting the condition only as a whole-line problem. | ภาพประกอบแสดงส่วนของสายพานลำเลียง ตำแหน่งขับเคลื่อน/ท้าย และเส้นทางส่งกลับ |
| ชิ้นส่วนที่ประกบกัน | ตรวจสอบลักษณะฟันเฟือง การติดตั้งลูกกลิ้ง การจัดแนวเพลา/เฟืองโซ่ การสัมผัสของตัวนำ และระยะเผื่อการดึงกลับ ชิ้นส่วนเหล่านี้สามารถสร้างรูปแบบการสึกหรอที่เลียนแบบปัญหาการเลือกโซ่ได้ | จำนวนฟันเฟืองและรูปภาพ แผนผังตัวนำ และตำแหน่งการปรับตั้งปัจจุบัน |
| เส้นทางการโหลด | Identify how product carriers, pans, rods or fixtures transfer load into the chain. For this topic, the key focus is organizing inspection by route position and thermal exposure rather than by a single chain-length reading. | ภาพวาดแสดงตำแหน่งของตัวยึด ระยะห่างระหว่างจุดยึด ระยะห่างระหว่างจุดศูนย์กลางของโซ่ และมวล/แรงที่รองรับ (หากทราบ) |
| สิ่งแวดล้อม | บันทึกอุณหภูมิ ความชื้น การล้างทำความสะอาด การปนเปื้อน และข้อจำกัดด้านการหล่อลื่นในแต่ละโซนของเครื่องจักร แยกการสัมผัสอย่างต่อเนื่องออกจากการสัมผัสในช่วงเวลาสั้นๆ หรือช่วงการทำความสะอาด | สรุปสภาพการใช้งานและแนวทางการบำรุงรักษา/การหล่อลื่น |
| ปล่อย | The final engineering action is to record condition at entry, hot zone, exit and return so the cause is not lost in a single overall judgement. The approved drawing should distinguish fixed interchange dimensions from selectable options. | inspection photos by zone, temperature data, lubrication method and measured wear. |
A uniform change along the whole strand suggests a different mechanism from damage concentrated at one sprocket, guide or transfer. For Oven Chain Inspection Checklist, compare left/right sides and loaded/return paths. The distribution of wear can reveal whether the driver is joint wear, side loading, contamination, thermal change or a carrier that is forcing the chain out of its natural path.
Increasing tension can temporarily change noise or tracking without correcting the underlying cause. If the observed issue is localized hot-zone damage, dry joints, guide scuffing or uneven tracking, first confirm alignment, take-up geometry and articulation. Excessive tension can add bearing load and make a marginal guide or attachment problem worse.
อุปกรณ์ในโรงงานเบเกอรี่สามารถเปลี่ยนสถานะระหว่างการผลิต การทำความสะอาด และการปิดระบบได้ โซ่อาจทำงานได้ปกติเมื่อเย็นและฝืดเมื่อร้อน หรืออาจทำงานได้อย่างอิสระในระหว่างการผลิต แต่เกิดการกัดกร่อนหลังจากปิดระบบเนื่องจากความชื้นซ้ำๆ บันทึกสถานะที่เกิดอาการดังกล่าว เพื่อให้เลือกวิธีการแก้ไขที่เหมาะสมกับรอบการทำงานจริง
For an unknown chain, one close-up is not enough. Pair a complete machine-zone image with side and end views of several pitches, a sprocket-engagement photo and a clear attachment/carrier view. Place a scale only where it does not hide the feature being measured. This photo set makes organizing inspection by route position and thermal exposure rather than by a single chain-length reading easier to evaluate remotely.
Record joint freedom, side wear, pitch growth, sprocket teeth, guides, take-up and carrier hardware, chain centers, sprocket tooth count and the carrier interface before changing components.
Describe what happens in tunnel oven conveyor systems, including temperature or moisture changes, speed, load and cleaning/lubrication constraints.
Document where localized hot-zone damage, dry joints, guide scuffing or uneven tracking appears. Compare drive, tail, loaded run, return run and transfer points rather than averaging the entire conveyor.
Include inspection photos by zone, temperature data, lubrication method and measured wear. State the required quantity or chain length and any documentation needed with the order.
Review pitch, widths, pin/roller geometry, attachments and material notes on one controlled drawing revision. For Oven Chain Inspection Checklist, the release decision should explicitly address organizing inspection by route position and thermal exposure rather than by a single chain-length reading.
หลังการติดตั้ง ให้ตรวจสอบการทำงานอย่างน้อยหนึ่งรอบเต็ม ตรวจสอบการเข้า/ออกของเฟืองและระยะห่างของตัวพา และตรวจสอบความตึงของโซ่อีกครั้งตามขั้นตอนของผู้ผลิตเครื่องจักร ไม่ควรใช้โซ่ใหม่เพื่อชดเชยชิ้นส่วนที่สึกหรอหรือจัดตำแหน่งไม่ถูกต้อง

The main reason to keep this process structured is that organizing inspection by route position and thermal exposure rather than by a single chain-length reading interacts with more than one component. A change that improves one symptom can shift load into another part of the mechanism. For example, correcting guide alignment may reduce side wear but also expose a take-up setting that was previously compensating for the misalignment. Record changes one at a time so the result can be interpreted.
For planned maintenance, compare the present condition with a baseline whenever one exists. If there is no baseline, create one during the next shutdown: photograph the sprockets and guide surfaces, record take-up position, measure a defined number of pitches, and note the chain’s location in tunnel oven conveyor systems. Repeating the same observations later is more informative than relying on general statements such as “the chain has stretched.”
เมื่อมีแบบร่างอยู่แล้ว ให้ตรวจสอบว่าฮาร์ดแวร์ที่ติดตั้งยังตรงกับแบบร่างนั้นหรือไม่ อุปกรณ์เบเกอรี่มักถูกดัดแปลงแก้ไขตลอดอายุการใช้งาน เช่น ตัวยึดอาจได้รับการซ่อมแซม รางนำทางอาจถูกย้าย เฟืองอาจถูกเปลี่ยน และช่วงระยะห่างของจุดยึดอาจเปลี่ยนแปลงไป แบบร่างยังคงมีประโยชน์ แต่การตรวจสอบภาคสนามจะช่วยป้องกันไม่ให้เอกสารเก่าถูกนำมาใช้เป็นหลักฐานยืนยันการกำหนดค่าปัจจุบันได้
Procurement and engineering should use the same evidence package. The RFQ should not separate commercial quantity from technical context: inspection photos by zone, temperature data, lubrication method and measured wear. This makes it possible to judge whether a standard series, a modified attachment or a custom replacement is the appropriate route without creating unnecessary back-and-forth.
Finally, treat the website as a preparation tool rather than the controlling product drawing. Measurements and diagrams narrow the family and help organize the RFQ; the released drawing defines the ordered configuration. That distinction is especially important where localized hot-zone damage, dry joints, guide scuffing or uneven tracking could have more than one mechanical cause.
Use Oven Chain Inspection Checklist as a machine-level question, not just a chain inspection. Compare the loaded and return runs, drive and tail ends, and any transfer or carrier transition in tunnel oven conveyor systems. Document whether localized hot-zone damage, dry joints, guide scuffing or uneven tracking is distributed along the strand or repeats at one location. That pattern helps separate progressive joint wear from alignment, guide, sprocket or carrier problems that a new chain alone will not correct.
The working record should include joint freedom, side wear, pitch growth, sprocket teeth, guides, take-up and carrier hardware. Mark which values are fixed by the existing machine and which values can be changed to improve service. The central engineering focus is organizing inspection by route position and thermal exposure rather than by a single chain-length reading. When a legacy part number conflicts with field measurements, hold the RFQ until the installed interface and the controlled drawing can be reconciled.
A useful enquiry combines commercial quantity with the technical package: inspection photos by zone, temperature data, lubrication method and measured wear. Also state whether the request is a direct replacement, a planned modification or a new machine design. The release objective is to record condition at entry, hot zone, exit and return so the cause is not lost in a single overall judgement. This reduces quote revisions and prevents a visually similar chain from being treated as interchangeable before geometry and duty have been checked.
ให้ใช้ข้อมูลอ้างอิงเดิมหากมี แต่ตรวจสอบรูปทรงและลักษณะการใช้งานของชิ้นส่วนที่ติดตั้งไว้ การดัดแปลงเครื่องจักร การเปลี่ยนชิ้นส่วนก่อนหน้านี้ หรือการสึกหรอ อาจทำให้หมายเลขชิ้นส่วนเพียงอย่างเดียวไม่สมบูรณ์
ใช้วิธีการวัดระยะห่างของฟันเฟืองหลายจุดในจำนวนข้อต่อที่เหมาะสม และบันทึกวิธีการวัด เปรียบเทียบกับระยะห่างของฟันเฟืองที่กำหนดไว้และข้อจำกัดในการบำรุงรักษาเครื่องจักร แทนที่จะพึ่งพาการวัดเพียงข้อต่อเดียวที่อยู่ติดกัน
เมื่อใดก็ตามที่พบการสึกหรอของฟันเฟือง การเกี่ยวกัน ปัญหาการจัดแนว หรือการสึกหรอของโซ่ก่อนกำหนดซ้ำๆ โซ่และเฟืองจะทำงานเป็นระบบขบกัน

























