Описание продукта
CZPT rollers enhance rotation on the bushing while reducing impact loads on the sprocket tooth during operation.
All components are heat treated to achieve maximum strength.
Pre-loaded during the manufacturing process to minimize initial elongation.
Hot dipped lubrication ensures 100% lubrication of all chain components to extend wear life and reduce maintenance costs.
| ANSI NO. |
PITCH | BUSH WIDTH |
ROLLER DIA |
PIN | PLATE | ULTIMATE TENSILE STRENGTH |
WEIGHT | |||
| Д | L | Lc | Т | H | ||||||
| mm | mm | mm | mm | mm | mm | mm | mm | KN/min | kg/m | |
| 428H-OR | 12.700 | 7.75 | 8.51 | 4.45 | 22.80 | 23.90 | 2.03 | 11.81 | 23.00 | 0.95 |
| 520H-OR | 15.875 | 6.25 | 10.16 | 5.09 | 22.00 | 23.20 | 2.42 | 15.09 | 21.80 | 1.30 |
| 50-OR | 15.875 | 9.40 | 10.16 | 5.09 | 24.80 | 26.00 | 2.03 | 15.09 | 21.80 | 1.15 |
| 60-OR | 19.050 | 12.57 | 11.91 | 5.94 | 30.40 | 31.90 | 2.42 | 18.08 | 31.10 | 1.66 |
| 80-OR | 25.400 | 15.75 | 15.88 | 7.94 | 35.50 | 37.00 | 3.25 | 24.13 | 55.60 | 2.95 |
| Применение: | Transmission Chain, Conveyor Chain, Dedicated Special Chain, Roller Chain |
|---|---|
| Материал: | Alloy/Carbon Steel |
| Обработка поверхности: | Полировка |
| Особенность: | Heat Resistant |
| Размер цепочки: | 1/2"*1" |
| Структура: | Роликовая цепь |
| Образцы: |
US$ 10/Meter
1 Meter(Min.Order) | |
|---|
| Настройка: |
Доступный
| Индивидуальный запрос |
|---|
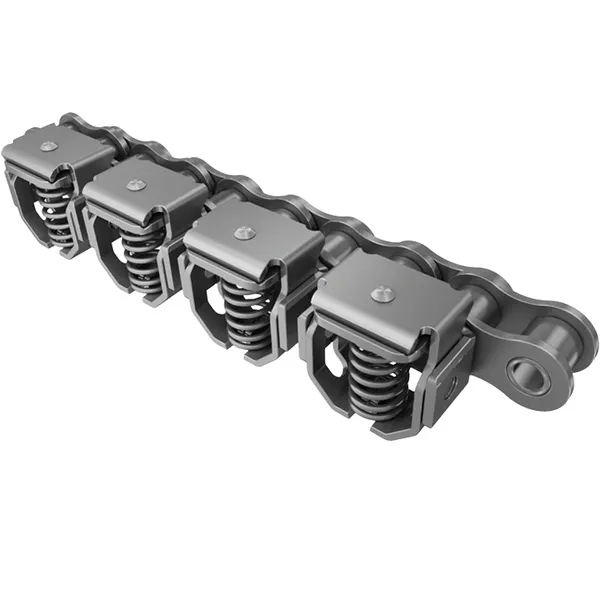
What are the benefits of using an overhead conveyor chain system?
Using an overhead conveyor chain system offers several benefits in various industrial applications. Here are some key advantages:
1. Space Optimization:
– Overhead conveyor chain systems utilize the vertical space, allowing efficient utilization of floor space. This is especially beneficial in facilities with limited floor area, as it enables efficient material handling and production flow without obstructing the work area.
2. Flexibility and Versatility:
– Overhead conveyor chains offer flexibility in routing and can be customized to fit the specific layout requirements of the facility. They can traverse different areas, including assembly lines, paint booths, storage areas, and more. The versatility of overhead systems allows for efficient and adaptable material movement.
3. Improved Safety:
– Overhead conveyor chains minimize ground-level obstructions, reducing the risk of tripping hazards and accidents. Operators and workers can safely navigate the work area without interference from the conveyor system.
4. Product Protection:
– Overhead conveyor chains provide better protection for the products being transported. By keeping the products elevated and away from potential hazards on the floor, such as dust, debris, or spills, the risk of product damage or contamination is reduced.
5. Increased Efficiency:
– Overhead conveyor systems can enhance production efficiency by facilitating continuous material flow and reducing manual handling. They enable automated loading and unloading of materials, leading to faster processing times and improved overall productivity.
6. Easy Maintenance:
– Overhead conveyor chains are typically designed for easy maintenance. Components such as chains, trolleys, and drives can be accessed and serviced conveniently, minimizing downtime and maintenance costs.
7. Customization and Integration:
– Overhead conveyor chains can be tailored to meet specific application requirements, including load capacity, speed, and control systems. They can also be integrated with other automated systems, such as robotic workstations or sorting mechanisms, to further optimize the material handling process.
Overall, using an overhead conveyor chain system provides efficient material handling, maximizes space utilization, enhances safety, and improves productivity in industrial environments.
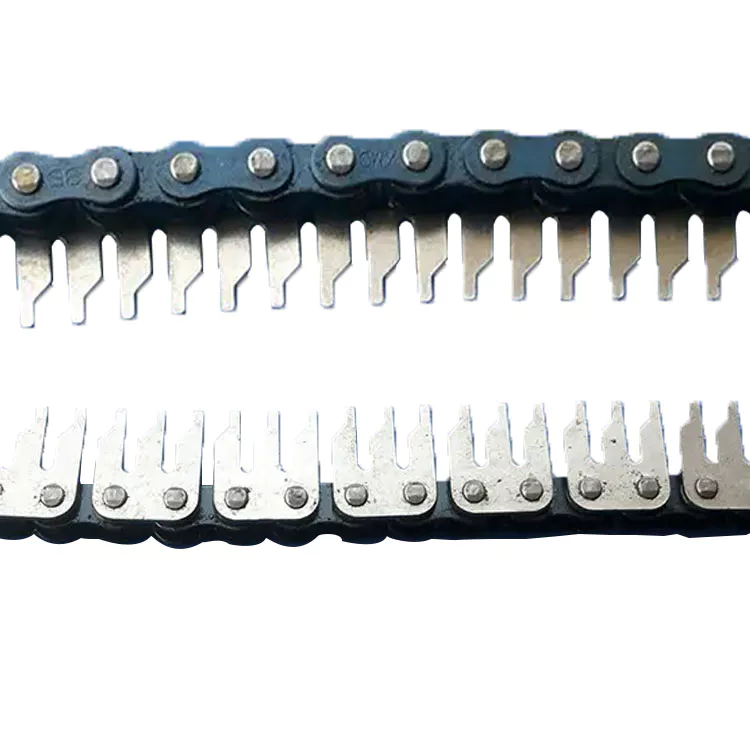
Can a conveyor chain be used in food processing applications?
Yes, a conveyor chain can be used in food processing applications. Conveyor chains play a crucial role in the efficient and hygienic handling of food products throughout the production process. Here are some key points to consider:
1. Food-Grade Materials: Conveyor chains used in food processing applications are typically made from food-grade materials such as stainless steel or plastic. These materials are corrosion-resistant, easy to clean, and comply with food safety regulations.
2. Hygiene Considerations: Food processing environments require high standards of hygiene. Conveyor chains designed for food applications incorporate features such as smooth surfaces, open link designs, and easy disassembly for thorough cleaning. They may also have specialized coatings or treatments to prevent bacterial growth.
3. Sanitary Design: Conveyor chains for food processing applications are designed with minimal crevices or joints to prevent food particles from getting trapped. They may have self-draining capabilities to remove excess fluids or debris.
4. Product Integrity: Conveyor chains in food processing applications ensure gentle handling of delicate food products to avoid damage or contamination. They can be equipped with accessories like cleats, side guards, or modular belt systems to securely hold and transport items of various shapes and sizes.
5. High Temperature and Washdown Capabilities: Some food processing applications require conveyor chains to withstand high temperatures during cooking, baking, or sterilization processes. Specialized chains with heat-resistant materials or coatings are available. Additionally, conveyor chains used in food processing should be capable of withstanding frequent washdowns and cleaning with water or cleaning agents.
6. Compliance with Standards: Conveyor chains used in food processing applications must comply with industry-specific standards such as FDA (Food and Drug Administration) regulations, HACCP (Hazard Analysis Critical Control Point) guidelines, and other food safety certifications.
When selecting a conveyor chain for food processing applications, it is important to consider the specific requirements of the production line, including the type of food being handled, the operating conditions, and the necessary sanitary standards. Proper maintenance and regular cleaning protocols should also be implemented to ensure food safety and product integrity.

How does a conveyor chain compare to other types of conveyor systems?
Conveyor chains are one of the common types of conveyor systems used in various industries. They offer specific advantages and characteristics that differentiate them from other types of conveyor systems.
1. Versatility: Conveyor chains are highly versatile and can be used for a wide range of applications, including horizontal, inclined, and vertical conveying. They can handle various types of materials, from bulk solids to individual items.
2. High Load Capacity: Conveyor chains are known for their high load-carrying capacity. They are designed to handle heavy loads and can be used in applications where other conveyor systems may not be suitable.
3. Durability: Conveyor chains are built to withstand harsh operating conditions and heavy-duty use. They are made from strong and durable materials, such as steel or alloy, that can withstand abrasion, impact, and wear.
4. Flexibility: Conveyor chains offer flexibility in terms of layout and design. They can be configured to accommodate complex conveyor paths, curves, and multiple discharge points, allowing for efficient material flow and system customization.
5. Cost-Effective: Conveyor chains often provide a cost-effective solution for material handling compared to other conveyor systems. They have a relatively low initial cost, require less maintenance, and have a longer service life.
However, it’s important to note that conveyor chains may not be suitable for every application. Other types of conveyor systems, such as belt conveyors, screw conveyors, or pneumatic conveyors, may offer specific advantages depending on the application requirements, material characteristics, or environmental factors.
Ultimately, the selection of the appropriate conveyor system depends on factors such as load capacity, material properties, layout constraints, cost considerations, and specific application needs.


editor by CX 2023-08-16

























