Record geometry
Pitch, width, roller/bush, pin, plate, overall width and attachment pattern.
Bakery Chain Technical Guide
Roller Chain vs Engineering Conveyor Chain is best answered by combining measured chain geometry, machine duty and the operating environment. This guide shows what to inspect, record and discuss before a replacement or new-chain decision.
Roller Chain vs Engineering Conveyor Chain should be evaluated from the actual conveyor. Start with chain pitch, transverse geometry, sprocket condition and any carrier attachment, then add temperature, moisture, washdown, load, speed and take-up information. The objective is not to identify a chain by appearance; it is to produce an RFQ that preserves the machine interface and makes application-dependent choices explicit.
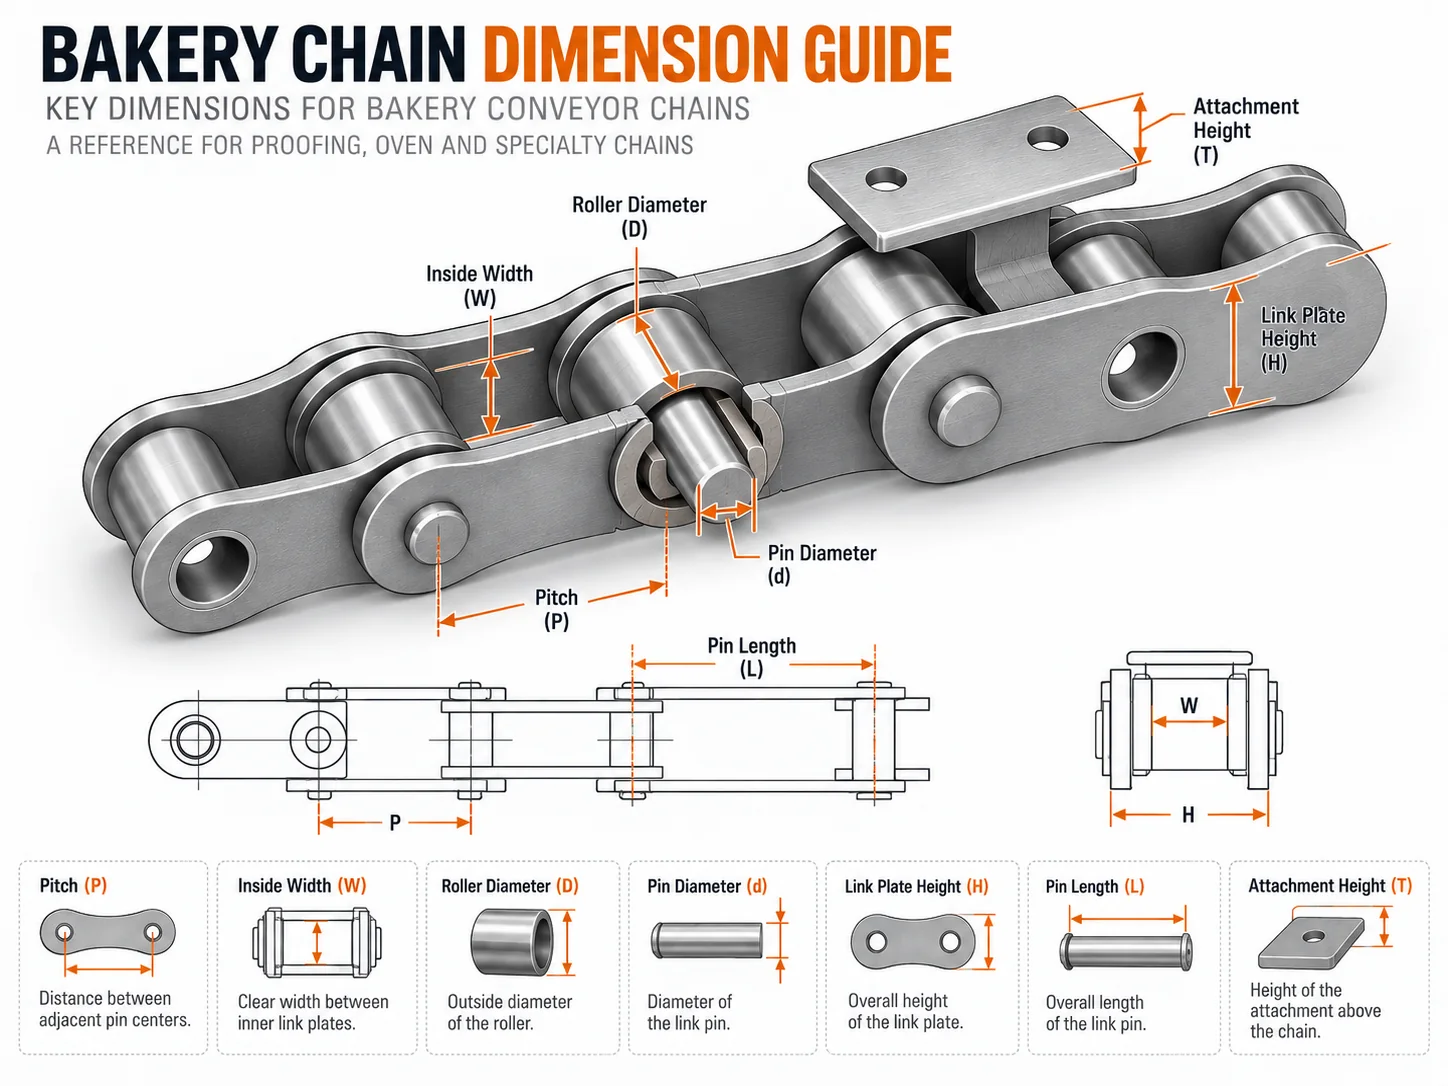
Measure several characteristics before removing the chain. Pitch locates the basic gearing relationship, but inside width, roller or bush diameter, pin diameter, plate height, overall width and attachment dimensions distinguish configurations that can share the same nominal pitch.
For a worn strand, measure cumulative pitch across multiple links. Photograph the chain from the side and end, and include the sprocket where practical.
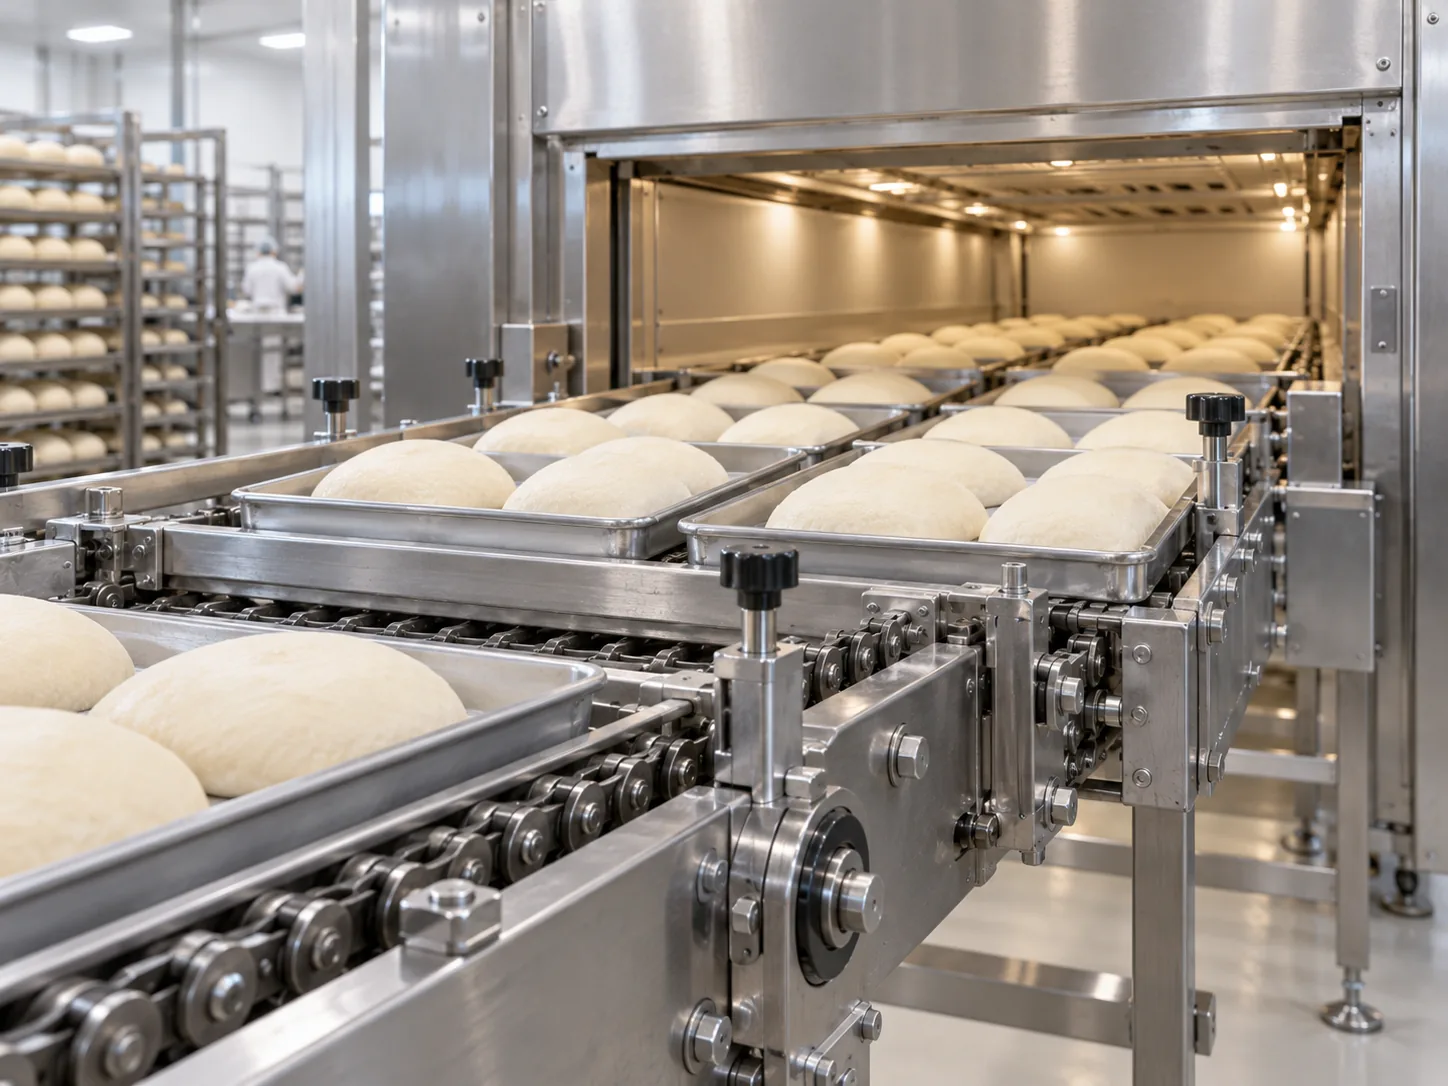
The same chain geometry can behave differently in a humid proofer, a hot oven, an ambient cooling section or a washdown area. For roller chain vs engineering conveyor chain, document the exact machine zone, whether the chain carries product directly or moves pans/fixtures, and whether the joint sees heat, moisture, cleaning chemicals or abrasive residue.
Process data helps determine which characteristics are fixed by interchangeability and which characteristics—such as material, clearance or attachment manufacturing method—should be reviewed for the application.

A chain does not operate independently. Rollers or bushes must enter and leave the sprocket tooth spaces smoothly, while guide tracks support the strand without forcing it sideways. Hooked teeth, shaft misalignment, eccentric sprockets or a tight guide can make a new chain wear quickly.
Inspect the complete path through one full circuit. If damage repeats at the same machine location, investigate the local support, transfer or carrier before assuming the chain itself is defective.
Pitch, width, roller/bush, pin, plate, overall width and attachment pattern.
Temperature, moisture, washdown, speed, load, production hours and starts.
Sprockets, guides, chain centers, take-up, alignment and carrier clearances.
Approve the final ordered geometry, material and application-dependent configuration before installation.
Ask what changed before the problem appeared: production rate, product or pan weight, cleaning cycle, lubricant, temperature, maintenance interval or replaced sprockets. Trend information is more valuable than a single photograph because it shows whether wear is uniform or concentrated.
During routine inspection, look for stiff joints, roller wear, pin movement, cracked or bent attachments, abnormal side contact and uneven take-up. Keep guards and safety procedures in place according to the machine owner’s requirements.
Include the measured dimensions, machine/process name, photos, drawing if available, quantity or required chain length, attachment interval, chain-center spacing, sprocket information, temperature, washdown condition, load and target delivery window. Review the bakery chain selection guide and the product-family overview for the next decision step.
A useful diagnosis starts with evidence that can be repeated by a second person. separating power-transmission duty from load-carrying conveyor duty. Record chain pull, speed, pitch, roller/attachment geometry, track support and carrier load. When the chain is worn, note which readings may be influenced by joint clearance or deformation, and prefer multi-pitch or multi-point measurements over one isolated dimension.
The chain does not operate by itself. In bakery drives versus product/carrier conveyors, inspect the sprockets, guides, return path, take-up and carrier interface at the same time. The symptom to watch is using a transmission-oriented chain where attachments, large rollers or conveyor clearances are required. A local problem that repeats at one machine position often points to alignment, clearance or mating-hardware issues rather than a uniform chain problem.
The practical decision is to start from what the chain must carry and how it runs on tracks and sprockets, then choose the construction family. That prevents a common error: changing chain tension, material or size before the root constraint has been identified. Use the chain drawing and the machine envelope together, because a configuration that looks correct in isolation can still interfere with a guard, transfer plate, sensor bracket or carrier.
Describe the operating cycle rather than a single adjective such as “hot,” “wet” or “food grade.” State normal and peak temperature where relevant, moisture or cleaning exposure, speed, start/stop behavior and lubrication limitations. These details decide whether clearances, materials or maintenance practice need to change while the basic geometry remains fixed.
| Check | Why it matters | What to send or verify |
|---|---|---|
| Identification | Confirm chain pull, speed, pitch, roller/attachment geometry, track support and carrier load. Use a measurement sequence that can be repeated after removal so the installed and bench readings can be compared. | Dimensioned sketch, scale-aware photos and any legacy drawing or part number. |
| Route position | Map where the chain runs through bakery drives versus product/carrier conveyors. Mark the exact location of using a transmission-oriented chain where attachments, large rollers or conveyor clearances are required instead of reporting the condition only as a whole-line problem. | Context photo showing the conveyor section, drive/tail positions and return path. |
| Mating parts | Inspect tooth profile, roller seating, shaft/sprocket alignment, guide contact and take-up reserve. These parts can create wear patterns that imitate a chain-selection problem. | Sprocket tooth count and photos, guide layout and current take-up position. |
| Load path | Identify how product carriers, pans, rods or fixtures transfer load into the chain. For this topic, the key focus is separating power-transmission duty from load-carrying conveyor duty. | Carrier drawing, attachment interval, chain-center spacing and supported mass/force where known. |
| Environment | Record temperature, humidity, washdown, contamination and lubrication restrictions by machine zone. Separate continuous exposure from short peaks or cleaning events. | Operating-condition summary and maintenance/lubrication practice. |
| Release | The final engineering action is to start from what the chain must carry and how it runs on tracks and sprockets, then choose the construction family. The approved drawing should distinguish fixed interchange dimensions from selectable options. | power/load data, conveyor layout, attachments, speed and environment. |
A uniform change along the whole strand suggests a different mechanism from damage concentrated at one sprocket, guide or transfer. For Roller Chain vs Engineering Conveyor Chain, compare left/right sides and loaded/return paths. The distribution of wear can reveal whether the driver is joint wear, side loading, contamination, thermal change or a carrier that is forcing the chain out of its natural path.
Increasing tension can temporarily change noise or tracking without correcting the underlying cause. If the observed issue is using a transmission-oriented chain where attachments, large rollers or conveyor clearances are required, first confirm alignment, take-up geometry and articulation. Excessive tension can add bearing load and make a marginal guide or attachment problem worse.
Bakery equipment can move between production, cleaning and shutdown states. A chain may articulate normally when cool and become tight when heated, or run freely during production but corrode after repeated wet shutdowns. Record the state in which the symptom occurs so the selected corrective action addresses the real duty cycle.
For an unknown chain, one close-up is not enough. Pair a complete machine-zone image with side and end views of several pitches, a sprocket-engagement photo and a clear attachment/carrier view. Place a scale only where it does not hide the feature being measured. This photo set makes separating power-transmission duty from load-carrying conveyor duty easier to evaluate remotely.
Record chain pull, speed, pitch, roller/attachment geometry, track support and carrier load, chain centers, sprocket tooth count and the carrier interface before changing components.
Describe what happens in bakery drives versus product/carrier conveyors, including temperature or moisture changes, speed, load and cleaning/lubrication constraints.
Document where using a transmission-oriented chain where attachments, large rollers or conveyor clearances are required appears. Compare drive, tail, loaded run, return run and transfer points rather than averaging the entire conveyor.
Include power/load data, conveyor layout, attachments, speed and environment. State the required quantity or chain length and any documentation needed with the order.
Review pitch, widths, pin/roller geometry, attachments and material notes on one controlled drawing revision. For Roller Chain vs Engineering Conveyor Chain, the release decision should explicitly address separating power-transmission duty from load-carrying conveyor duty.
After installation, observe at least one full circuit, check sprocket entry/exit and carrier clearance, and recheck take-up according to the machine maker’s procedure. New chain should not be used to compensate for worn or misaligned hardware.

The main reason to keep this process structured is that separating power-transmission duty from load-carrying conveyor duty interacts with more than one component. A change that improves one symptom can shift load into another part of the mechanism. For example, correcting guide alignment may reduce side wear but also expose a take-up setting that was previously compensating for the misalignment. Record changes one at a time so the result can be interpreted.
For planned maintenance, compare the present condition with a baseline whenever one exists. If there is no baseline, create one during the next shutdown: photograph the sprockets and guide surfaces, record take-up position, measure a defined number of pitches, and note the chain’s location in bakery drives versus product/carrier conveyors. Repeating the same observations later is more informative than relying on general statements such as “the chain has stretched.”
When an existing drawing is available, verify that the installed hardware still matches it. Bakery equipment is often modified over its service life: carriers can be repaired, guide rails moved, sprockets replaced, and attachment intervals changed. The drawing remains useful, but field verification prevents a historical document from being treated as proof of the current configuration.
Procurement and engineering should use the same evidence package. The RFQ should not separate commercial quantity from technical context: power/load data, conveyor layout, attachments, speed and environment. This makes it possible to judge whether a standard series, a modified attachment or a custom replacement is the appropriate route without creating unnecessary back-and-forth.
Finally, treat the website as a preparation tool rather than the controlling product drawing. Measurements and diagrams narrow the family and help organize the RFQ; the released drawing defines the ordered configuration. That distinction is especially important where using a transmission-oriented chain where attachments, large rollers or conveyor clearances are required could have more than one mechanical cause.
Use Roller Chain vs Engineering Conveyor Chain as a machine-level question, not just a chain inspection. Compare the loaded and return runs, drive and tail ends, and any transfer or carrier transition in bakery drives versus product/carrier conveyors. Document whether using a transmission-oriented chain where attachments, large rollers or conveyor clearances are required is distributed along the strand or repeats at one location. That pattern helps separate progressive joint wear from alignment, guide, sprocket or carrier problems that a new chain alone will not correct.
The working record should include chain pull, speed, pitch, roller/attachment geometry, track support and carrier load. Mark which values are fixed by the existing machine and which values can be changed to improve service. The central engineering focus is separating power-transmission duty from load-carrying conveyor duty. When a legacy part number conflicts with field measurements, hold the RFQ until the installed interface and the controlled drawing can be reconciled.
A useful enquiry combines commercial quantity with the technical package: power/load data, conveyor layout, attachments, speed and environment. Also state whether the request is a direct replacement, a planned modification or a new machine design. The release objective is to start from what the chain must carry and how it runs on tracks and sprockets, then choose the construction family. This reduces quote revisions and prevents a visually similar chain from being treated as interchangeable before geometry and duty have been checked.
Use the old reference if available, but verify the installed geometry and duty. Machine modifications, previous substitutions or wear can make a part number alone incomplete.
Use a multi-pitch measurement across a practical number of links and record the method. Compare it with the nominal pitch and machine maintenance limits rather than relying on one adjacent-link measurement.
Whenever tooth wear, hooking, alignment concerns or repeated premature chain wear are present. The chain and sprocket work as a meshing system.

























