Product Description
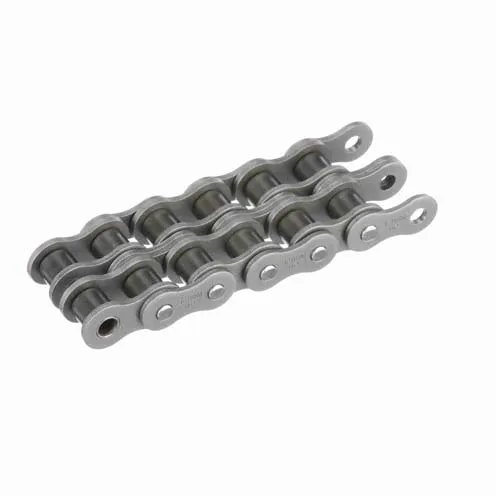
Stainless Steel Chrome Steel Industrial Roller Chain C2050 C2052 Double Pitch Conveyor Roller Chain With Extended Pins
Product Description
Roller chains conforms to ISO, ANSI, DIN, JIS and other standards. It adopts high-quality materials and advanced processing technology. The roller chains has the characteristics of high tensile strength and high fatigue strength. The roller chain is widely used in construction machinery, agricultural machinery, motorcycles, and automobile transmission. , food conveying machinery, logistics conveying machinery, packaging machinery and other fields, to transmit power for various mechanical facilities
1. Material: Stainless Steel 304 & 316 / Alloy Carbon Steel
2. Surface Treatment: Shot peening / Zinc-plated / Nickel-plated / Dacromet-plated
3. Chain No:
35SS-1, 40SS-1, 50SS-1, 60SS-1, 80SS-1, 100SS-1, 120SS-1, 140SS-1;
35SS-2, 40SS-2, 50SS-2, 60SS-2, 80SS-2, 100SS-2, 120SS-2, 140SS-2;
35SS-3, 40SS-3, 50SS-3, 60SS-3, 80SS-3, 100SS-3, 120SS-3, 140SS-3;
4. Application: Stainless Steel Chains are used in so many industries, such as machine manufacturing, food machine, etc. Also are suitable for high and low temperature conditions.
5. Characteristic:
1. The chain can be used on the both sides of multi-axle transmission.
2. Easy installation and replacement.
3. It can obtain larger reduction ratio.
4. The roller chain has good elasticity, high strength and each hinge part has lubricating oil, so it can be stored easliy. Thus, compared with the rigid contact tooth, it has good cushioning and vibration absorbing ability.
| Product Name | Stainless Steel Chrome Steel Industrial Roller Chain C2050 C2052 Double Pitch Conveyor Roller Chain With Extended Pins |
| Material | carbon steel,SS304, SS316, etc |
| Standard | DIN GB ISO JIS |
| DIN/ISO chain No. | C2050 C2052 C2060 C2062 C2080 C2082,ect |
| Key Words | Roller Chains |
| Application Area | Food processing, pharmaceutical and chemical industries, electronics, household appliances, automotive manufacturing, metallurgy, sewage treatment |
| Delivery time | 3-10 days depends on quantity needed |
Product Parameters
Company Profile
HangZhouTerry Machinery Co.,Ltd is a leading internatioal Machinery Manufacturer. The growing economics and convenient transportation of HangZhou benefits the development of Terry Machinery. Our products are utilized in commercial, industrial and custom application. Terry Machinery is specialized in engineering machinery bearing and vehicle industrial bearing. Our products have been exported over 53 countries.The goal of Terry Machinery is to provide out customers with widest range of products at lowest price, high quality with the best service.
Certifications
Our Advantages
1. World-Class Roller Chains
We provide our customers with all types of indigenous chains with world-class quality.
2. Free Samples:
We can provide free 1-10 meters,but you need bear shipping cost.
3. Genuine products With Excellent Quality:
The company has always proved the 100% quality products it provides with genuine intent.
4. Many Cheap International Forwarders:
We have many International forwarders partner and all kinds of shipping channel,keep sure your goods arrived yourside safe and fast.
5. Quick Delivery:
The company provides just-in-time delivery with its streamlined supply chain.
Packaging & Shipping
FAQ
1.What is the minimum order quantity for this product?
Depending on the size of the bearing, the MOQ is variable, if you are interested, you can contact me for a quote.
2.What is your latest delivery time?
Most orders will be shipped within 3-10 days of payment being received.
3.What are the advantages of your company’s services compared to other companies?
Answer questions online 24 hours a day, reply in a timely manner, and provide various documents required by customers for customs clearance or sales. 100% after-sales service.
4.Which payment method does your company support?
Do our best to meet customer needs, negotiable.
5.Do you accept OEM or customized service?
In addition to standard products, we also supply non-standard and modified standard products for special application. Meanwhile, we provide OEM service.
Please feel free to contact us, if you have any other question
| Standard or Nonstandard: | Standard |
|---|---|
| Application: | Textile Machinery, Garment Machinery, Conveyer Equipment, Packaging Machinery, Electric Cars, Motorcycle, Food Machinery, Marine, Mining Equipment, Agricultural Machinery, Car |
| Surface Treatment: | Polishing |
| Structure: | Roller Chain |
| Material: | Carbon Steel |
| Type: | Double Pitch Chain |
| Samples: |
US$ 2/Meter
1 Meter(Min.Order) | |
|---|
What are the considerations for selecting a low-maintenance conveyor chain?
When selecting a low-maintenance conveyor chain, several considerations should be taken into account:
1. Material Selection:
– Choose a conveyor chain made from materials that are resistant to wear, corrosion, and contamination. Stainless steel, plastic, or self-lubricating chains are commonly used for their durability and low maintenance requirements.
2. Lubrication-Free Design:
– Look for conveyor chains that have a self-lubricating design or are pre-lubricated with materials that reduce friction and eliminate the need for additional lubrication. This helps to minimize maintenance tasks associated with regular lubrication.
3. Sealed Construction:
– Consider conveyor chains with sealed construction to prevent the ingress of dirt, debris, and moisture. Sealed chains require less frequent cleaning and maintenance, making them ideal for low-maintenance applications.
4. Easy Cleaning:
– Opt for conveyor chains that are designed for easy cleaning. Smooth surfaces, open structures, and accessible components allow for quick and efficient cleaning, reducing maintenance time and effort.
5. Resistance to Contamination:
– Select a conveyor chain that is resistant to contamination. This includes resistance to chemicals, oils, greases, and other substances commonly found in the application environment. Chains that can withstand contamination require less frequent cleaning and maintenance.
6. Wear Monitoring:
– Look for conveyor chains that have wear monitoring features, such as wear indicators or sensors. These features help to identify chain wear and provide timely maintenance alerts, allowing for proactive replacement or adjustment.
7. Manufacturer Support:
– Consider the support provided by the chain manufacturer. A reputable manufacturer will offer guidance on maintenance intervals, replacement schedules, and provide technical assistance to ensure the proper functioning of the chain.
By considering these factors, you can select a low-maintenance conveyor chain that minimizes the need for frequent inspections, lubrication, cleaning, and replacement, resulting in reduced maintenance efforts and costs.
What are the benefits of using stainless steel conveyor chains?
Stainless steel conveyor chains offer several advantages over other types of chains. Here are some of the key benefits:
1. Corrosion Resistance: Stainless steel is highly resistant to corrosion, making it suitable for applications in harsh environments or industries where frequent washdowns or exposure to moisture is required. It does not rust or corrode like other metals, ensuring a longer lifespan and reliable performance.
2. Strength and Durability: Stainless steel chains are known for their high strength and durability. They can withstand heavy loads, high temperatures, and abrasive materials without deformation or breakage. This makes them ideal for heavy-duty applications where reliability and longevity are crucial.
3. Hygienic and Sanitary: Stainless steel is a non-porous material that is easy to clean and maintain. It is resistant to bacteria, mold, and other contaminants, making it suitable for industries with strict hygiene requirements such as food processing, pharmaceuticals, and medical devices. Stainless steel chains can be thoroughly cleaned and sanitized, reducing the risk of product contamination.
4. Temperature Resistance: Stainless steel chains can withstand a wide range of temperatures, both high and low. They exhibit excellent heat resistance, allowing them to maintain their strength and performance even in extreme temperature conditions.
5. Aesthetic Appeal: Stainless steel chains have a sleek and polished appearance, adding a professional and aesthetic touch to the conveyor system. They are commonly used in industries where visual appeal and brand representation are important, such as retail or luxury goods.
6. Chemical Resistance: Stainless steel is resistant to various chemicals, including acids, alkalis, and solvents. This makes it suitable for applications where contact with corrosive substances is likely.
7. Compatibility with High-Speed Applications: Stainless steel chains can withstand high-speed operations without compromising their structural integrity or performance. They maintain their stability and accuracy even at elevated speeds.
Overall, stainless steel conveyor chains offer corrosion resistance, strength, durability, hygienic properties, temperature resistance, aesthetic appeal, chemical resistance, and compatibility with high-speed applications. These benefits make them a preferred choice in industries such as food and beverage, pharmaceuticals, automotive, and manufacturing, where reliability, cleanliness, and performance are essential.

What are the cost considerations when purchasing a conveyor chain?
When purchasing a conveyor chain, there are several cost considerations that need to be taken into account to ensure an optimal investment and operational efficiency.
1. Initial Cost: The initial cost of the conveyor chain includes the cost of the chain itself, as well as any additional components such as sprockets, attachments, and connecting links. It is important to compare prices from different suppliers and evaluate the overall value for the money.
2. Maintenance and Repair Costs: Consider the long-term maintenance and repair costs associated with the conveyor chain. Some chains may require more frequent lubrication or replacement of components, which can add to the overall operating expenses.
3. Service Life: The service life of the conveyor chain is an essential factor in determining its cost-effectiveness. Chains with longer service life may have a higher initial cost but can result in lower replacement and downtime costs in the long run.
4. Energy Efficiency: Energy consumption is an ongoing cost to consider. Conveyor chains that offer lower friction and efficient power transmission can contribute to energy savings and reduce operating expenses.
5. Maintenance Ease: Consider the ease of maintenance when selecting a conveyor chain. Chains that are easier to clean, inspect, and maintain can reduce labor costs and increase operational efficiency.
6. Compatibility and Integration: Ensure that the selected conveyor chain is compatible with the existing conveyor system or equipment. Retrofitting or modifying the system to accommodate a specific chain may incur additional costs.
7. Supplier Support and Warranty: Evaluate the level of technical support provided by the supplier and the warranty coverage offered for the conveyor chain. This can impact the overall cost of ownership and provide peace of mind in case of any unforeseen issues.
It is important to consider these factors holistically and make a cost-benefit analysis based on the specific requirements of the application. Choosing a conveyor chain that aligns with the budget, performance needs, and long-term cost considerations will help optimize the investment and ensure efficient material handling operations.


editor by CX 2023-12-01

























