Product Description
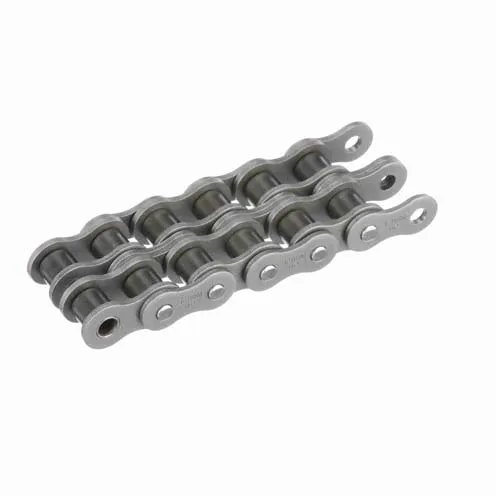
Stainless Steel Chain
Strength:
1. For Free Samples
2. Prompt Delivery
3. Green Product
4. International Approvals
5. Experienced Staff
Catalogue
1. Stainless steel roller chains
2. Short pitch stainless steel conveyor chain with attachments
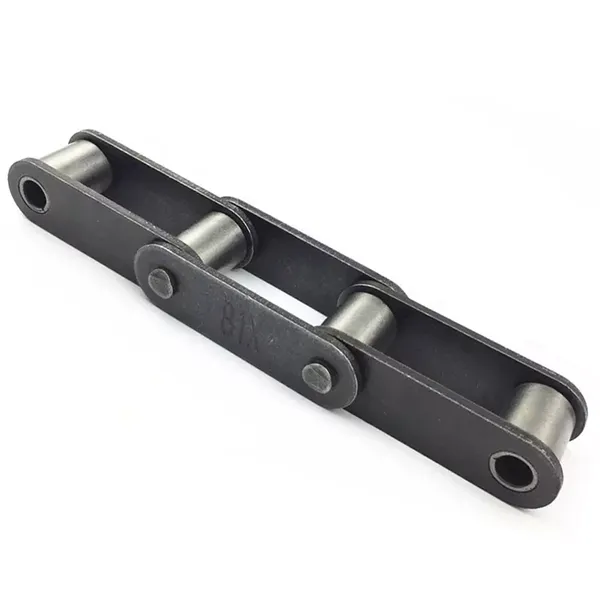
3. Double pitch stainless steel conveyor chains
4. Double pitch stainless steel conveyor chain with attachments
5. Stainless steel hollow pin chains
Why Choose Us?
1. HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd established in 1991, we have 5 subsidiaries in China and have 6 subsidiaries abroad;
2. We covering a production area of 200, 100 square meters, have more than 1, 800 sets of advanced equipment and over 3, 100 highly skilled employees, the annual production capacity has exceeded 20, 000, 000meters;
3. We specialized in producing all kinds of standard chains and special chains, such as A or B series chains, driving chains, conveyor chains, dragging chains, agricultural chains and so on;
4. We have obtained ISO9001, ISO14001, ISO16969, AAA and API certificates.
We look CZPT to receiving your enquires soon.
| Usage: | Transmission Chain |
|---|---|
| Material: | Stainless steel |
| Surface Treatment: | Polishing |
| Feature: | Heat Resistant |
| Chain Size: | 1/2"*3/32" |
| Structure: | Roller Chain |
| Customization: |
Available
| Customized Request |
|---|

Can a conveyor chain be used in high-load applications?
Yes, a conveyor chain can be used in high-load applications. Conveyor chains are designed to withstand heavy loads and provide reliable and efficient material handling in various industries. Here’s a detailed explanation:
– Robust Construction:
A conveyor chain for high-load applications is typically constructed using durable materials such as alloy steel or stainless steel. These chains are designed to withstand the forces and stresses imposed by heavy loads without deformation or failure.
– High Load Capacity:
Conveyor chains for high-load applications are designed with larger and stronger components, including thicker plates, larger pins, and stronger attachments. These enhancements allow the chain to handle heavier loads and distribute the weight evenly across the chain’s links and rollers.
– Proper Selection:
When using a conveyor chain in high-load applications, it is crucial to select the appropriate chain type and size based on the specific load requirements. Factors such as the weight of the conveyed material, the conveyor speed, and the operating conditions should be considered during the selection process.
– Lubrication and Maintenance:
In high-load applications, proper lubrication and regular maintenance of the conveyor chain are essential. Adequate lubrication reduces friction and wear, ensuring smooth operation and extending the chain’s service life. Regular inspections and maintenance routines help identify any issues or wear that may affect the chain’s performance.
– Application-Specific Chains:
In some cases, specialized conveyor chains, such as forged link chains or roller chains, are used to handle extremely heavy loads. These chains offer enhanced strength and durability, making them suitable for demanding high-load applications.
Overall, a properly selected and maintained conveyor chain can reliably handle high-load applications, providing efficient and continuous material handling in industries such as mining, construction, automotive, and heavy manufacturing.
What are the benefits of using stainless steel conveyor chains?
Stainless steel conveyor chains offer several advantages over other types of chains. Here are some of the key benefits:
1. Corrosion Resistance: Stainless steel is highly resistant to corrosion, making it suitable for applications in harsh environments or industries where frequent washdowns or exposure to moisture is required. It does not rust or corrode like other metals, ensuring a longer lifespan and reliable performance.
2. Strength and Durability: Stainless steel chains are known for their high strength and durability. They can withstand heavy loads, high temperatures, and abrasive materials without deformation or breakage. This makes them ideal for heavy-duty applications where reliability and longevity are crucial.
3. Hygienic and Sanitary: Stainless steel is a non-porous material that is easy to clean and maintain. It is resistant to bacteria, mold, and other contaminants, making it suitable for industries with strict hygiene requirements such as food processing, pharmaceuticals, and medical devices. Stainless steel chains can be thoroughly cleaned and sanitized, reducing the risk of product contamination.
4. Temperature Resistance: Stainless steel chains can withstand a wide range of temperatures, both high and low. They exhibit excellent heat resistance, allowing them to maintain their strength and performance even in extreme temperature conditions.
5. Aesthetic Appeal: Stainless steel chains have a sleek and polished appearance, adding a professional and aesthetic touch to the conveyor system. They are commonly used in industries where visual appeal and brand representation are important, such as retail or luxury goods.
6. Chemical Resistance: Stainless steel is resistant to various chemicals, including acids, alkalis, and solvents. This makes it suitable for applications where contact with corrosive substances is likely.
7. Compatibility with High-Speed Applications: Stainless steel chains can withstand high-speed operations without compromising their structural integrity or performance. They maintain their stability and accuracy even at elevated speeds.
Overall, stainless steel conveyor chains offer corrosion resistance, strength, durability, hygienic properties, temperature resistance, aesthetic appeal, chemical resistance, and compatibility with high-speed applications. These benefits make them a preferred choice in industries such as food and beverage, pharmaceuticals, automotive, and manufacturing, where reliability, cleanliness, and performance are essential.
What are the common causes of conveyor chain failures?
Conveyor chain failures can occur due to various reasons, and identifying the root cause is crucial for preventing future issues. Here are some common causes of conveyor chain failures:
- Lack of Lubrication: Insufficient or improper lubrication can lead to increased friction and wear on the chain components, resulting in premature failure.
- Excessive Load: Overloading the conveyor chain beyond its rated capacity can cause excessive stress and strain, leading to chain elongation, deformation, or link breakage.
- Misalignment: Improper alignment of the conveyor chain can cause uneven loading and excessive wear on specific areas, leading to chain failure.
- Environmental Factors: Harsh operating environments, such as high temperatures, corrosive substances, or abrasive materials, can accelerate chain wear and corrosion, leading to failure.
- Foreign Objects: The presence of foreign objects or debris on the conveyor system can interfere with the movement of the chain, causing jamming, binding, or chain damage.
- Poor Maintenance: Inadequate maintenance practices, such as irregular inspections, failure to address minor issues promptly, or neglecting to replace worn components, can contribute to chain failures.
- Incorrect Installation: Improper installation, including incorrect tensioning, misalignment, or using incompatible components, can result in premature chain failure.
- Fatigue and Wear: Continuous operation over time can lead to fatigue and wear in the chain, especially in high-speed or heavy-duty applications, resulting in eventual failure.
Regular maintenance, proper lubrication, adequate training for operators, and adherence to manufacturer guidelines can help mitigate these common causes of conveyor chain failures. Conducting routine inspections, promptly addressing issues, and replacing worn components can also significantly extend the life of the conveyor chain.


editor by CX 2023-09-13

























