Product Description
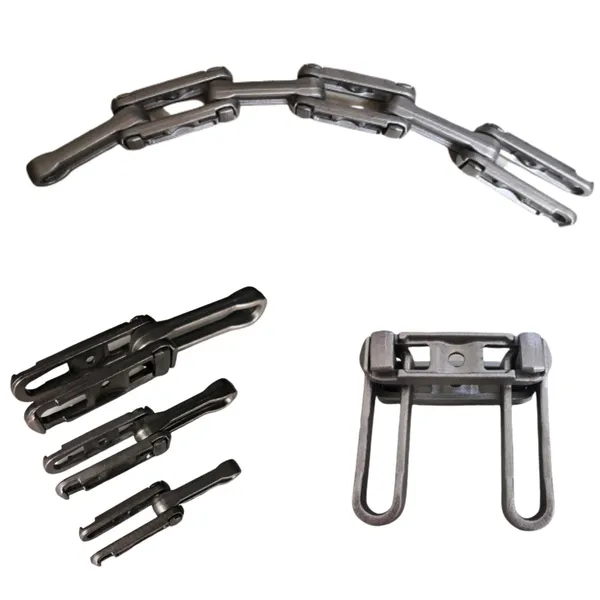
MC Series Hollow Pin Chains:
Carbon Steel and Stainless Steel Hollow Pin Chain for food handling conveyors. Products are available in ANSI standard series, double pitch series with standard rollers, and large rollers.
This chain has hollow pins so that the holes can be used to mount various pins and attachments.
| Product Name |
MC Series Hollow Pin Chains |
| Type | MC28, MC56, MC112, MC224 |
| Colour | primary |
| Material | carbon steel, alloy steel,stainless steel |
| Customize | YES |
| OEM | YES |
| Surface Treatment | rust-preventative oil |
| Shipping Type | sea & air |
| Market | global |
| Payment Terms | T/T in advance |
| Packaging | carton,wooden case,pallet |
Main products:
Transmission Chains:
Standard Roller Chains/ Nickel-Plated Roller Chain/ Stainless Steel Roller Chain/ Bicycle Chain/ Motorcycle Chain/ Chains for Automotive Engines/ Leaf Chains/ Silent Chain.
Conveyor Chains:
Small Size Conveyor Chains/ Large Size Conveyor Chains/ Roller Conveyor Chain/ Hollow Pin Chain/ Drive Chain/ Steel Bushing Chain/ Welded Steel Mill Chain/ Welded Steel Drag Chain/ Barloop Chain/ Drop Forged Rivetless Chain/ Caterpiller Drive Chain/ Cast Combination Chain/ Cast Pintle Chain/ Double Flex Chain/ Specialty Chain/ Plastic Top Chain/ Snap Cover Chain.
Link Chains:
Grade 120 Alloy Chain/ Grade 100 Alloy chain/ Grade 80 Lifting Chain/ Grade 70 Transport Chain/ Grade 50 Stainless Steel Chain/ Grade 43 High Test Chain/ Grade 40 High Test chain/ Grade 30 Proof Coil Chain/ Double Loop Chain/ Single Jack Chain/ Twist Chain/ Register Chain/ Ball Chain/ Oval Link/ Square Chain.
Sprockets:
Single Type A Hub/ Single Type B Hub/ Single Type C Hub/ Single Type D Hub/ Double Strand Type B Hub/ Double Strand Type C Hub/ Hardened Teeth Type A/ Double Single Type A Sprocket/ Double Pitch Strand Type B Hub/ Large Roller Double Pitch Sprocket.
Gear & Rack:
Spur Gears/ Helical Gears/ Bevel Gear/ Hypoid Gears/ Worm Gear/ Internal Helical Gear/ Herringbone Gears/ Rack And Pinion Gears/ Sector Gear/ Internal Ring Gear/ Miter Gears/ Nylon Gear Rack.
Wire Mesh:
Woven Wire Mesh/ Plain Weave/ Twilled Weave/ Plain Dutch Weave/ Twilled Dutch Weave/ Reverse Plain Dutch Weave/ Reverse Twilled Dutch Weave/ Five Heddle Weave/ Super Mesh Weave/ Welded Wire Mesh/ Wire Mesh Belt.
Shackles:
Screw Pin Anchor Shackle/ Round Pin Anchor Shackle/ Bolt Type Safety Anchor Shackle/ Screw Pin Chain Shackle/ Round Pin Chain Shackle/ Bolt Type Safety Chain Shackle.
Hooks:
Clevis Sling Hook/ Clevis Grab Hook/ Eye Sling Hooks/ Eye Grab Hook/ Clevis Foundry Hooks.
Riggings:
Chain Hoists/ Wire Rope Clip/ Link/ Coupling Link/ Quick Link/ Snap Hooks/ Eye Bolt/ Turnbuckle/ Anchor Rod/ Swivels/ Cable Thimble.
Machinery Equipment:
Belt conveyors/ Scraper Conveyor/ Chain Conveyor/ Plate Conveyor/ Roller Conveyor/ Spiral Conveyor/ Elevator Conveyors/ Incline Conveyor/ Vegetable And Fruit Processing Machines/ Food Processing Machinery/ Dairy Processing Equipment/ Slaughtering Equipment/ Brewing Equipment/ Frozen Drink Machine.
Company information:
We are engaged in the import and export of Mechanical Hardware.
We have professional factory. Technology is strong in products of different specifications complete, has strong product development and manufacturing capacity.to provide all kinds of hardware tools products, specifications complete, variety, quality, reasonable price.
Our Advantages:
Our company has over 20 years’ experience producing high-quality hardware products.
The products are reliable and we can manufacture the products according to customers’ requirement.
We can also cooperate with customers to develop new products.
Our products have been certified by CE and ROHS, also can provide customized product Certificate.
We sincerely welcome domestic and foreign, new and old customers to carry on the cooperation and exchange with us, and establish a long-time cooperative relationship.
Company Name: HangZhou CHINAMFG Jin Hao International Trade Co., Ltd.
/* March 10, 2571 17:59:20 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Material: | Alloy |
|---|---|
| Structure: | Hollow Chain |
| Surface Treatment: | Oxygenation |
| Chain Size: | 1/2"*11/128" |
| Feature: | Oil Resistant |
| Chain No.: | Mc56 |
| Samples: |
US$ 10/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
Can a conveyor chain be used in cleanroom environments?
Yes, conveyor chains can be used in cleanroom environments with proper selection and design considerations. Cleanroom environments require stringent control of airborne particles, such as dust, microbes, and contaminants, to maintain high levels of cleanliness. Here are some factors to consider when using a conveyor chain in a cleanroom:
1. Material Selection:
– Choose a conveyor chain made from materials that are compatible with cleanroom requirements. Stainless steel, plastic, or special coatings are commonly used for their clean and non-contaminating properties.
– Avoid materials that generate excessive particles or contaminants, such as certain types of lubricants or chain coatings.
2. Design Considerations:
– Design the conveyor chain system to minimize particle generation. This includes smooth surfaces, rounded edges, and avoiding areas that can trap or accumulate particles.
– Use sealed or enclosed chain designs to prevent the release of lubricants or contaminants.
– Consider the integration of additional features, such as covers or guards, to further protect the chain and prevent particle ingress.
3. Cleaning and Maintenance:
– Establish a cleaning and maintenance protocol specific to the cleanroom environment. This may include regular cleaning and sanitization procedures to maintain cleanliness standards.
– Use cleaning agents and procedures that are approved for cleanroom use and do not introduce contaminants.
– Regularly inspect the conveyor chain system for any signs of wear, damage, or contamination. Promptly address any issues to ensure the chain’s reliability and cleanliness.
4. Compliance with Cleanroom Standards:
– Ensure that the conveyor chain system meets the cleanliness and particle generation requirements of the specific cleanroom standards or classifications in which it will be used.
– Comply with relevant industry guidelines and regulations, such as ISO standards, when selecting and using conveyor chains in cleanroom environments.
By considering these factors and implementing proper material selection, design considerations, cleaning protocols, and compliance with cleanroom standards, a conveyor chain can be effectively used in cleanroom environments while maintaining the required cleanliness levels.
How does lubrication affect the performance of a conveyor chain?
Lubrication plays a crucial role in the performance and longevity of a conveyor chain. Proper lubrication helps to reduce friction, wear, and heat generation, ensuring smooth operation and minimizing the risk of premature failure. Here’s how lubrication affects the performance of a conveyor chain:
1. Friction Reduction: Lubrication forms a thin film between the chain components, reducing friction between metal surfaces. This reduces the energy required for operation, minimizes heat generation, and prevents excessive wear and tear.
2. Wear Prevention: Lubrication forms a protective layer on the chain components, preventing direct metal-to-metal contact. This helps to reduce wear and extend the service life of the chain.
3. Corrosion Protection: Lubricants often contain anti-corrosion additives that protect the chain from rust and oxidation. This is particularly important in environments with high humidity or exposure to corrosive substances.
4. Noise Reduction: Proper lubrication reduces the noise generated during chain operation by minimizing friction and metal-to-metal contact. This can contribute to a quieter and more comfortable working environment.
5. Temperature Control: Lubrication helps to dissipate heat generated during chain operation, preventing excessive temperature rise. This is crucial in high-speed or heavy-duty applications where heat can lead to accelerated wear and reduced chain performance.
6. Maintenance and Service Life: Regular lubrication and proper lubricant selection are essential for maintaining the chain’s performance and extending its service life. Adequate lubrication reduces the need for frequent maintenance, minimizes downtime, and lowers overall operating costs.
It’s important to follow the manufacturer’s recommendations for lubrication frequency and use the appropriate lubricant for the conveyor chain. Regular inspections and maintenance checks should also be conducted to ensure proper lubrication levels and address any issues promptly. Proper lubrication practices will enhance the performance, reliability, and durability of the conveyor chain system.

What are the cost considerations when purchasing a conveyor chain?
When purchasing a conveyor chain, there are several cost considerations that need to be taken into account to ensure an optimal investment and operational efficiency.
1. Initial Cost: The initial cost of the conveyor chain includes the cost of the chain itself, as well as any additional components such as sprockets, attachments, and connecting links. It is important to compare prices from different suppliers and evaluate the overall value for the money.
2. Maintenance and Repair Costs: Consider the long-term maintenance and repair costs associated with the conveyor chain. Some chains may require more frequent lubrication or replacement of components, which can add to the overall operating expenses.
3. Service Life: The service life of the conveyor chain is an essential factor in determining its cost-effectiveness. Chains with longer service life may have a higher initial cost but can result in lower replacement and downtime costs in the long run.
4. Energy Efficiency: Energy consumption is an ongoing cost to consider. Conveyor chains that offer lower friction and efficient power transmission can contribute to energy savings and reduce operating expenses.
5. Maintenance Ease: Consider the ease of maintenance when selecting a conveyor chain. Chains that are easier to clean, inspect, and maintain can reduce labor costs and increase operational efficiency.
6. Compatibility and Integration: Ensure that the selected conveyor chain is compatible with the existing conveyor system or equipment. Retrofitting or modifying the system to accommodate a specific chain may incur additional costs.
7. Supplier Support and Warranty: Evaluate the level of technical support provided by the supplier and the warranty coverage offered for the conveyor chain. This can impact the overall cost of ownership and provide peace of mind in case of any unforeseen issues.
It is important to consider these factors holistically and make a cost-benefit analysis based on the specific requirements of the application. Choosing a conveyor chain that aligns with the budget, performance needs, and long-term cost considerations will help optimize the investment and ensure efficient material handling operations.


editor by CX 2024-01-11

























