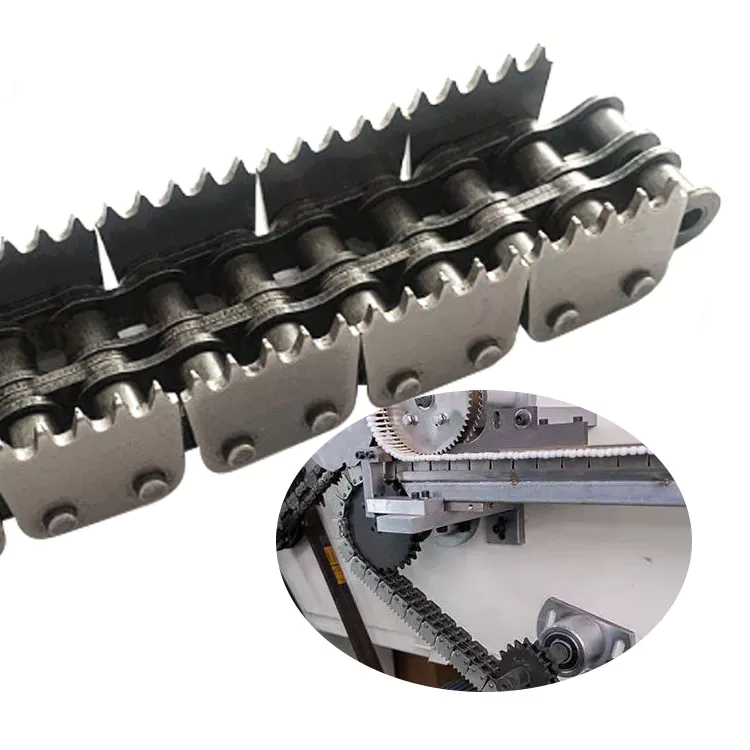
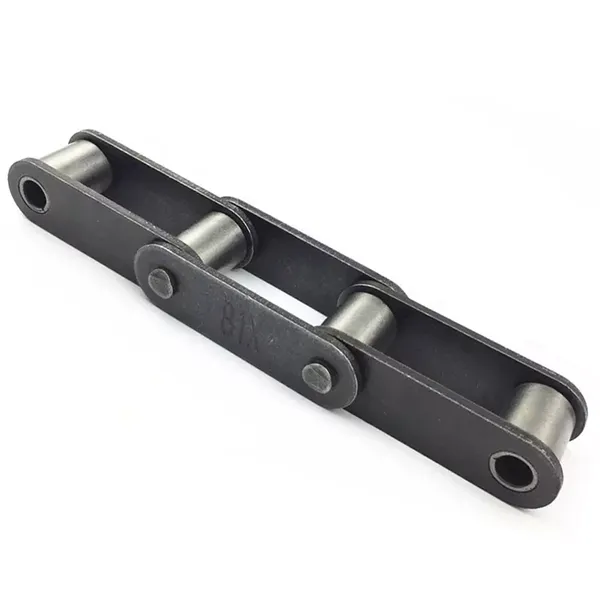
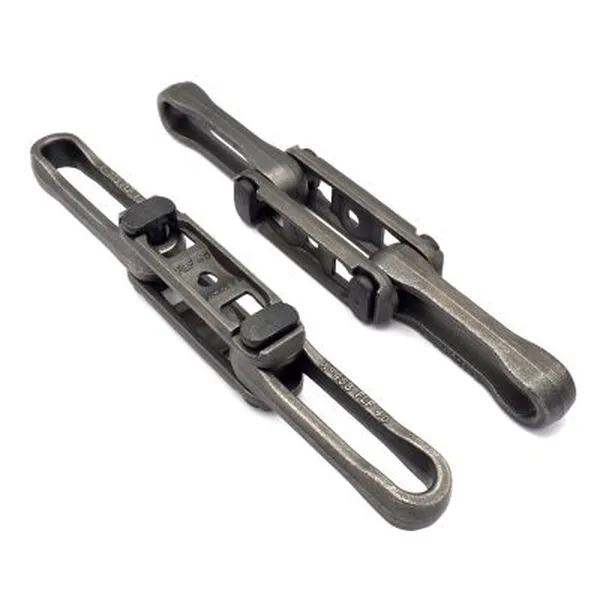
Product Description
| DIN Chain No. | ISO/ANSI Chain No. | P/mm | d1/mm | L/mm | b1/mm | T/mm | |||||||||||||||||||||||||||
| 08A-1 | 40 | 12.70 | 7.92 | 16.70 | 7.85 | 1.50 | |||||||||||||||||||||||||||
| 10A-1 | 50 | 15.875 | 10.16 | 20.70 | 9.40 | 2. Abbreviation: CHOHO Industry. √ HangZhou CHOHO Industrial Co., Ltd. was founded in 1999. Has become the leader of chain system technology, the first batch of natioal recognized enterprise technology center,national technology innovation demonstration enterprise,and the first A-share listed company in China’s chain drive industry.The securities code is 003033.
We are very close to the port of HangZhou, which saves a lot of logistics costs and transportation time! We have our own logistics company and transportation department. If you need me to deliver goods to your warehouse or other ports in China, such as ZheJiang Port and ZheJiang Port, we can also do it!
√ CHOHO has a natural brand awareness. As of January 2571, CHOHO has registered the “CHOHO” trademark in more than 60 countries, including the United States, Japan, the United Kingdom, France, Germany, Russia, Spain, Austria, Belgium, Bulgaria, Croatia, Czech Republic, Denmark, Finland, Greece , Hungary, Ireland, Italy, Netherlands, Poland, Portugal, Romania, Ukraine, Sweden, Australia, Algeria, Egypt, Kenya, Morocco, South Korea, Kazakhstan, Mongolia, Syria, Thailand, Pakistan, India, Brazil, Mexico, Colombia, etc. CHOHO has been invited to participate in many international exhibitions around the world, including industrial exhibitions, agricultural exhibitions, motorcycle exhibitions, engine exhibitions, such as Hannover Messe, Bologna Fair, Canton Fair ,VIV ASIA and other world famous exhibitions! COOPERATIVE CLIENT Broad Customer Channels Market Continues to Develop! Choho Provide Chain System Solutions for The Global Top 500 and The Enterprises in Various Fields Top 10! FAQ
1. Are you a Manufacturer or Trade Company? OTHER HOT SELL PRODUCTS
Thx for Reading!
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
.shipping-cost-tm .tm-status-off{background: none;padding:0;color: #1470cc}
What are the benefits of using a silent conveyor chain?A silent conveyor chain, also known as a noise-reducing conveyor chain, offers several advantages in conveyor system applications: 1. Noise Reduction: – One of the primary benefits of using a silent conveyor chain is the significant reduction in noise levels. These chains are specifically designed to minimize the noise generated during operation, creating a quieter and more comfortable working environment. 2. Improved Work Environment: – By reducing noise levels, a silent conveyor chain contributes to a better work environment, particularly in settings where noise reduction is important, such as manufacturing facilities, warehouses, and distribution centers. It helps reduce employee fatigue, enhances communication, and improves overall worker satisfaction. 3. Compliance with Noise Regulations: – In some industries or regions, there are specific noise regulations that must be met. Using a silent conveyor chain helps ensure compliance with these regulations, avoiding potential penalties and legal issues. 4. Increased Productivity: – A quieter working environment created by a silent conveyor chain can lead to increased productivity. With reduced noise distractions, employees can focus better on their tasks, resulting in improved efficiency and output. 5. Extended Chain and Equipment Life: – Silent conveyor chains are often designed with advanced materials and technologies that offer enhanced wear resistance and durability. They can withstand heavy loads, reduce friction, and minimize wear and tear on both the chain and the associated equipment, resulting in longer service life and reduced maintenance costs. 6. Versatility: – Silent conveyor chains are available in various configurations and designs, making them compatible with a wide range of conveyor systems and applications. They can be used in different industries, including automotive, food processing, packaging, and more. When considering a silent conveyor chain, it is important to consult with a reputable chain manufacturer or supplier to ensure the chain meets the specific requirements of the application.
What are the future trends and advancements in conveyor chain technology?The field of conveyor chain technology is constantly evolving, driven by the need for improved efficiency, productivity, and sustainability. Here are some of the future trends and advancements in conveyor chain technology: 1. Automation and robotics: The integration of conveyor chains with automation and robotics systems is a growing trend. This includes the use of advanced sensors, machine vision, and artificial intelligence to enable autonomous operation, precise positioning, and efficient material handling. 2. Smart and connected systems: Conveyor chains are becoming increasingly connected through the Internet of Things (IoT) technology. This allows for real-time monitoring, data collection, and analysis of various performance parameters such as chain wear, tension, temperature, and energy consumption. Smart systems can optimize maintenance schedules, detect potential failures, and improve overall system efficiency. 3. Lightweight and high-strength materials: The development of lightweight yet high-strength materials is an ongoing focus in conveyor chain technology. Advanced alloys, composites, and engineered plastics offer improved strength-to-weight ratios, reducing energy consumption and increasing the load capacity of conveyor systems. 4. Energy efficiency: Energy efficiency is a key consideration in conveyor chain design. Future advancements aim to minimize power consumption through the use of efficient drive systems, regenerative braking, and smart control algorithms that optimize speed and acceleration profiles. Energy recovery technologies, such as regenerative drives, can also capture and reuse energy during deceleration or braking. 5. Sustainability and environmental friendliness: Conveyor chain technology is moving towards more sustainable and environmentally friendly solutions. This includes the use of eco-friendly materials, improved lubrication techniques to minimize environmental impact, and the adoption of energy-efficient components and systems. Recycling and circular economy concepts are also gaining prominence in the design and manufacturing of conveyor chains. 6. Advanced wear monitoring and predictive maintenance: The future of conveyor chain technology involves advanced wear monitoring systems that can accurately predict the remaining useful life of chains and components. This enables proactive maintenance planning and reduces unplanned downtime. Predictive maintenance algorithms analyze data collected from sensors and provide timely alerts for chain replacement or repair. These are just a few examples of the future trends and advancements in conveyor chain technology. As technology continues to advance, we can expect further innovations that enhance performance, efficiency, reliability, and sustainability in conveyor systems.
What are the environmental considerations when using a conveyor chain?When using a conveyor chain, there are several environmental considerations to take into account: 1. Temperature and Humidity: Conveyor chains may be exposed to different temperature and humidity levels depending on the application and operating environment. Extreme temperatures or high humidity can affect the performance and lifespan of the chain. It is important to select a chain material and lubrication that can withstand the specific environmental conditions. 2. Contamination and Cleanliness: The presence of dust, dirt, debris, or other contaminants can impact the operation and efficiency of the conveyor chain. Regular cleaning and maintenance should be performed to prevent build-up and ensure smooth chain movement. 3. Chemical Exposure: Conveyor chains used in industries such as chemical processing or food production may come into contact with corrosive chemicals or cleaning agents. It is crucial to choose a chain material that is resistant to chemical corrosion and select appropriate lubricants compatible with the chemicals present in the environment. 4. Noise and Vibration: Conveyor systems can generate noise and vibration during operation, which may have environmental implications. Noise reduction measures, such as using noise-dampening materials or implementing vibration isolation techniques, can help minimize the impact on the surrounding environment and comply with noise regulations. 5. Energy Efficiency: Consideration should be given to energy consumption and efficiency when using a conveyor chain. Optimize the system design, minimize friction losses, and utilize energy-efficient components to reduce the environmental impact and operational costs. 6. Sustainability: Increasingly, sustainability is an important consideration in industrial operations. Choosing conveyor chains made from recyclable or renewable materials, implementing energy-saving measures, and practicing responsible waste management can contribute to a more environmentally friendly operation. By taking these environmental considerations into account, industries can ensure the proper functioning of conveyor chains while minimizing environmental impact and complying with relevant regulations.
|