Product Description
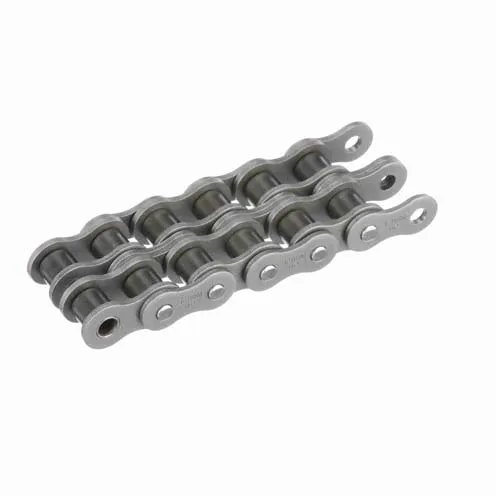
Double Pitch Transmission Chains with K1 Attachments -2040k1
A. Our Services:
1. Any of your kind inquiry about chain would be replied within 24 hours.
2. Well-trained and experienced sales staffs will reply all your concerns in fluent English.
3. OEM services are available with us, our professional designer would make your private idea into being.
4. Protection of your sales area, ideas of design and all your private information.
5. Delivery by air mail or ship for your orders.
6. With years of manufacture and promotion experience in global market, brings you profit and great success!
B.Technical parameters
C. Company show & Product Process
D. Packaging
| Packaging Details: | Chain+Plastic Bag+Neutral Box+Wooden case+Big Carton+Steel Pallets |
| Delivery Detail: | five weeks |
E. FAQ:
1. Are you manufacturer or trade Company?
We are a factory founded in 1991 with trade team for international service.
2. What terms of payment you usually use?
T/T 30% deposit and 70% against document, Western Union, L/C at sight
3. what is your lead time for your goods?
Normally 45 days after confirmed order. 30 days could be available in low season for some items (during May to July), and 65 days during new year and hot season ( Jan to March).
4. Do you attend any Show?
We attend Hannover show in Germany, NMW in Austrilia, Canton fair, PTC, in China and many other special furniture shows.
| Usage: | Transmission Chain |
|---|---|
| Material: | Alloy/Carbon Steel |
| Surface Treatment: | Oil Blooming |
| Feature: | Heat Resistant |
| Chain Size: | 1/2"*3/32" |
| Structure: | Roller Chain |
| Customization: |
Available
| Customized Request |
|---|

Can a conveyor chain be used in pharmaceutical manufacturing?
Yes, conveyor chains can be used in pharmaceutical manufacturing for various applications. Conveyor systems play a crucial role in the efficient and safe transportation of pharmaceutical products throughout the manufacturing process. Here are some key considerations when using conveyor chains in pharmaceutical manufacturing:
1. Material Selection:
– Choose conveyor chains made from materials that are suitable for pharmaceutical applications, such as stainless steel or FDA-approved plastic. These materials offer corrosion resistance, cleanliness, and compliance with industry regulations.
2. Cleanliness and Sanitation:
– Ensure that the conveyor chain design allows for easy cleaning and sanitation. Smooth surfaces, minimal crevices, and access for cleaning equipment are important to maintain a hygienic environment.
3. Contamination Control:
– Implement measures to prevent contamination of pharmaceutical products. This includes using chain lubricants that are safe for pharmaceutical applications and implementing proper handling and storage procedures.
4. Product Protection:
– Choose conveyor chain systems that minimize product damage or degradation. This can include utilizing gentle product handling features such as low-friction surfaces, adjustable speed controls, and proper product spacing.
5. Regulatory Compliance:
– Ensure that the conveyor chain system complies with pharmaceutical industry regulations and guidelines, such as Good Manufacturing Practices (GMP) and the requirements of regulatory bodies like the FDA.
6. Integration with Equipment:
– Consider the integration of conveyor chains with other equipment in the pharmaceutical manufacturing process, such as labeling machines, filling machines, and packaging equipment. The conveyor system should provide seamless operation and synchronization with these machines.
By carefully selecting and designing conveyor chains specifically for pharmaceutical manufacturing, it is possible to meet the stringent requirements of the industry in terms of cleanliness, product integrity, and regulatory compliance.
What are the benefits of using a modular conveyor chain system?
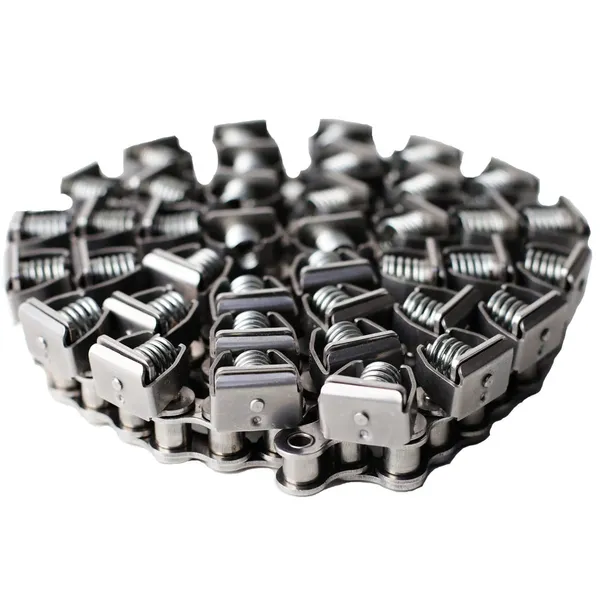
A modular conveyor chain system offers several benefits in terms of flexibility, efficiency, and ease of maintenance. Here are some key advantages:
1. Versatility: Modular conveyor chains are designed with interlocking modules that can be easily connected and disconnected. This allows for flexibility in configuring the conveyor system according to specific layout requirements, production needs, or space limitations. Modules can be added, removed, or repositioned to accommodate changing production processes or product variations.
2. Customizability: The modular design of the conveyor chain system enables customization to meet specific application requirements. Different types of modules are available, including straight sections, curves, inclines, declines, merges, and diverters. Accessories such as side guides, cleats, or product hold-downs can be easily integrated into the system.
3. Quick Installation and Modification: Modular conveyor chains are designed for easy installation and modification. With their snap-in or snap-on connections, modules can be rapidly assembled or disassembled, reducing downtime during system setup or reconfiguration. This feature also facilitates maintenance, repairs, or future expansions.
4. Enhanced Efficiency: The modularity of the conveyor chain system allows for efficient material handling and optimized workflow. The smooth transfer between modules minimizes product jams or misalignments, ensuring a continuous and consistent flow of materials. The ability to incorporate curves or inclines in the system enables efficient use of floor space and facilitates the movement of products through different elevations.
5. Easy Maintenance: Modular conveyor chain systems are designed for ease of maintenance. Individual modules can be easily accessed and replaced without disassembling the entire system. This reduces maintenance time and costs. Additionally, the open structure of the modules allows for easy cleaning, debris removal, and inspection.
6. Durability and Reliability: Modular conveyor chains are typically made from high-quality materials such as plastic or stainless steel, ensuring durability and long-lasting performance. They are resistant to wear, corrosion, and chemical damage, making them suitable for various industrial environments. The interlocking design provides stability and prevents chain slippage during operation.
7. Safety Features: Modular conveyor chain systems can incorporate safety features such as emergency stop buttons, safety guarding, or sensors for detecting blockages or excessive loads. These features help maintain a safe working environment for operators and protect the integrity of the products being transported.
Overall, a modular conveyor chain system offers versatility, customizability, efficiency, and ease of maintenance. It is a reliable solution for material handling in industries such as manufacturing, packaging, distribution, and logistics.
What is a conveyor chain and how does it work?
A conveyor chain is a type of mechanical chain specifically designed for use in conveyor systems. It is composed of a series of interconnected links that form a continuous chain loop. The links are typically made of metal and are joined together through pins or other connecting elements.
Conveyor chains work by transferring power and motion from the driving mechanism, such as a motor or sprocket, to the conveyor system to move materials or products along a predetermined path. The chain is placed on a track or guide rails, and as it moves, it carries the load placed on it.
The operation of a conveyor chain involves the following steps:
- Power transmission:
The driving mechanism transfers rotational power to the conveyor chain, typically through a motor and sprockets. The motor provides the necessary torque to drive the chain.
- Traction and motion:
As the driving mechanism rotates the sprockets, the teeth of the sprockets engage with the links of the conveyor chain. This interaction creates traction, causing the chain to move along the desired path.
- Load carrying:
The load to be transported is placed on the conveyor chain. The load can be in the form of products, materials, or other items. As the chain moves, it carries the load along the conveyor system, allowing for efficient transportation or handling.
- Support and guidance:
The conveyor chain is supported and guided by various components, such as guide rails, rollers, or wear strips. These components ensure the proper alignment and smooth movement of the chain along the conveyor system.
Conveyor chains are commonly used in industries such as manufacturing, logistics, packaging, and material handling. They offer a reliable and efficient method for moving products or materials in a controlled and automated manner.


editor by CX 2023-10-16

























