PROOFER CHAINS • BAKERY OVEN CHAINS • STAINLESS STEEL CHAINS • ATTACHMENT CHAINS • HOLLOW PIN CHAINS • CUSTOM REPLACEMENT • PROOFER CHAINS • BAKERY OVEN CHAINS • STAINLESS STEEL CHAINS • ATTACHMENT CHAINS • HOLLOW PIN CHAINS • CUSTOM REPLACEMENT
Product Description
Professional Powder Coating Production Line Plant Automatic Spray Painting Line XT Forged Overhead Conveyor Chain For Painting Line Steel Beams Shot
We can supply painting line chain
Our drop forged rivetless chain such as X348, X458, X468, X678, X698, F100, F160 and so on
Our products are most competitive and are of high quality. Our trolley are also most competitive in world market.
We are also supplier of detachable chain: 25, 32, 32W, 45, 51, 52, 55, 62 chain and so on. Which is used widely on agricultural machine. Please feel free to contact with us and our goods are most competitive in your market.
Our Drop Forged Chain and trolley can be used widely in aggregate, amusement park rides, asphalt paving, automotive industry, bakery ovens, bottling, bucket elevators, car dumper, car wash, case conveyors, cement plants, citrus processing, clean grain and return elevators, coal preparation, construction equipment, conveyors, cotton tramper, dairy handling, fertilizer conveying, flight conveyors, food processing, forest products, grain handling, heavy duty conveyors, high-temperature industrial ovens, jack ladder, log handling, material handling, meat packing, mining, overhead conveyors, power drives, produce washdown, pulp and paper, recycling, refineries, roofing plants, rubber manufacturing, stackers, steel mills, sugar harvesting, sugar processing, trolle, conveyors, utilities, water treatment
| Material |
Alloy steel |
| Process |
Assembled |
| Heat treatment |
Case hardening, Meshbeltfurnace quenching heat treatment |
| Surface treatment |
Blackened, Zinc galvanized, Nickel galvanized, Chroming, Colour Painting, or as per customer’s request |
| Performance |
High precision, high wear resistance, low noise, smooth and steady, high strength |
| Model number |
X348, X458, 468H, X678, 698, 698H, F100x16, F100x17, F160x24 |
| Packaging |
Plastic bag ,carton box ,plywood case or customer requirement. |
Shipping Cost:
Estimated freight per unit.
|
To be negotiated
|
| Usage: |
Transmission Chain, Drag Chain, Dedicated Special Chain, Transportation Chain |
| Material: |
Steel |
| Color: |
Solid Color |
| Customization: |
Available
|
Customized Request
|
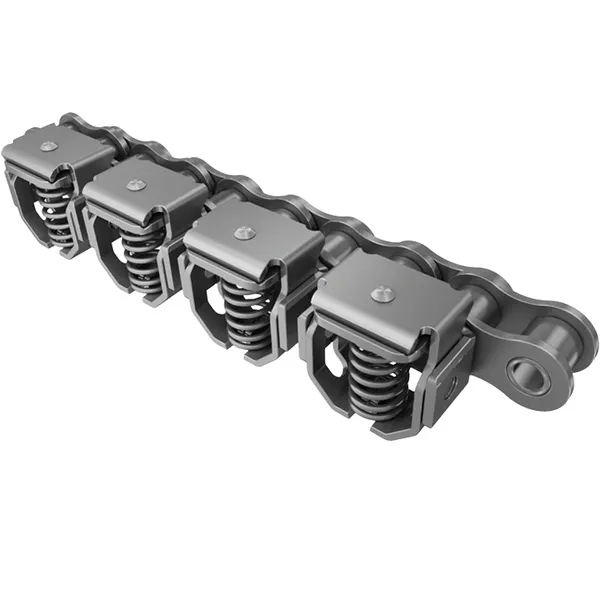
What are the benefits of using a self-lubricating conveyor chain?
Self-lubricating conveyor chains offer several advantages over traditional lubricated chains. Here are some key benefits:
1. Reduced Maintenance: Self-lubricating chains eliminate the need for regular lubrication, reducing the time and effort required for maintenance. This is particularly beneficial in applications where access to the chain is difficult or time-consuming.
2. Cost Savings: By eliminating the need for external lubrication, self-lubricating chains can help reduce lubrication costs over the lifetime of the chain. This includes the cost of lubricants, as well as the labor and equipment required for lubrication maintenance.
3. Clean and Environmentally Friendly: Self-lubricating chains do not require external lubricants, resulting in a cleaner working environment. There is no risk of lubricant spills or contamination of the surrounding area, making them ideal for applications that require strict cleanliness standards, such as food processing or pharmaceutical industries.
4. Extended Chain Life: Self-lubricating chains are designed with built-in lubrication systems that provide a continuous and controlled supply of lubricant to the chain components. This helps reduce friction, wear, and heat generation, resulting in longer chain life and improved performance.
5. Improved Reliability: With consistent and reliable lubrication, self-lubricating chains maintain optimal performance and minimize the risk of chain failure or breakdown. They are less susceptible to premature wear, elongation, and corrosion, ensuring a more reliable and efficient conveyor system.
It’s important to note that the specific benefits of self-lubricating chains may vary depending on the manufacturer and the design of the chain. It’s recommended to consult with the chain manufacturer or an industry expert to understand the suitability and advantages of self-lubricating chains for a particular application.
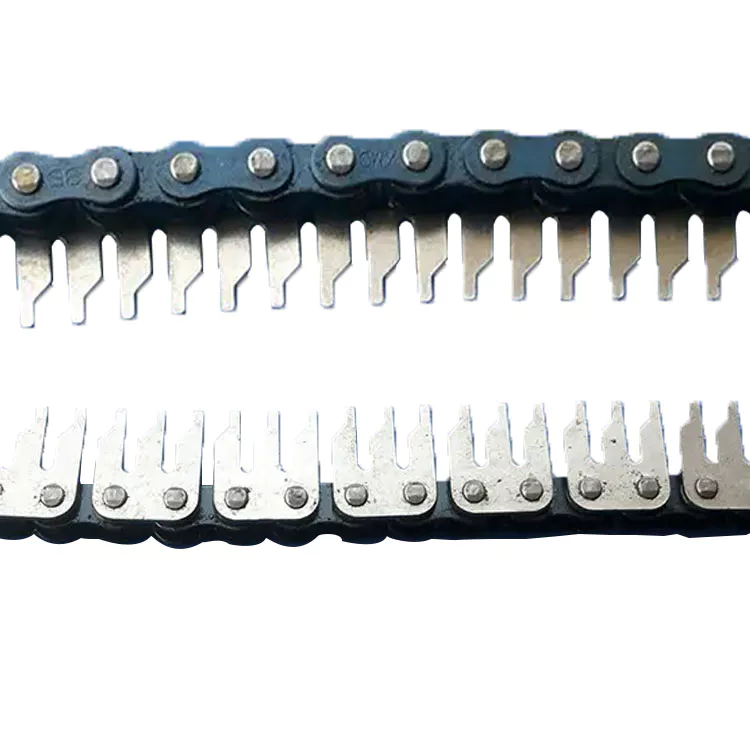
Can a conveyor chain be used in food processing applications?
Yes, a conveyor chain can be used in food processing applications. Conveyor chains play a crucial role in the efficient and hygienic handling of food products throughout the production process. Here are some key points to consider:
1. Food-Grade Materials: Conveyor chains used in food processing applications are typically made from food-grade materials such as stainless steel or plastic. These materials are corrosion-resistant, easy to clean, and comply with food safety regulations.
2. Hygiene Considerations: Food processing environments require high standards of hygiene. Conveyor chains designed for food applications incorporate features such as smooth surfaces, open link designs, and easy disassembly for thorough cleaning. They may also have specialized coatings or treatments to prevent bacterial growth.
3. Sanitary Design: Conveyor chains for food processing applications are designed with minimal crevices or joints to prevent food particles from getting trapped. They may have self-draining capabilities to remove excess fluids or debris.
4. Product Integrity: Conveyor chains in food processing applications ensure gentle handling of delicate food products to avoid damage or contamination. They can be equipped with accessories like cleats, side guards, or modular belt systems to securely hold and transport items of various shapes and sizes.
5. High Temperature and Washdown Capabilities: Some food processing applications require conveyor chains to withstand high temperatures during cooking, baking, or sterilization processes. Specialized chains with heat-resistant materials or coatings are available. Additionally, conveyor chains used in food processing should be capable of withstanding frequent washdowns and cleaning with water or cleaning agents.
6. Compliance with Standards: Conveyor chains used in food processing applications must comply with industry-specific standards such as FDA (Food and Drug Administration) regulations, HACCP (Hazard Analysis Critical Control Point) guidelines, and other food safety certifications.
When selecting a conveyor chain for food processing applications, it is important to consider the specific requirements of the production line, including the type of food being handled, the operating conditions, and the necessary sanitary standards. Proper maintenance and regular cleaning protocols should also be implemented to ensure food safety and product integrity.
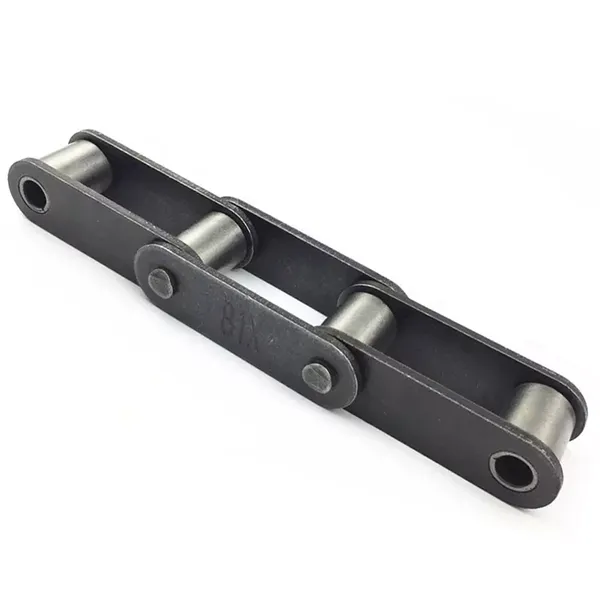
What industries commonly use conveyor chains?
Conveyor chains are widely used in various industries for efficient material handling and transportation. Here are some of the industries commonly using conveyor chains:
- Manufacturing: Conveyor chains are extensively used in manufacturing industries such as automotive, electronics, appliances, and machinery. They facilitate the movement of components, parts, and finished products along assembly lines.
- Food and Beverage: The food and beverage industry relies heavily on conveyor chains for conveying and processing food products, including packaging, sorting, and distribution. Conveyor chains in this industry often have specific requirements such as sanitary design and resistance to contaminants.
- Logistics and Warehousing: Conveyor chains are integral to logistics and warehousing operations for efficient handling of goods, including sorting, loading, unloading, and distribution. They are commonly used in distribution centers, airports, and postal facilities.
- Mining and Quarrying: Conveyor chains play a crucial role in mining and quarrying operations by transporting bulk materials such as coal, ore, gravel, and aggregates. They are designed to withstand heavy loads and harsh environments.
- Agriculture: In the agricultural sector, conveyor chains are used for handling crops, grains, seeds, and livestock feed. They are employed in processing plants, grain elevators, and animal feed production facilities.
- Automotive: The automotive industry extensively uses conveyor chains in assembly plants for transporting vehicle components, body frames, engines, and other parts throughout the production process.
- Pharmaceutical and Healthcare: Conveyor chains are utilized in pharmaceutical and healthcare facilities for the automated movement of medical supplies, pharmaceutical products, and laboratory specimens.
- Chemical and Petrochemical: Conveyor chains are employed in chemical and petrochemical industries for the handling of hazardous materials, bulk chemicals, and raw materials during production and storage.
- Construction and Building Materials: Conveyor chains are used in construction sites and building material production facilities for conveying materials such as cement, bricks, aggregates, and roofing materials.
These are just a few examples, and conveyor chains are also utilized in many other industries where efficient material handling and transportation are essential for the production and distribution processes.


editor by CX 2023-09-07
 English
























