Mô tả sản phẩm
| Model NO. | 06C/08A/10A/12A/16A/20A/24A/28A/32A/40A/06B/08B/10B/12B/16B/20B/24B/28B/32B/40B-1/2/3 Heavy duty |
| Chain Model | Roller Chains |
| Structure (for Chain) | Xích con lăn |
| Thông số kỹ thuật | GB/T, DIN, ANSI, ISO, BS, JIS. |
| Origin | HangZhou, ZheJiang |
| Color | Solid Color |
| Chain Color | Customized |
Our company
Wolff Chain Co. is 1 of the professional chain manufacturers in China. We focus on reseaching, manufacturing and trading of the chain drive with famous brands — “DOVON” and “DECHO”. We supply OEM services for many famous enterprises such as SUZUKI, XIHU (WEST LAKE) DIS., FAW, AGCO, JUMING as well.
Wolff mainly producing the Transmission chains,Conveyor chains,Dragging Chains,Silent chains,Leaf chains,Roller chains,Special chain and many other series of chain products. Our technicians a have improved the chains quality to the world-level. High quality material selection, powerful and precise heat-treatment technology and excellent assembly methods ensure Wolff chains meet the tough and strict requirements for machines and vehicles.
All of our products completely conform to the international standard such as ISO\DIN\ANSI\BS\JIS, etc. Wolff has been successfully certified by ISO9001 Quality Management System,SGS inspection and BV inspection. Wolff chains can be widely applied to many industries including automobile, motorcycle, forklift, wood processing machine, constructure machine, packing machine, food machine,tobacco machine and agricultural equipments. Wolff chains are popular in America,South America,Europe,Middle East, South East Asia and Africa markets.
Xưởng của chúng tôi
Our certification
Welcome to our exhibition
Câu hỏi thường gặp
Q1. What is your terms of packing?
A: Thông thường, chúng tôi đóng gói hàng hóa trong hộp màu đơn sắc. Nếu bạn có yêu cầu đặc biệt về đóng gói, vui lòng thương lượng trước với chúng tôi, chúng tôi có thể đóng gói hàng hóa theo yêu cầu của bạn.
Câu 2. Điều khoản thanh toán của bạn là gì?
A: Thanh toán đặt cọc 30% bằng chuyển khoản ngân hàng (T/T), và 70% trước khi giao hàng. Chúng tôi sẽ gửi ảnh sản phẩm và bao bì cho bạn xem.
Trước khi bạn thanh toán số tiền còn lại. Về các điều khoản thanh toán khác, vui lòng thương lượng trước với chúng tôi, chúng ta có thể thảo luận thêm.
Câu 3. Điều khoản giao hàng của bạn là gì?
A: EXW, FOB, CFR, CIF.
Câu 4. Thời gian giao hàng của bạn như thế nào?
A: Thông thường, sẽ mất từ 25 đến 30 ngày sau khi nhận được tiền đặt cọc. Thời gian giao hàng cụ thể phụ thuộc vào...
Về các mặt hàng và số lượng đơn đặt hàng của bạn.
Câu 5. Bạn có thể sản xuất theo mẫu không?
A: Vâng, chúng tôi có thể sản xuất theo mẫu hoặc bản vẽ kỹ thuật của bạn. Chúng tôi có thể chế tạo khuôn và đồ gá.
Câu 6. Chính sách mẫu của bạn là gì?
A: Chúng tôi có thể cung cấp mẫu nếu có sẵn linh kiện trong kho, nhưng khách hàng phải trả phí mẫu và phí vận chuyển.
Chi phí vận chuyển. Chúng tôi hoan nghênh đơn đặt hàng mẫu.
Câu 7. Bạn có kiểm tra tất cả hàng hóa trước khi giao hàng không?
A: Vâng, chúng tôi có bài kiểm tra 100% trước khi giao hàng.
Câu 8: Làm thế nào để chúng ta xây dựng mối quan hệ kinh doanh lâu dài và tốt đẹp?
1. Chúng tôi duy trì chất lượng tốt và giá cả cạnh tranh để đảm bảo lợi ích cho khách hàng;
2. Chúng tôi tôn trọng mọi khách hàng như những người bạn và chúng tôi chân thành kinh doanh cũng như kết bạn với họ.
Bất kể họ đến từ đâu.
| Standard or Nonstandard: | Standard |
|---|---|
| Ứng dụng: | Textile Machinery, Garment Machinery, Conveyer Equipment, Packaging Machinery, Food Machinery, Marine, Mining Equipment |
| Xử lý bề mặt: | Tinh dầu nở hoa |
| Kết cấu: | Xích con lăn |
| Vật liệu: | Carbon Steel |
| Type: | Short Pitch Chain |
| Mẫu: |
US$ 0/Mảnh
1 chiếc (Số lượng đặt tối thiểu) | |
|---|
| Tùy chỉnh: |
Có sẵn
| Yêu cầu tùy chỉnh |
|---|
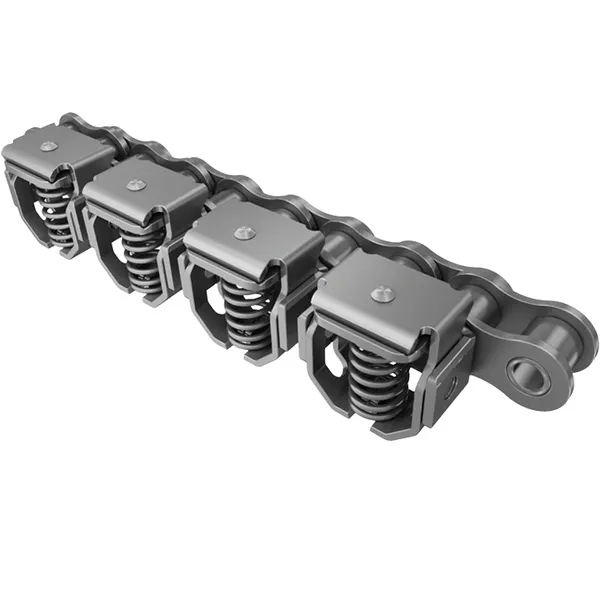
What are the benefits of using an overhead conveyor chain system?
Using an overhead conveyor chain system offers several benefits in various industrial applications. Here are some key advantages:
1. Space Optimization:
– Overhead conveyor chain systems utilize the vertical space, allowing efficient utilization of floor space. This is especially beneficial in facilities with limited floor area, as it enables efficient material handling and production flow without obstructing the work area.
2. Flexibility and Versatility:
– Overhead conveyor chains offer flexibility in routing and can be customized to fit the specific layout requirements of the facility. They can traverse different areas, including assembly lines, paint booths, storage areas, and more. The versatility of overhead systems allows for efficient and adaptable material movement.
3. Improved Safety:
– Overhead conveyor chains minimize ground-level obstructions, reducing the risk of tripping hazards and accidents. Operators and workers can safely navigate the work area without interference from the conveyor system.
4. Bảo vệ sản phẩm:
– Overhead conveyor chains provide better protection for the products being transported. By keeping the products elevated and away from potential hazards on the floor, such as dust, debris, or spills, the risk of product damage or contamination is reduced.
5. Increased Efficiency:
– Overhead conveyor systems can enhance production efficiency by facilitating continuous material flow and reducing manual handling. They enable automated loading and unloading of materials, leading to faster processing times and improved overall productivity.
6. Easy Maintenance:
– Overhead conveyor chains are typically designed for easy maintenance. Components such as chains, trolleys, and drives can be accessed and serviced conveniently, minimizing downtime and maintenance costs.
7. Customization and Integration:
– Overhead conveyor chains can be tailored to meet specific application requirements, including load capacity, speed, and control systems. They can also be integrated with other automated systems, such as robotic workstations or sorting mechanisms, to further optimize the material handling process.
Overall, using an overhead conveyor chain system provides efficient material handling, maximizes space utilization, enhances safety, and improves productivity in industrial environments.
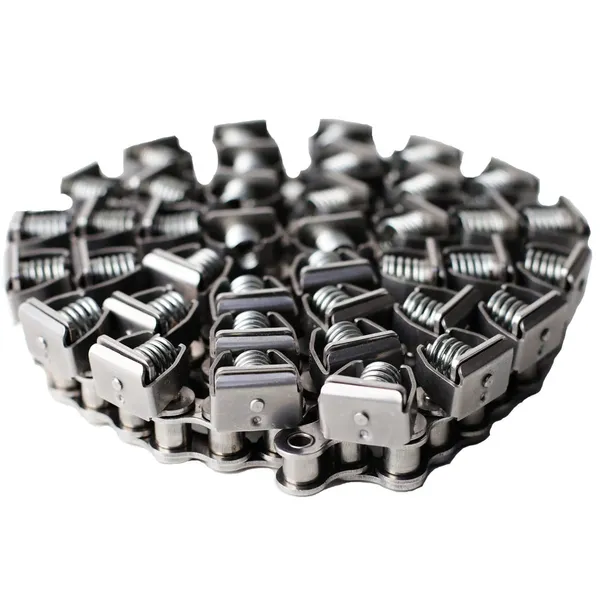
How do you calculate the power requirements for a conveyor chain?
Calculating the power requirements for a conveyor chain involves considering various factors. Here’s a step-by-step process:
1. Determine the total weight to be transported: Measure or estimate the total weight of the material or product that will be carried by the conveyor chain. This includes the weight of the product itself, any packaging, and additional loads.
2. Determine the speed of the conveyor: Determine the desired speed at which the conveyor chain will operate. This is typically measured in feet per minute (FPM) or meters per second (m/s).
3. Calculate the required capacity: Multiply the total weight by the desired speed to determine the required capacity of the conveyor system. This will give you the weight per unit of time (e.g., pounds per minute or kilograms per hour).
4. Consider the conveyor’s design factors: Take into account various design factors such as the type and pitch of the conveyor chain, the coefficient of friction between the chain and the conveyor components, and any incline or decline angles of the conveyor system. These factors affect the power requirements.
5. Determine the required power: Use the following formula to calculate the power requirements:
Power (in horsepower) = (Capacity × Friction Factor) ÷ (33,000 × Efficiency)
Where:
– Capacity is the weight per unit of time (from step 3)
– Friction Factor is the ratio of chain tension to chain weight, taking into account the design factors
– 33,000 is a conversion factor to convert the units to horsepower
– Efficiency is the overall efficiency of the conveyor system, typically expressed as a decimal value (e.g., 0.95 for 95% efficiency)
6. Select a suitable motor: Based on the calculated power requirements, select a motor that can provide the necessary power to drive the conveyor chain. Consider factors such as motor type, motor efficiency, and overload capacity.
It’s important to note that the power requirements may vary depending on specific conveyor system designs and operating conditions. Consulting with a qualified engineer or conveyor manufacturer is recommended to ensure accurate calculations and proper motor selection.
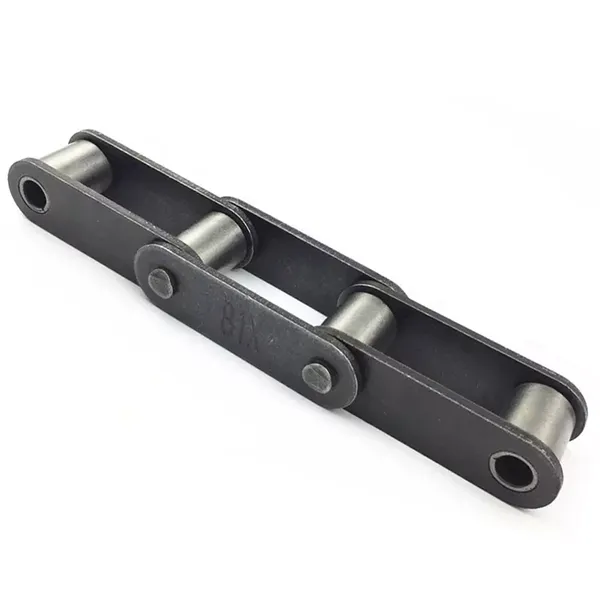
What industries commonly use conveyor chains?
Conveyor chains are widely used in various industries for efficient material handling and transportation. Here are some of the industries commonly using conveyor chains:
- Manufacturing: Conveyor chains are extensively used in manufacturing industries such as automotive, electronics, appliances, and machinery. They facilitate the movement of components, parts, and finished products along assembly lines.
- Food and Beverage: The food and beverage industry relies heavily on conveyor chains for conveying and processing food products, including packaging, sorting, and distribution. Conveyor chains in this industry often have specific requirements such as sanitary design and resistance to contaminants.
- Logistics and Warehousing: Conveyor chains are integral to logistics and warehousing operations for efficient handling of goods, including sorting, loading, unloading, and distribution. They are commonly used in distribution centers, airports, and postal facilities.
- Mining and Quarrying: Conveyor chains play a crucial role in mining and quarrying operations by transporting bulk materials such as coal, ore, gravel, and aggregates. They are designed to withstand heavy loads and harsh environments.
- Agriculture: In the agricultural sector, conveyor chains are used for handling crops, grains, seeds, and livestock feed. They are employed in processing plants, grain elevators, and animal feed production facilities.
- Automotive: The automotive industry extensively uses conveyor chains in assembly plants for transporting vehicle components, body frames, engines, and other parts throughout the production process.
- Pharmaceutical and Healthcare: Conveyor chains are utilized in pharmaceutical and healthcare facilities for the automated movement of medical supplies, pharmaceutical products, and laboratory specimens.
- Chemical and Petrochemical: Conveyor chains are employed in chemical and petrochemical industries for the handling of hazardous materials, bulk chemicals, and raw materials during production and storage.
- Construction and Building Materials: Conveyor chains are used in construction sites and building material production facilities for conveying materials such as cement, bricks, aggregates, and roofing materials.
These are just a few examples, and conveyor chains are also utilized in many other industries where efficient material handling and transportation are essential for the production and distribution processes.


editor by CX 2023-08-09

























