பதிவு வடிவியல்
பிட்ச், அகலம், ரோலர்/புஷ், பின், பிளேட், ஒட்டுமொத்த அகலம் மற்றும் இணைப்பு முறை.
பேக்கரி சங்கிலி தொழில்நுட்ப வழிகாட்டி
Hollow Pin Chains in Bakery Proofers is best answered by combining measured chain geometry, machine duty and the operating environment. This guide shows what to inspect, record and discuss before a replacement or new-chain decision.
Hollow Pin Chains in Bakery Proofers should be evaluated from the actual conveyor. Start with chain pitch, transverse geometry, sprocket condition and any carrier attachment, then add temperature, moisture, washdown, load, speed and take-up information. The objective is not to identify a chain by appearance; it is to produce an RFQ that preserves the machine interface and makes application-dependent choices explicit.
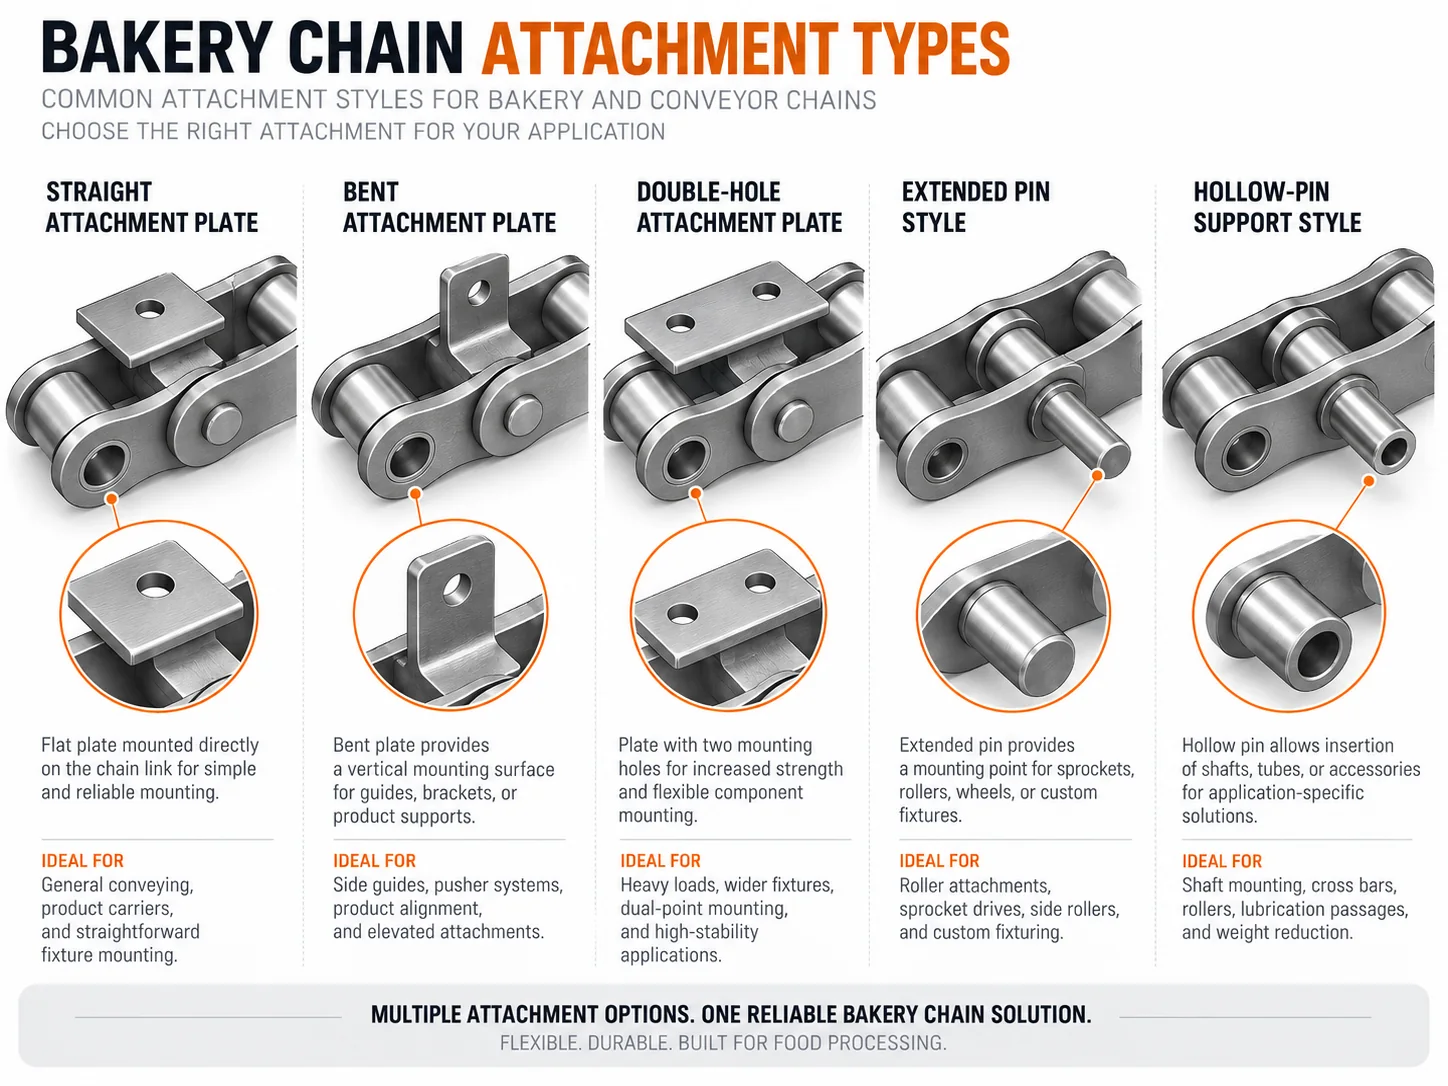
சங்கிலியை அகற்றுவதற்கு முன் பல பண்புகளை அளவிடவும். பிட்ச் அடிப்படை பற்சக்கர உறவைக் குறிப்பிடுகிறது, ஆனால் உட்புற அகலம், ரோலர் அல்லது புஷ் விட்டம், பின் விட்டம், பிளேட் உயரம், ஒட்டுமொத்த அகலம் மற்றும் இணைப்புப் பரிமாணங்கள் ஆகியவை ஒரே பெயரளவு பிட்சைப் பகிர்ந்து கொள்ளக்கூடிய உள்ளமைப்புகளை வேறுபடுத்துகின்றன.
தேய்ந்த இழைக்கு, பல இணைப்புகளில் உள்ள மொத்தப் பிட்சை அளவிடவும். சங்கிலியைப் பக்கவாட்டிலிருந்தும் முனையிலிருந்தும் புகைப்படம் எடுக்கவும், இயன்ற இடங்களில் ஸ்ப்ராக்கெட்டையும் அதில் சேர்க்கவும்.
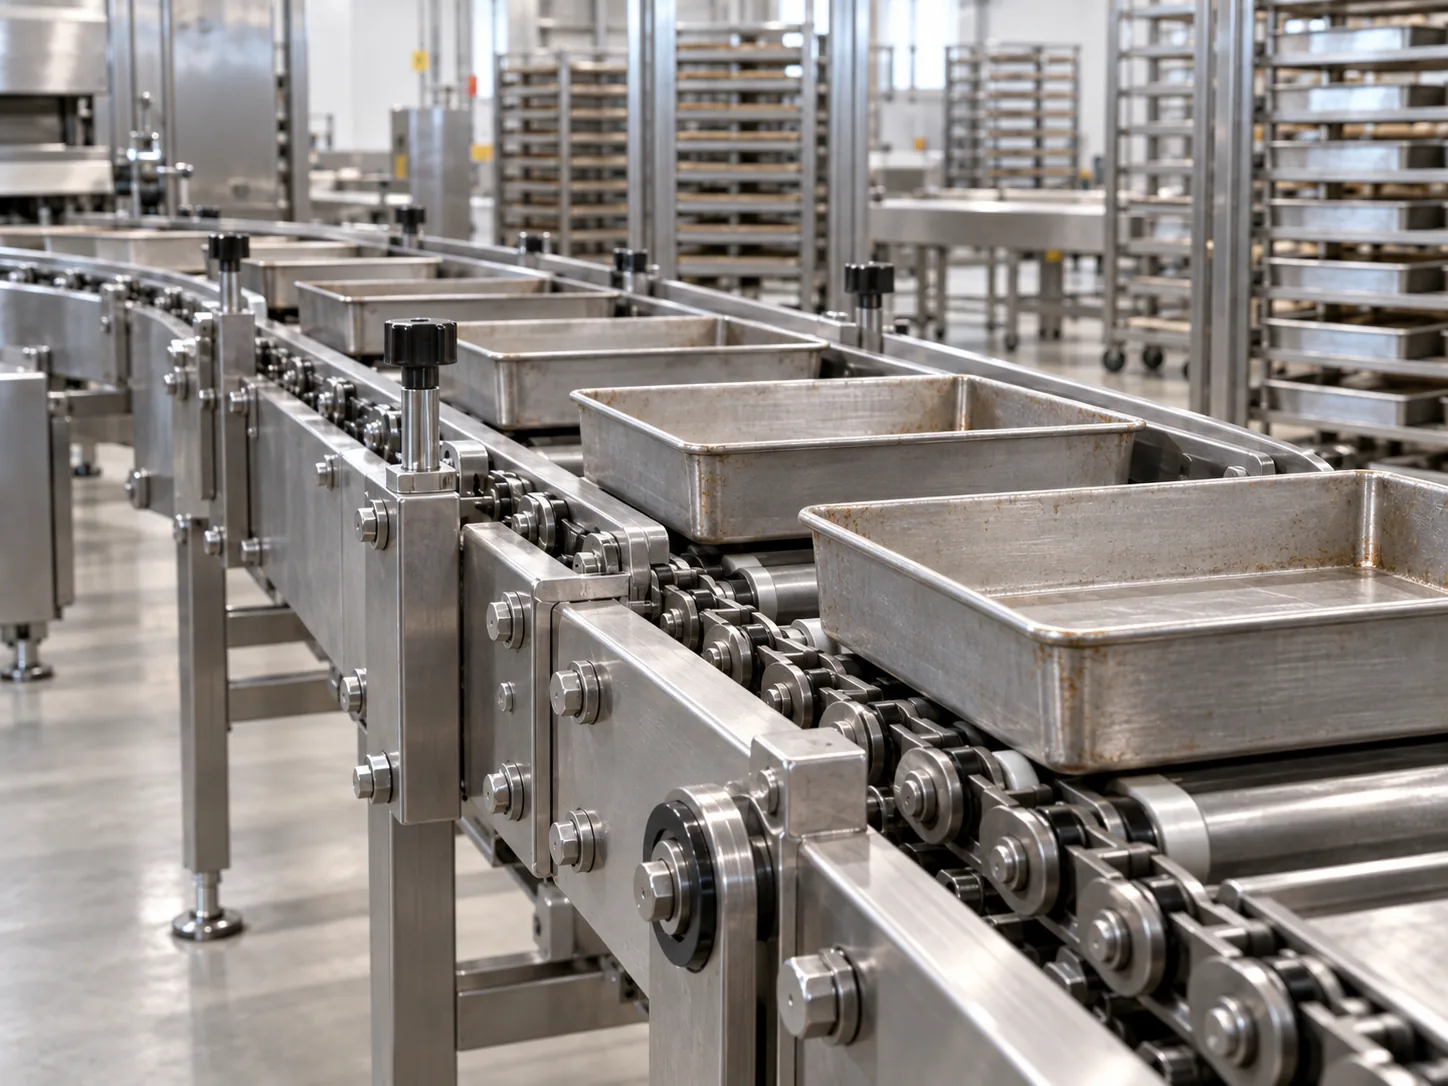
The same chain geometry can behave differently in a humid proofer, a hot oven, an ambient cooling section or a washdown area. For hollow pin chains in bakery proofers, document the exact machine zone, whether the chain carries product directly or moves pans/fixtures, and whether the joint sees heat, moisture, cleaning chemicals or abrasive residue.
செயல்முறைத் தரவு, எந்தப் பண்புகள் பரிமாற்றத்தன்மையால் நிர்ணயிக்கப்பட்டவை என்பதையும், மூலப்பொருள், இடைவெளி அல்லது இணைப்பு உற்பத்தி முறை போன்ற எந்தப் பண்புகள் பயன்பாட்டிற்காக மதிப்பாய்வு செய்யப்பட வேண்டும் என்பதையும் தீர்மானிக்க உதவுகிறது.

ஒரு சங்கிலி தனித்து இயங்குவதில்லை. உருளைகள் அல்லது புஷ்கள் ஸ்ப்ராக்கெட் பற்களுக்கு இடையேயான இடைவெளிகளில் சீராக நுழைந்து வெளியேற வேண்டும், அதே நேரத்தில் வழிகாட்டித் தடங்கள் சங்கிலி இழையைப் பக்கவாட்டில் தள்ளாமல் தாங்க வேண்டும். வளைந்த பற்கள், ஷாஃப்ட்டின் சீரற்ற அமைப்பு, மையத்திலிருந்து விலகிய ஸ்ப்ராக்கெட்டுகள் அல்லது இறுக்கமான வழிகாட்டி போன்றவை ஒரு புதிய சங்கிலி விரைவாகத் தேய்ந்துபோகக் காரணமாகலாம்.
ஒரு முழுச் சுற்று வழியாக முழுப் பாதையையும் ஆய்வு செய்யவும். அதே இயந்திர இடத்தில் சேதம் மீண்டும் ஏற்பட்டால், தொடர் அமைப்பே பழுதடைந்தது என்று கருதுவதற்கு முன்பு, உள்ளூர் ஆதரவு, பரிமாற்றம் அல்லது கேரியரை விசாரிக்கவும்.
பிட்ச், அகலம், ரோலர்/புஷ், பின், பிளேட், ஒட்டுமொத்த அகலம் மற்றும் இணைப்பு முறை.
வெப்பநிலை, ஈரப்பதம், கழுவுதல், வேகம், சுமை, உற்பத்தி நேரங்கள் மற்றும் தொடக்கங்கள்.
பற்சக்கரங்கள், வழிகாட்டிகள், சங்கிலி மையங்கள், இழுவிசை, சீரமைப்பு மற்றும் கேரியர் இடைவெளிகள்.
நிறுவுவதற்கு முன், இறுதியாக ஆர்டர் செய்யப்பட்ட வடிவம், பொருள் மற்றும் பயன்பாட்டைச் சார்ந்த உள்ளமைப்பிற்கு ஒப்புதல் அளியுங்கள்.
பிரச்சனை தோன்றுவதற்கு முன்பு என்னென்ன மாற்றங்கள் நிகழ்ந்தன என்று கேளுங்கள்: உற்பத்தி விகிதம், பொருள் அல்லது தட்டின் எடை, சுத்தம் செய்யும் சுழற்சி, மசகு எண்ணெய், வெப்பநிலை, பராமரிப்பு இடைவெளி அல்லது மாற்றப்பட்ட பற்சக்கரங்கள். தேய்மானம் சீராக உள்ளதா அல்லது ஒரு குறிப்பிட்ட இடத்தில் குவிந்துள்ளதா என்பதைக் காட்டுவதால், ஒரு தனிப் புகைப்படத்தை விடப் போக்கு குறித்த தகவல்கள் அதிக மதிப்பு வாய்ந்தவை.
வழக்கமான ஆய்வின்போது, இறுக்கமான இணைப்புகள், ரோலர் தேய்மானம், பின் அசைவு, விரிசல் விட்ட அல்லது வளைந்த இணைப்புகள், இயல்புக்கு மாறான பக்கவாட்டுத் தொடர்பு மற்றும் சீரற்ற இழுவை ஆகியவற்றைக் கவனிக்கவும். இயந்திர உரிமையாளரின் தேவைகளுக்கு ஏற்ப பாதுகாப்பு உறைகளையும் பாதுகாப்பு நடைமுறைகளையும் பராமரிக்கவும்.
அளவிடப்பட்ட பரிமாணங்கள், இயந்திரம்/செயல்முறையின் பெயர், புகைப்படங்கள், வரைபடம் (கிடைத்தால்), அளவு அல்லது தேவையான சங்கிலியின் நீளம், இணைப்பு இடைவெளி, சங்கிலி-மைய இடைவெளி, பற்சக்கரத் தகவல், வெப்பநிலை, கழுவும் நிலை, சுமை மற்றும் இலக்கு விநியோகக் காலம் ஆகியவற்றைச் சேர்க்கவும். மதிப்பாய்வு செய்யவும். பேக்கரி சங்கிலி தேர்வு வழிகாட்டி மற்றும் அந்த தயாரிப்பு-குடும்ப மேலோட்டங்கள் அடுத்த முடிவெடுக்கும் கட்டத்திற்காக.
A useful diagnosis starts with evidence that can be repeated by a second person. using hollow pins as a controlled interface for cross rods and product carriers. Record pin bore, cross-rod diameter, strand center distance, retention method and carrier width. When the chain is worn, note which readings may be influenced by joint clearance or deformation, and prefer multi-pitch or multi-point measurements over one isolated dimension.
The chain does not operate by itself. In proofers using cross bars, removable carriers or parallel chain strands, inspect the sprockets, guides, return path, take-up and carrier interface at the same time. The symptom to watch is cross-rod binding, unequal strand load or restricted articulation. A local problem that repeats at one machine position often points to alignment, clearance or mating-hardware issues rather than a uniform chain problem.
The practical decision is to treat the rod-and-pin connection as part of the load path, not just a convenient mounting hole. That prevents a common error: changing chain tension, material or size before the root constraint has been identified. Use the chain drawing and the machine envelope together, because a configuration that looks correct in isolation can still interfere with a guard, transfer plate, sensor bracket or carrier.
“சூடான,” “ஈரமான” அல்லது “உணவுத் தரம் வாய்ந்த” போன்ற ஒற்றைப் பெயரடையைக் கொண்டு விவரிக்காமல், இயக்கச் சுழற்சியை விவரிக்கவும். பொருத்தமான இடங்களில் இயல்பான மற்றும் உச்சபட்ச வெப்பநிலை, ஈரப்பதம் அல்லது சுத்தம் செய்யும் வெளிப்பாடு, வேகம், தொடங்குதல்/நிறுத்துதல் செயல்பாடு மற்றும் உயவு வரம்புகள் ஆகியவற்றைக் குறிப்பிடவும். அடிப்படை வடிவியல் மாறாமல் இருக்கும்போது, இடைவெளிகள், பொருட்கள் அல்லது பராமரிப்பு நடைமுறைகளை மாற்ற வேண்டுமா என்பதை இந்த விவரங்கள் தீர்மானிக்கின்றன.
| சரிபார்க்கவும் | அது ஏன் முக்கியம் | எதை அனுப்ப வேண்டும் அல்லது சரிபார்க்க வேண்டும் |
|---|---|---|
| அடையாளம் | Confirm pin bore, cross-rod diameter, strand center distance, retention method and carrier width. Use a measurement sequence that can be repeated after removal so the installed and bench readings can be compared. | பரிமாண வரைபடம், அளவைக் காட்டும் புகைப்படங்கள் மற்றும் ஏதேனும் பழைய வரைபடம் அல்லது பாக எண். |
| வழித்தட நிலை | Map where the chain runs through proofers using cross bars, removable carriers or parallel chain strands. Mark the exact location of cross-rod binding, unequal strand load or restricted articulation instead of reporting the condition only as a whole-line problem. | கன்வேயர் பிரிவு, இயக்கி/வால் நிலைகள் மற்றும் திரும்பும் பாதையைக் காட்டும் சூழல் புகைப்படம். |
| இணையும் பாகங்கள் | பல்லின் வடிவம், ரோலர் பொருந்துதல், ஷாஃப்ட்/ஸ்ப்ராக்கெட் சீரமைப்பு, கைடு தொடர்பு மற்றும் டேக்-அப் ரிசர்வ் ஆகியவற்றை ஆய்வு செய்யவும். இந்தப் பாகங்கள், செயின்-செலக்டிவ் சிக்கலைப் போன்ற தேய்மான வடிவங்களை உருவாக்கக்கூடும். | ஸ்ப்ராக்கெட் பற்களின் எண்ணிக்கை மற்றும் புகைப்படங்கள், கைடு அமைப்பு மற்றும் தற்போதைய டேக்-அப் நிலை. |
| சுமை பாதை | Identify how product carriers, pans, rods or fixtures transfer load into the chain. For this topic, the key focus is using hollow pins as a controlled interface for cross rods and product carriers. | தாங்கி வரைபடம், இணைப்பு இடைவெளி, சங்கிலி மைய இடைவெளி மற்றும் தாங்கப்படும் நிறை/விசை (தெரிந்த இடங்களில்). |
| சுற்றுச்சூழல் | இயந்திரப் பகுதி வாரியாக வெப்பநிலை, ஈரப்பதம், கழுவுதல், மாசுபடுதல் மற்றும் மசகு எண்ணெய் கட்டுப்பாடுகளைப் பதிவு செய்யவும். தொடர்ச்சியான வெளிப்பாட்டை, குறுகிய உச்சநிலைகள் அல்லது சுத்தம் செய்யும் நிகழ்வுகளிலிருந்து பிரிக்கவும். | இயக்க நிலைச் சுருக்கம் மற்றும் பராமரிப்பு/மசகு நடைமுறை. |
| வெளியீடு | The final engineering action is to treat the rod-and-pin connection as part of the load path, not just a convenient mounting hole. The approved drawing should distinguish fixed interchange dimensions from selectable options. | hollow-pin dimensions, rod detail, strand spacing, carrier mass and cleaning routine. |
A uniform change along the whole strand suggests a different mechanism from damage concentrated at one sprocket, guide or transfer. For Hollow Pin Chains in Bakery Proofers, compare left/right sides and loaded/return paths. The distribution of wear can reveal whether the driver is joint wear, side loading, contamination, thermal change or a carrier that is forcing the chain out of its natural path.
Increasing tension can temporarily change noise or tracking without correcting the underlying cause. If the observed issue is cross-rod binding, unequal strand load or restricted articulation, first confirm alignment, take-up geometry and articulation. Excessive tension can add bearing load and make a marginal guide or attachment problem worse.
பேக்கரி உபகரணங்கள் உற்பத்தி, சுத்தம் செய்தல் மற்றும் நிறுத்தம் ஆகிய நிலைகளுக்கு இடையில் இயங்கக்கூடும். ஒரு சங்கிலி குளிர்ச்சியாக இருக்கும்போது சாதாரணமாக இயங்கி, சூடாக்கப்படும்போது இறுக்கமாகலாம்; அல்லது உற்பத்தியின்போது தடையின்றி இயங்கி, மீண்டும் மீண்டும் ஈரமான நிறுத்தங்களுக்குப் பிறகு அரிப்புக்குள்ளாகலாம். அறிகுறி ஏற்படும் நிலையைப் பதிவு செய்யவும், அப்போதுதான் தேர்ந்தெடுக்கப்பட்ட சரிசெய்யும் நடவடிக்கை உண்மையான பணிச் சுழற்சியைக் கையாளும்.
For an unknown chain, one close-up is not enough. Pair a complete machine-zone image with side and end views of several pitches, a sprocket-engagement photo and a clear attachment/carrier view. Place a scale only where it does not hide the feature being measured. This photo set makes using hollow pins as a controlled interface for cross rods and product carriers easier to evaluate remotely.
Record pin bore, cross-rod diameter, strand center distance, retention method and carrier width, chain centers, sprocket tooth count and the carrier interface before changing components.
Describe what happens in proofers using cross bars, removable carriers or parallel chain strands, including temperature or moisture changes, speed, load and cleaning/lubrication constraints.
Document where cross-rod binding, unequal strand load or restricted articulation appears. Compare drive, tail, loaded run, return run and transfer points rather than averaging the entire conveyor.
Include hollow-pin dimensions, rod detail, strand spacing, carrier mass and cleaning routine. State the required quantity or chain length and any documentation needed with the order.
Review pitch, widths, pin/roller geometry, attachments and material notes on one controlled drawing revision. For Hollow Pin Chains in Bakery Proofers, the release decision should explicitly address using hollow pins as a controlled interface for cross rods and product carriers.
நிறுவிய பிறகு, குறைந்தபட்சம் ஒரு முழுச் சுற்றைக் கவனிக்கவும், ஸ்ப்ராக்கெட் நுழைவு/வெளியேற்றம் மற்றும் கேரியர் இடைவெளியைச் சரிபார்க்கவும், மேலும் இயந்திர உற்பத்தியாளரின் நடைமுறைப்படி டேக்-அப்பை மீண்டும் சரிபார்க்கவும். தேய்ந்த அல்லது தவறாகப் பொருத்தப்பட்ட பாகங்களை ஈடுசெய்ய புதிய சங்கிலியைப் பயன்படுத்தக் கூடாது.
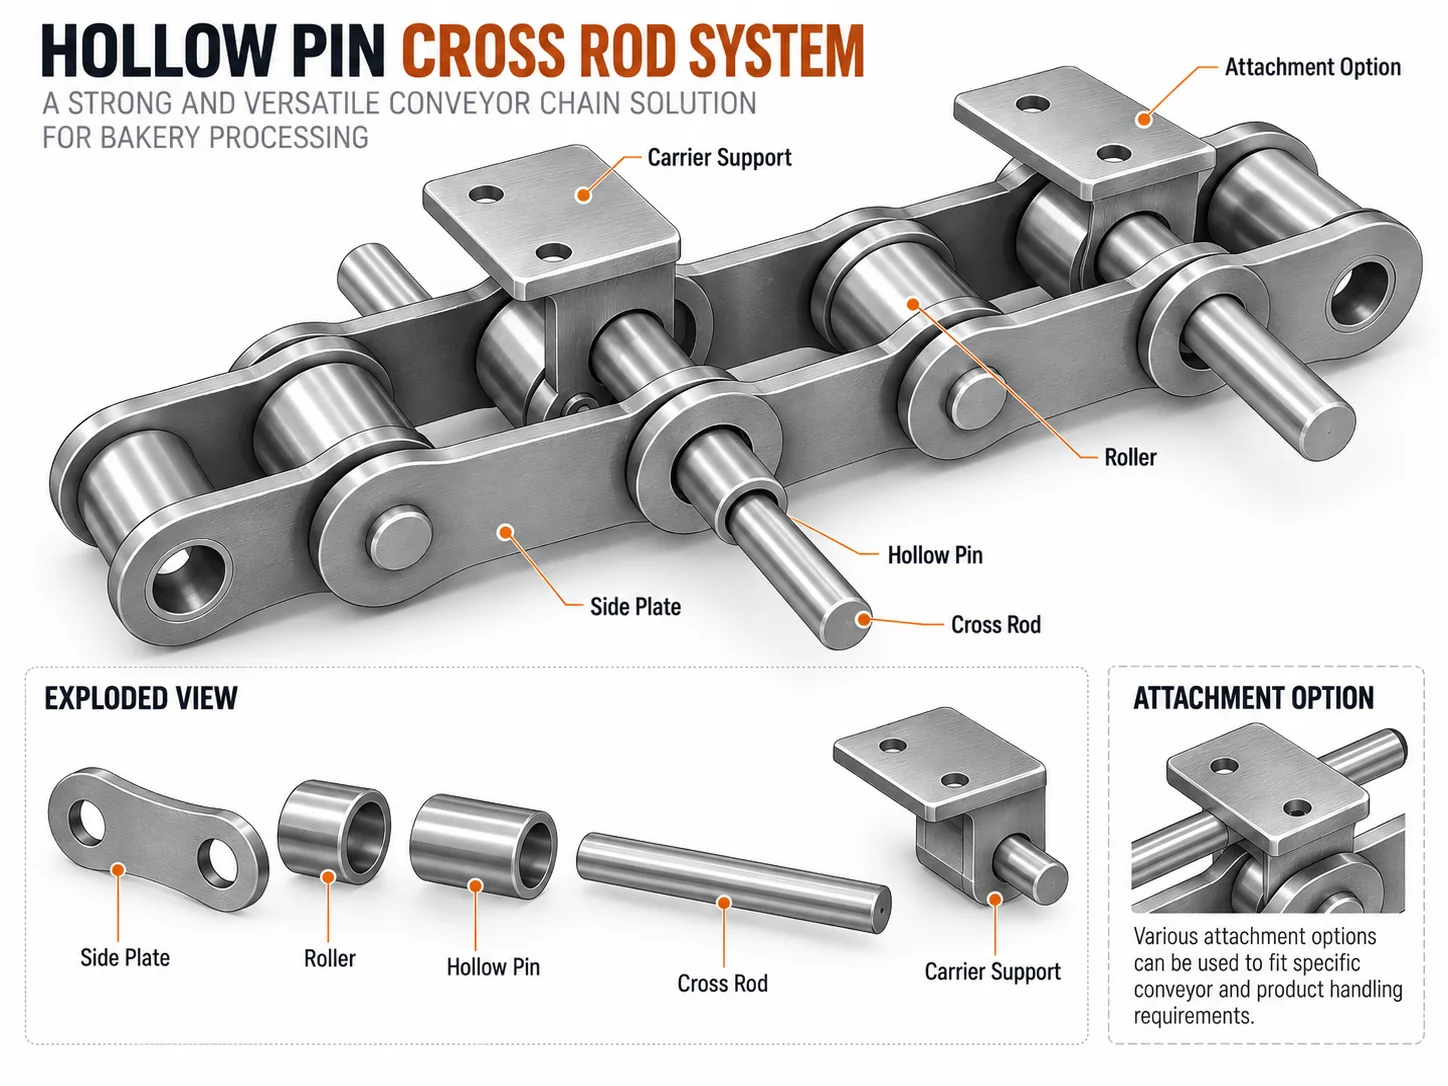
The main reason to keep this process structured is that using hollow pins as a controlled interface for cross rods and product carriers interacts with more than one component. A change that improves one symptom can shift load into another part of the mechanism. For example, correcting guide alignment may reduce side wear but also expose a take-up setting that was previously compensating for the misalignment. Record changes one at a time so the result can be interpreted.
For planned maintenance, compare the present condition with a baseline whenever one exists. If there is no baseline, create one during the next shutdown: photograph the sprockets and guide surfaces, record take-up position, measure a defined number of pitches, and note the chain’s location in proofers using cross bars, removable carriers or parallel chain strands. Repeating the same observations later is more informative than relying on general statements such as “the chain has stretched.”
ஏற்கனவே உள்ள வரைபடம் கிடைக்கும்போது, நிறுவப்பட்ட வன்பொருள் அதனுடன் இன்னும் பொருந்துகிறதா என்பதைச் சரிபார்க்கவும். பேக்கரி உபகரணங்கள் அவற்றின் சேவைக் காலத்தில் அடிக்கடி மாற்றியமைக்கப்படுகின்றன: தாங்கிகள் பழுதுபார்க்கப்படலாம், வழிகாட்டித் தண்டுகள் நகர்த்தப்படலாம், பற்சக்கரங்கள் மாற்றப்படலாம், மற்றும் இணைப்பு இடைவெளிகள் மாற்றப்படலாம். வரைபடம் பயனுள்ளதாகவே இருக்கும், ஆனால் களச் சரிபார்ப்பு ஒரு பழைய ஆவணத்தை தற்போதைய உள்ளமைப்பிற்கான ஆதாரமாகக் கருதுவதைத் தடுக்கிறது.
Procurement and engineering should use the same evidence package. The RFQ should not separate commercial quantity from technical context: hollow-pin dimensions, rod detail, strand spacing, carrier mass and cleaning routine. This makes it possible to judge whether a standard series, a modified attachment or a custom replacement is the appropriate route without creating unnecessary back-and-forth.
Finally, treat the website as a preparation tool rather than the controlling product drawing. Measurements and diagrams narrow the family and help organize the RFQ; the released drawing defines the ordered configuration. That distinction is especially important where cross-rod binding, unequal strand load or restricted articulation could have more than one mechanical cause.
Use Hollow Pin Chains in Bakery Proofers as a machine-level question, not just a chain inspection. Compare the loaded and return runs, drive and tail ends, and any transfer or carrier transition in proofers using cross bars, removable carriers or parallel chain strands. Document whether cross-rod binding, unequal strand load or restricted articulation is distributed along the strand or repeats at one location. That pattern helps separate progressive joint wear from alignment, guide, sprocket or carrier problems that a new chain alone will not correct.
The working record should include pin bore, cross-rod diameter, strand center distance, retention method and carrier width. Mark which values are fixed by the existing machine and which values can be changed to improve service. The central engineering focus is using hollow pins as a controlled interface for cross rods and product carriers. When a legacy part number conflicts with field measurements, hold the RFQ until the installed interface and the controlled drawing can be reconciled.
A useful enquiry combines commercial quantity with the technical package: hollow-pin dimensions, rod detail, strand spacing, carrier mass and cleaning routine. Also state whether the request is a direct replacement, a planned modification or a new machine design. The release objective is to treat the rod-and-pin connection as part of the load path, not just a convenient mounting hole. This reduces quote revisions and prevents a visually similar chain from being treated as interchangeable before geometry and duty have been checked.
பழைய குறிப்பு எண் கிடைத்தால் அதைப் பயன்படுத்தவும், ஆனால் நிறுவப்பட்ட வடிவம் மற்றும் பயன்பாட்டு அளவைச் சரிபார்க்கவும். இயந்திர மாற்றங்கள், முந்தைய மாற்றீடுகள் அல்லது தேய்மானம் ஆகியவை ஒரு பாக எண்ணை மட்டும் முழுமையற்றதாக ஆக்கிவிடக்கூடும்.
நடைமுறைக்கு ஏற்ற எண்ணிக்கையிலான இணைப்புகளில் பல்சுழற்சி அளவீட்டைப் பயன்படுத்தி, அந்த முறையைப் பதிவு செய்யவும். அருகருகே உள்ள ஒரே ஒரு இணைப்பின் அளவீட்டை மட்டும் சார்ந்திருப்பதற்குப் பதிலாக, அதனை இயல்பான சுருதி மற்றும் இயந்திரப் பராமரிப்பு வரம்புகளுடன் ஒப்பிடவும்.
பற்களின் தேய்மானம், சிக்கிக்கொள்ளுதல், சீரமைப்புப் பிரச்சனைகள் அல்லது சங்கிலி மீண்டும் மீண்டும் முன்கூட்டியே தேய்தல் போன்ற பிரச்சனைகள் இருக்கும்போதெல்லாம், சங்கிலியும் பற்சக்கரமும் ஒரு பிணைப்பு அமைப்பாகச் செயல்படுகின்றன.

























